

Working Principle and Features of a Dry Coffee Powder Pneumatic Conveying System
For those in the coffee processing industry, understanding the technology behind efficient dry coffee powder handling is crucial. The pneumatic conveying system, specifically designed for dry coffee powders, represents a sophisticated solution that combines functionality with reliability. This article delves into the working principle and key features of such a system, providing insights into how it operates and why it is a preferred choice for coffee manufacturers.
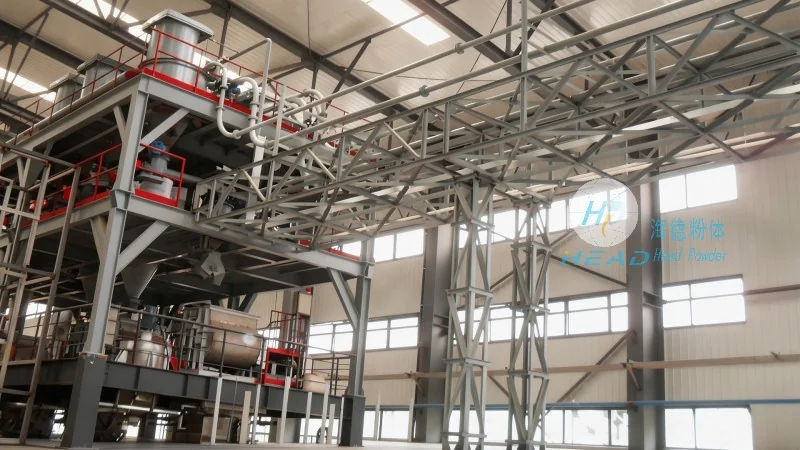
Introduction to Dry Coffee Powder Pneumatic Conveying Systems
A dry coffee powder pneumatic conveying system is a method of transporting dry, free-flowing materials like coffee powder through a pipeline using air or other gases as the conveying medium. Unlike traditional mechanical conveyors, this system eliminates the need for physical contact between the powder and the conveying equipment, which is particularly beneficial for maintaining product quality and hygiene. The system is widely adopted in coffee processing plants due to its ability to handle fine powders without causing degradation or contamination.
The Working Principle of the System
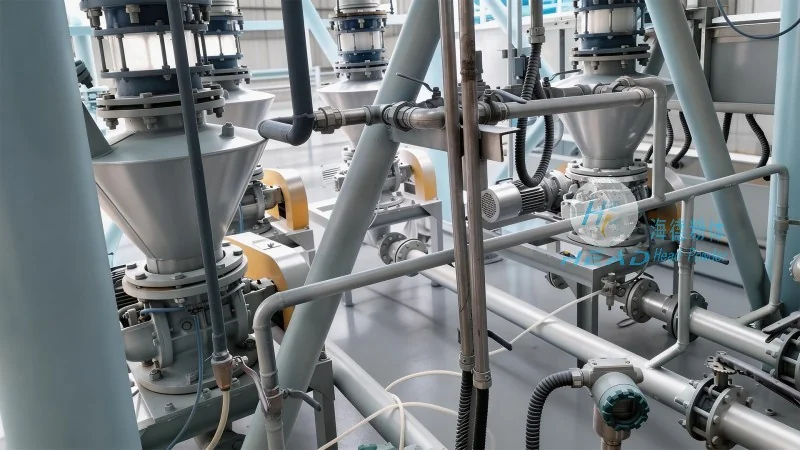
The core of a dry coffee powder pneumatic conveying system lies in its air-driven mechanism. The process begins with the coffee powder being fed into a hopper or feeder, where it is then introduced into a pipeline. Simultaneously, a fan or blower generates a high-pressure air stream that propels the powder particles through the pipeline. The air flow can be either positive pressure (where air pushes the powder) or negative pressure (where air pulls the powder from a receiver). For coffee powders, positive pressure systems are commonly used as they offer better control over the conveying process and can handle longer distances and multiple transfer points.
Within the pipeline, the coffee powder is suspended in the air stream, forming a dense phase or dilute phase flow. The density of the powder-air mixture determines the system's capacity and efficiency. In a dense phase system, the powder is conveyed in a more concentrated form, which reduces the risk of product degradation and is ideal for sensitive materials like coffee. The system's design, including the size of the pipeline, the speed of the air flow, and the feeding mechanism, all contribute to the smooth and efficient transport of the coffee powder from the source to the destination.
Key Features and Advantages
Several key features make the dry coffee powder pneumatic conveying system an attractive option for coffee manufacturers. Firstly, it offers a clean and hygienic conveying method, as there are no mechanical parts in direct contact with the product, minimizing the risk of contamination. This is critical in the food industry, where product safety and quality are paramount. Secondly, the system is highly efficient in terms of energy consumption and operational costs. By using air as the conveying medium, it reduces the need for additional equipment like conveyor belts or buckets, which can be costly to maintain and replace.
Another significant advantage is the system's ability to handle multiple transfer points and long distances without significant loss of material or quality. This flexibility allows manufacturers to design production lines that are optimized for their specific needs, whether it's moving coffee powder from a storage silo to a roasting machine or from a processing unit to a packaging line. The system also provides better control over the flow rate and pressure, ensuring consistent and reliable operation.
Furthermore, the dry coffee powder pneumatic conveying system is designed to be compact and space-efficient. Unlike large mechanical conveyors that require extensive floor space, this system can be installed in a more compact footprint, making it suitable for facilities with limited space. This is particularly beneficial for coffee processing plants that need to maximize their production area while maintaining high efficiency.
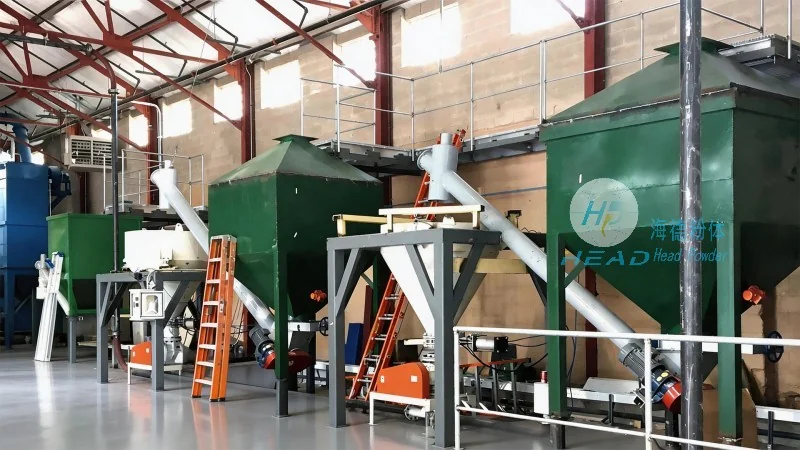
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
As a leading provider of engineering solutions for the powder handling industry, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality pneumatic conveying systems tailored to the needs of coffee manufacturers. With years of experience in the field, the company has developed a deep understanding of the unique challenges faced by the coffee industry, such as maintaining product quality, ensuring hygiene, and optimizing operational efficiency.
HeadPowder's team of engineers and technicians work closely with clients to understand their specific requirements and design customized solutions that meet their needs. The company's commitment to quality is evident in its use of advanced materials and rigorous testing procedures to ensure that each system meets the highest standards of performance and reliability. Whether it's a new installation or an upgrade to an existing system, HeadPowder provides comprehensive support, from design and manufacturing to installation and maintenance.
Address and Location
Shandong HeadPowder Engineering Co., Ltd. is located in Shandong, China, where the company has established a strong presence in the powder handling industry. The company's facilities are equipped with state-of-the-art technology and equipment, enabling it to produce high-quality pneumatic conveying systems that are used by clients worldwide. The company's location in China provides a strategic advantage, allowing it to leverage the region's manufacturing capabilities and supply chain infrastructure to deliver products efficiently and cost-effectively.