

Working Principle and Features of Aggregate Powder Pneumatic Conveying Systems
Aggregate powder pneumatic conveying systems are essential in industrial processes for efficiently transporting bulk materials such as aggregates, powders, and granules. These systems utilize air pressure or vacuum to move materials through a pipeline, offering a flexible and efficient alternative to traditional mechanical conveying methods. Understanding the working principle and key features of such systems is crucial for selecting the right equipment for specific applications.
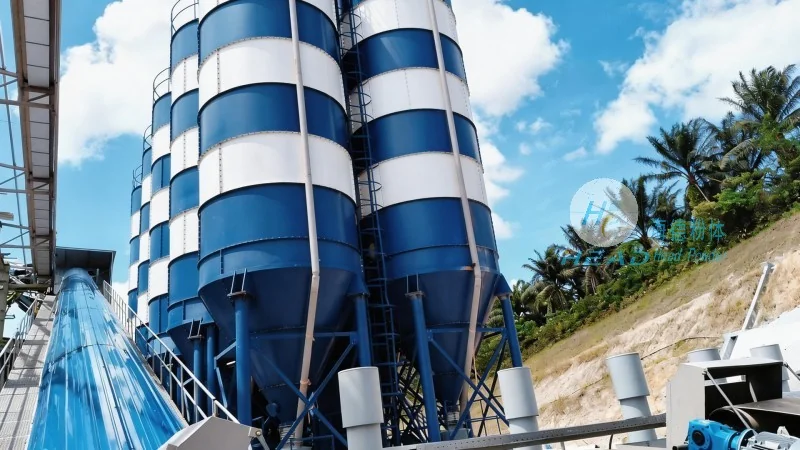
Working Principle of Aggregate Powder Pneumatic Conveying Systems
The core mechanism of aggregate powder pneumatic conveying systems involves the use of air as the medium to transport material. The process typically starts with the material being fed into a hopper or feeder. From there, the material is introduced into a pipeline where it is carried by a stream of air. The air flow can be generated through positive pressure (blowing air into the system) or negative pressure (sucking air out of the system). The choice between positive and negative pressure depends on factors like material properties, system layout, and operational requirements. In positive pressure systems, a blower or compressor provides the necessary air pressure to push the material through the pipeline. In negative pressure systems, a vacuum pump creates a vacuum that pulls the material along. The air velocity and pressure are carefully controlled to ensure stable and efficient transport without causing material degradation or blockages.
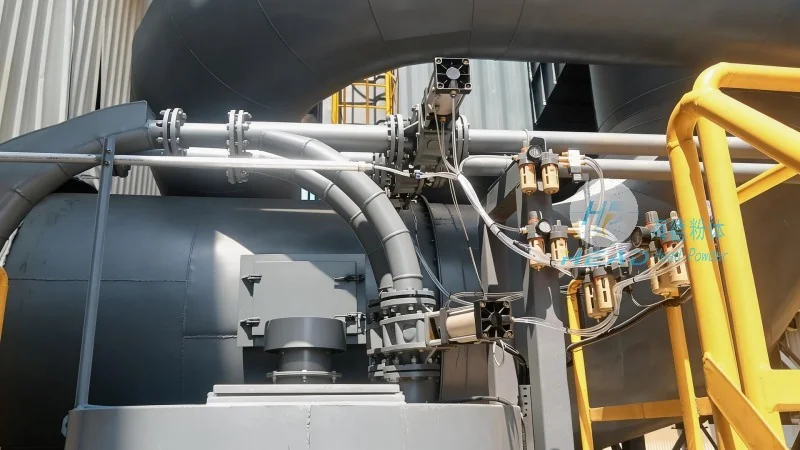
Key Features of Aggregate Powder Pneumatic Conveying Systems
Aggregate powder pneumatic conveying systems offer several advantages that make them suitable for diverse industrial applications. One of the primary features is their ability to handle a wide range of materials, including fine powders, coarse aggregates, and granular substances. This versatility allows for the transportation of materials with varying particle sizes and densities. Another significant feature is the system's flexibility in terms of layout and installation. Pneumatic conveying lines can be designed to follow complex routes, including vertical and horizontal segments, making them adaptable to different factory layouts and space constraints. Additionally, these systems are known for their low maintenance requirements compared to mechanical conveying equipment, as they have fewer moving parts and are less prone to wear and tear. The enclosed pipeline design also helps in maintaining material integrity and preventing contamination, which is critical for materials used in food, pharmaceutical, or high-purity applications. Furthermore, pneumatic conveying systems can operate at high speeds, reducing overall transport time and increasing production efficiency. However, it is important to note that the efficiency of the system depends on proper design, including the selection of appropriate air velocities, pipeline diameters, and pressure levels to avoid issues like material segregation or pipeline blockages.
Applications and Benefits in Industrial Settings
Aggregate powder pneumatic conveying systems are widely used in various industries, including construction, mining, food processing, and pharmaceuticals. In the construction industry, they are commonly employed to transport sand, gravel, and cement from storage silos to mixing plants or construction sites. The ability to handle large volumes of aggregates efficiently supports the high demand for building materials in construction projects. In the mining sector, these systems are used to transport ore and mineral powders from processing facilities to storage or further processing units. The robust design of pneumatic conveying systems makes them suitable for handling abrasive and heavy materials, which are typical in mining operations. The food and pharmaceutical industries benefit from the hygienic design of these systems, as they can be constructed with materials that meet food-grade and pharmaceutical standards, ensuring that the transported materials remain clean and free from contamination. The benefits of using pneumatic conveying systems in these industries include improved product quality, reduced labor costs, and enhanced safety by minimizing manual handling of bulk materials.
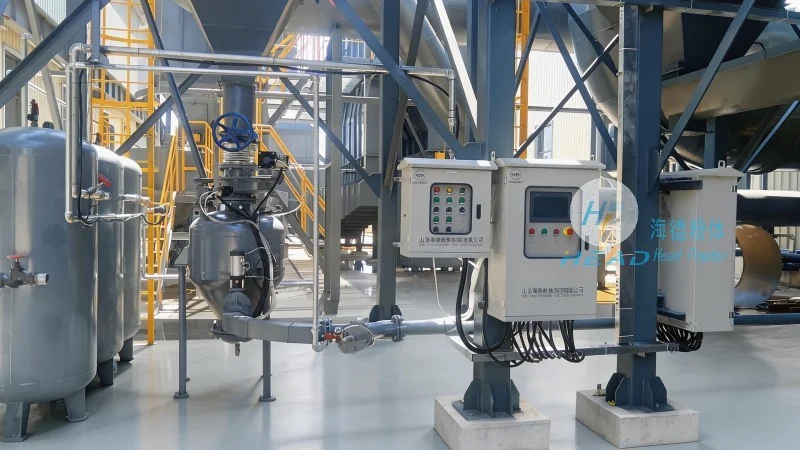
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a leading manufacturer and supplier of aggregate powder pneumatic conveying systems. With a focus on innovation and quality, the company has established itself as a trusted partner in the industry, providing customized solutions tailored to the specific needs of clients. HeadPowder's expertise lies in designing and manufacturing efficient, reliable, and durable pneumatic conveying systems that meet the highest standards of performance and safety. The company's commitment to customer satisfaction is reflected in its comprehensive after-sales support, including installation, maintenance, and technical assistance. HeadPowder's facilities are located in Shandong, China, where the company leverages advanced manufacturing technologies and a skilled workforce to produce high-quality equipment. By combining technical expertise with customer-centric approaches, HeadPowder continues to deliver solutions that enhance operational efficiency and productivity for its clients worldwide.