

Working Principle and Features of a Powdered Material Mixing Pneumatic Conveying Machine
At Shandong HeadPowder Engineering Co., Ltd., we specialize in the design and manufacturing of advanced equipment for the powder handling industry. Our flagship product, the powdered material mixing pneumatic conveying machine, is engineered to meet the demanding needs of various industrial applications. This article delves into the working principle and key features of this essential piece of equipment, providing a comprehensive overview for professionals in the field.

Understanding the Working Principle
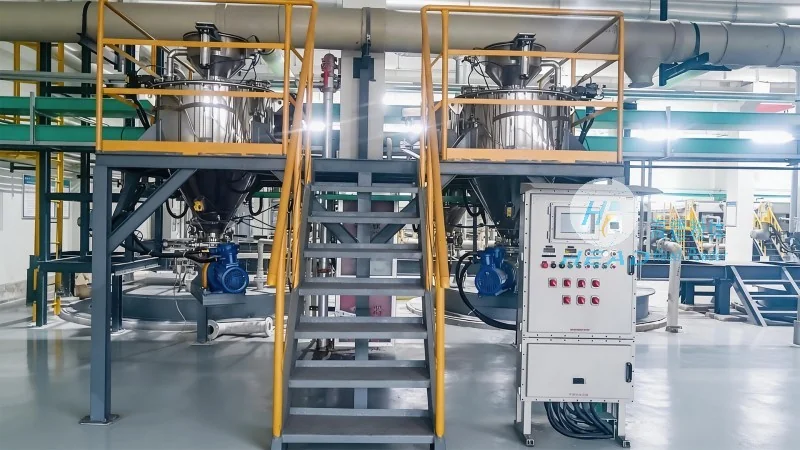
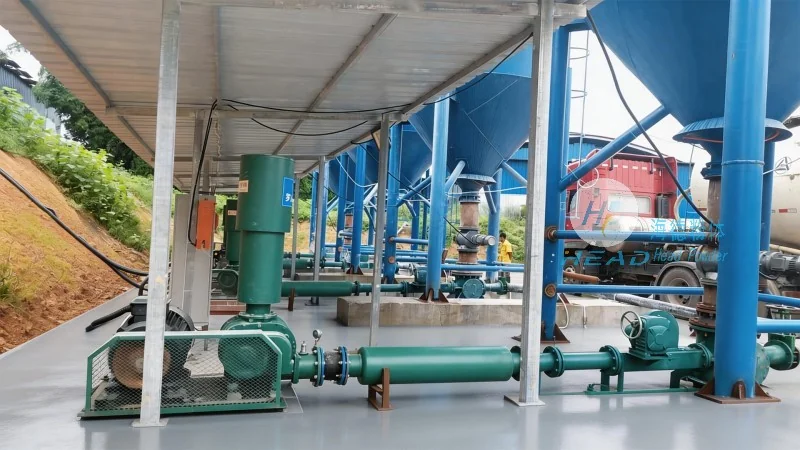
The powdered material mixing pneumatic conveying machine operates on the principle of pneumatic transport, utilizing air as the medium to move bulk powders from one location to another. The system typically consists of a hopper for material storage, a mixing chamber where different powders are combined, and a conveying pipeline that transports the mixed material to the discharge point. The process begins with the material being fed into the hopper, where it is then drawn into the mixing chamber by the action of a fan or blower. Inside the mixing chamber, the powders are thoroughly blended to achieve the desired composition. The mixed material is then propelled through the conveying pipeline by the force of the air stream, which is generated by the fan. The conveying speed and pressure are carefully controlled to ensure efficient and consistent transport without causing degradation or segregation of the powder particles.
Key Features and Advantages
Our powdered material mixing pneumatic conveying machine offers several distinct advantages that make it a preferred choice for industrial applications. Firstly, it provides a dust-free and hygienic method of material handling, which is crucial in industries such as food, pharmaceuticals, and chemicals where contamination control is paramount. The enclosed system prevents the release of powders into the environment, ensuring compliance with environmental regulations and maintaining a safe working environment. Secondly, the machine offers high efficiency in terms of material transfer, with minimal loss and maximum throughput. The mixing capability allows for the precise combination of multiple powders, enabling the production of customized formulations. Additionally, the pneumatic conveying system is flexible and can be easily integrated into existing production lines, reducing the need for extensive modifications. The machine is also designed for durability and low maintenance, with robust components that can withstand the rigors of continuous operation. This results in lower operational costs and increased productivity over the long term.
Technical Specifications and Applications
The powdered material mixing pneumatic conveying machine from Shandong HeadPowder Engineering Co., Ltd. is available in various models to suit different production requirements. The equipment is equipped with advanced control systems that allow for precise adjustment of conveying parameters, ensuring optimal performance. The machine can handle a wide range of powder types, including fine powders, granules, and bulk materials, with particle sizes ranging from sub-micron to several millimeters. Typical applications include the mixing and conveying of raw materials in the food processing industry, the blending of active ingredients in pharmaceutical manufacturing, and the transport of chemical powders in the chemical industry. The machine's versatility makes it suitable for a variety of processes, from small-scale laboratory applications to large-scale industrial production.
Conclusion
In conclusion, the powdered material mixing pneumatic conveying machine is a highly effective solution for the efficient and hygienic handling of powdered materials. Its working principle, based on pneumatic transport and mixing, combined with its key features such as dust-free operation, high efficiency, and flexibility, makes it an indispensable tool in modern industrial settings. Shandong HeadPowder Engineering Co., Ltd. is committed to providing high-quality equipment that meets the evolving needs of the industry, ensuring reliable performance and customer satisfaction. Whether you are in the food, pharmaceutical, or chemical sector, our pneumatic conveying machine offers a reliable and efficient solution for your material handling requirements.