

Working Principle and Features of Stone Material Pneumatic Conveying Systems
For industries dealing with stone materials, efficient material handling is crucial. Pneumatic conveying systems offer a reliable solution to transport bulk materials like gravel, crushed stone, and other aggregates. This article explores the working principles and key features of such systems, highlighting how they enhance operational efficiency and safety in material processing.
Working Principle of Pneumatic Conveying Systems
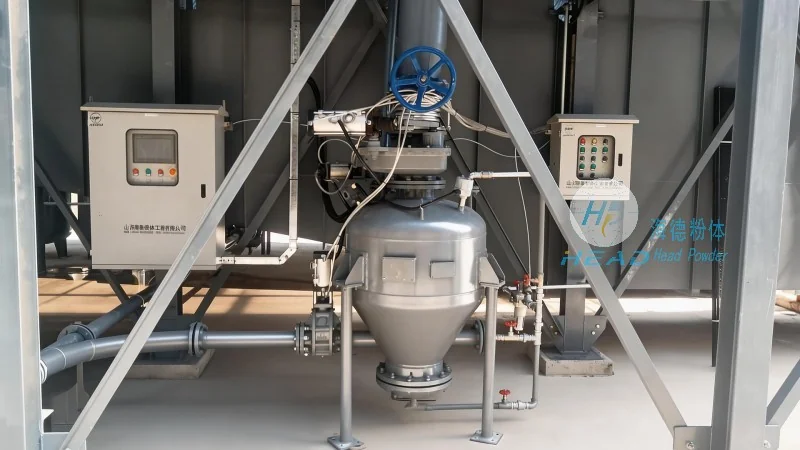
The core of a pneumatic conveying system is the use of air to transport solid materials. The process typically involves a series of components that work in tandem to move material from a source to a destination. At its essence, the system operates by creating a pressure differential that propels the material through a pipeline. There are two main types of pneumatic conveying: pressure and vacuum systems. Pressure systems use compressed air to push material, while vacuum systems use a vacuum to pull material. Both methods rely on the principle of air flow to transport particles, ensuring that even abrasive stone materials are handled smoothly without damage to the equipment.
Key Features and Advantages of Stone Material Pneumatic Conveying Systems
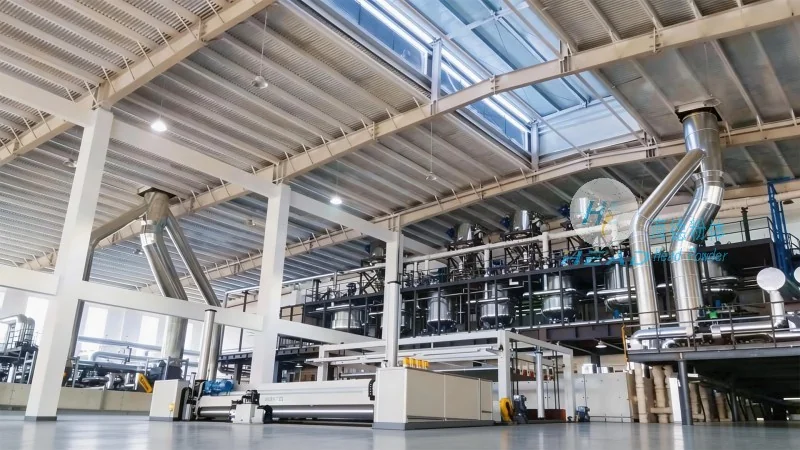
When selecting a pneumatic conveying system for stone materials, several features stand out as critical. First, the system’s ability to handle abrasive materials without excessive wear is a significant advantage. The design of the pipeline and components, such as high-quality steel or specialized coatings, minimizes wear from crushed stone or gravel. Second, the system offers flexibility in layout, allowing for vertical, horizontal, or mixed-direction transport. This adaptability is essential for facilities with complex layouts or limited space. Third, pneumatic conveying systems provide a dust-free operation, which is vital for maintaining a safe and clean working environment. Unlike traditional belt or bucket elevators, these systems keep the material enclosed, reducing dust emissions and improving air quality. Additionally, the systems are energy-efficient, with modern designs optimizing air usage to reduce operational costs. The ability to transport materials at high speeds also contributes to increased productivity, as the system can move large volumes of stone material quickly and reliably.
Application and Performance in Real-World Scenarios
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and manufacturing pneumatic conveying systems tailored to the needs of stone processing industries. The company’s expertise lies in understanding the unique challenges of handling abrasive stone materials, such as gravel and crushed rock. By leveraging advanced engineering and high-quality materials, HeadPowder ensures that their systems deliver long-lasting performance and minimal maintenance. For example, a client in the construction aggregate industry reported a 30% reduction in material handling time after implementing a HeadPowder pneumatic conveying system. The system’s ability to handle high volumes of stone material while maintaining low operational costs made it a preferred choice. Furthermore, the company’s commitment to customizing solutions means that each system is designed to meet specific operational requirements, ensuring optimal performance in diverse applications.
Conclusion
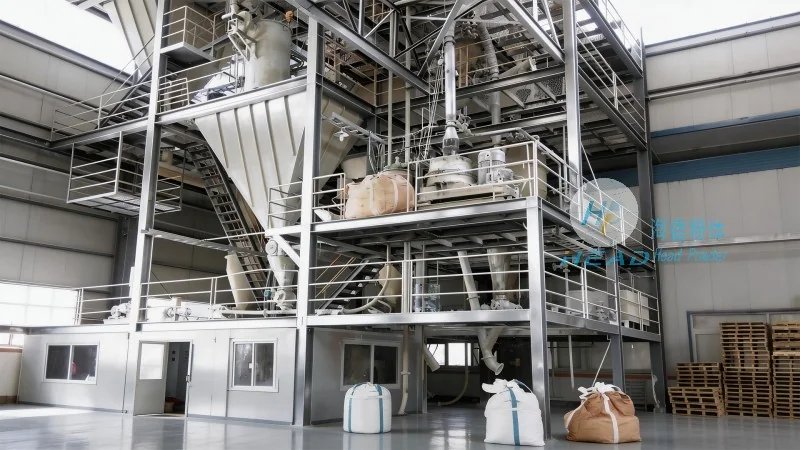
Pneumatic conveying systems for stone materials are a robust and efficient solution for material handling in various industries. By understanding the working principles and key features, businesses can make informed decisions about implementing such systems. The advantages, including durability, flexibility, and dust-free operation, make these systems a valuable investment. Shandong HeadPowder Engineering Co., Ltd. stands as a trusted partner in providing high-quality pneumatic conveying systems that meet the demands of modern stone processing operations. With their expertise and commitment to quality, HeadPowder continues to deliver reliable solutions that enhance productivity and safety in material handling.