

Working Principle and Features of Cocoa Powder Material Pneumatic Conveying Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing advanced pneumatic conveying solutions tailored for handling cocoa powder and similar fine materials. This article delves into the operational mechanics and key attributes of their equipment, offering insights into how these systems efficiently transport cocoa powder while maintaining product integrity.
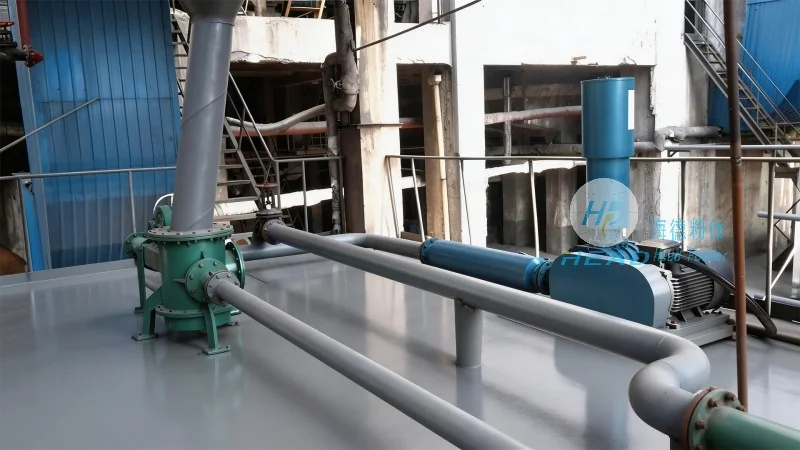
Understanding the Pneumatic Conveying Process
The core of HeadPowder's cocoa powder pneumatic conveying equipment lies in the air-based transport mechanism. The system typically operates by creating a pressure differential or using vacuum to draw cocoa powder from a storage silo or hopper into a conveying line. A blower or compressor generates the necessary airflow, which propels the powder through pipelines to the destination, such as a processing unit or packaging area. This method eliminates the need for mechanical components like belts or buckets, reducing friction and minimizing product contamination.
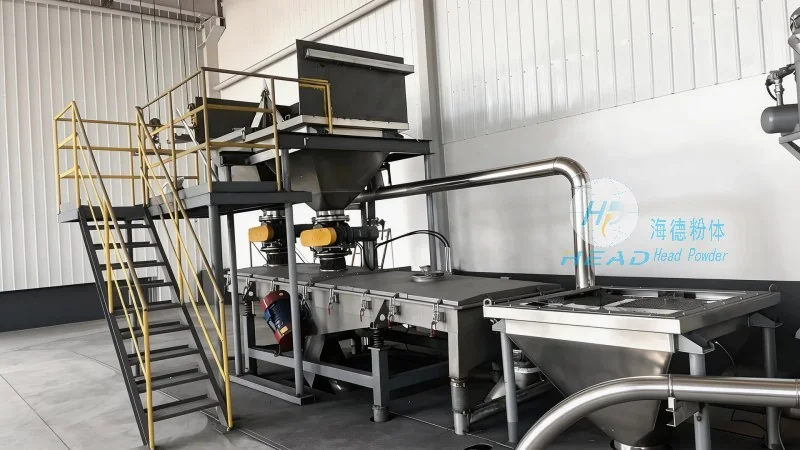
Key Features of the Equipment
HeadPowder's cocoa powder pneumatic conveying systems are designed with several distinct features that enhance performance and reliability. Firstly, the equipment incorporates advanced filtration and separation technology to prevent dust accumulation and ensure clean air circulation. This is crucial for maintaining the quality of cocoa powder, which is sensitive to moisture and contaminants. Secondly, the system features adjustable airflow controls, allowing operators to optimize the conveying rate based on material characteristics and pipeline length. This flexibility ensures efficient transport without excessive energy consumption.
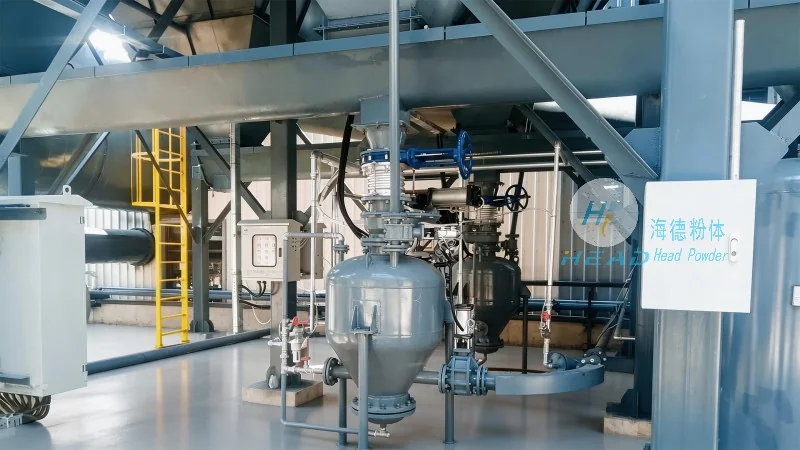
Advantages in Material Handling
When handling cocoa powder, traditional methods like belt conveyors may cause product degradation due to friction and exposure to air. In contrast, pneumatic conveying offers several advantages. The enclosed system protects cocoa powder from environmental factors, preserving its flavor and aroma. Additionally, the equipment is highly scalable, making it suitable for both small-scale production lines and large industrial facilities. HeadPowder's solutions are engineered to handle varying particle sizes and moisture content, ensuring consistent performance across different applications.
Operational Efficiency and Maintenance
HeadPowder's cocoa powder pneumatic conveying equipment is built for long-term operational efficiency. The design minimizes downtime through robust components and easy maintenance access points. Regular cleaning and filter replacement are the primary maintenance tasks, which can be performed quickly without disrupting production. The system's energy-efficient operation also contributes to lower operational costs, making it a cost-effective choice for businesses handling cocoa powder on a regular basis.
Conclusion
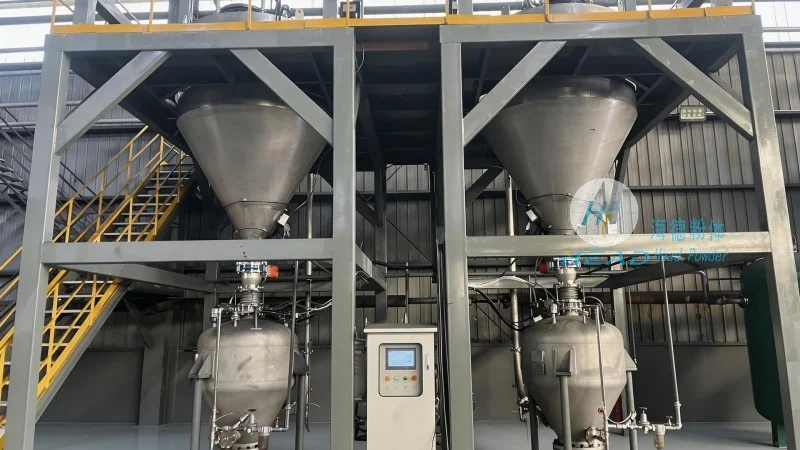
HeadPowder's cocoa powder material pneumatic conveying equipment combines advanced technology with practical design to deliver reliable and efficient transport solutions. By leveraging air-based transport and incorporating features like filtration and adjustable controls, the system ensures the quality of cocoa powder while optimizing operational performance. As a trusted manufacturer based in Shandong, China, HeadPowder continues to provide high-quality equipment tailored to the needs of the cocoa processing industry.