

Principles and Operational Characteristics of Purified Ash Pneumatic Conveying Systems
Industrial material handling systems, particularly those used for transporting purified ash, rely on sophisticated pneumatic conveying technologies to ensure efficient and reliable operation. These systems have become integral to industries such as power generation, cement production, and waste management, where the safe and effective movement of ash is critical to overall process efficiency. This article explores the underlying principles of purified ash pneumatic conveying lines and highlights the key operational characteristics that define their performance in real-world applications.
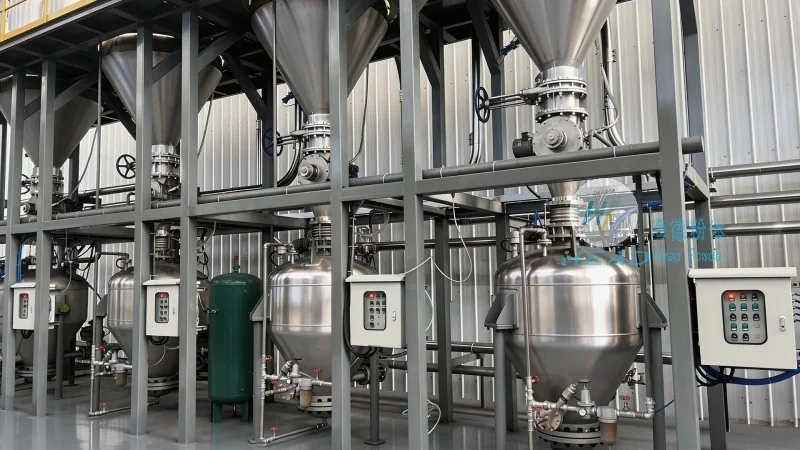
Principles of Pneumatic Conveying for Purified Ash
Pneumatic conveying systems for purified ash operate on the fundamental principle of utilizing air as a transport medium to move particulate materials through a pipeline. The process begins with a blower or fan that generates a flow of air, which then lifts and transports the ash particles from the source point to the destination. This method is based on the concept of differential pressure, where the pressure difference between the inlet and outlet of the system creates the necessary force to move the material. The design of the conveying line, including factors like pipe diameter, air velocity, and the type of air flow (positive or negative pressure), is critical in determining the system's capacity and efficiency. Positive pressure systems, where air is forced into the pipeline, are commonly used for long-distance or high-volume transport, while negative pressure systems, which draw air out of the pipeline, are suitable for shorter distances or applications where dust control is a priority.
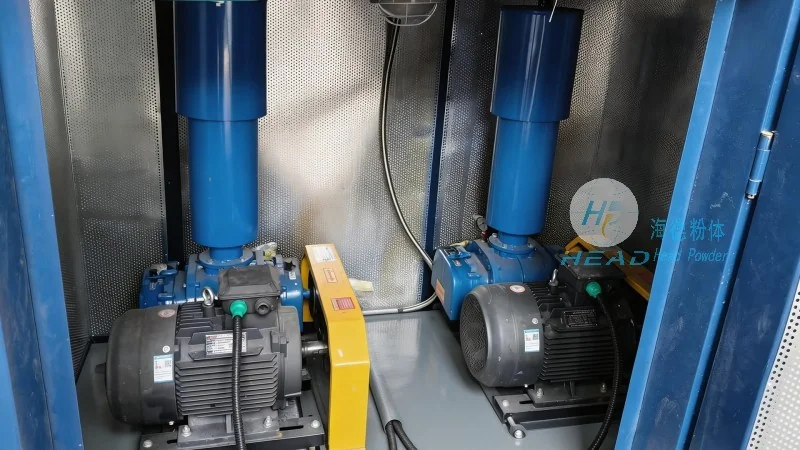
Key Working Scene Characteristics
The operational characteristics of purified ash pneumatic conveying systems are tailored to specific industrial environments, such as thermal power plants, cement factories, and waste treatment facilities. These systems are engineered to handle high volumes of ash with minimal maintenance, ensuring continuous operation even under demanding conditions. The flexibility of the system allows for seamless integration with existing infrastructure, reducing the need for extensive site modifications and minimizing downtime during installation. Additionally, the ability to control the flow rate and pressure enables precise delivery of ash to processing units, such as storage silos or treatment facilities, ensuring that the material is handled in a controlled and efficient manner. The systems are also designed for durability, with components like wear-resistant liners, robust blower systems, and high-quality piping that can withstand the abrasive nature of ash particles over extended periods. This durability is further enhanced by regular maintenance protocols and the use of advanced materials that resist corrosion and wear, ensuring long-term reliability.
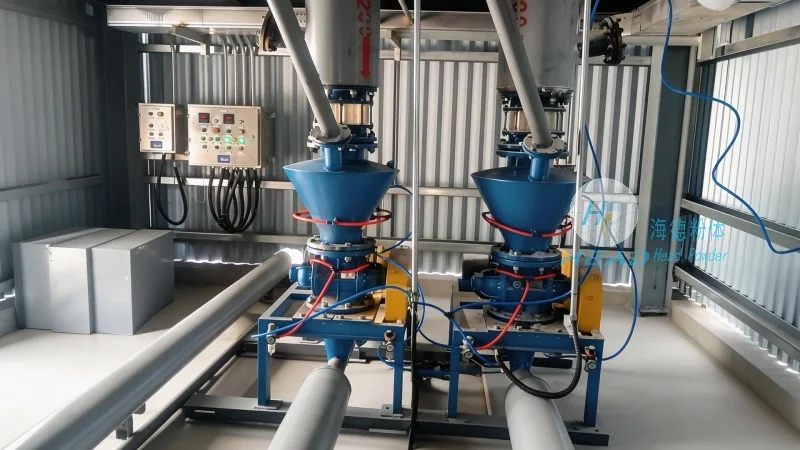
Company Overview and Expertise
HeadPowder, a leading provider of engineering solutions for material handling, specializes in the design and implementation of advanced pneumatic conveying systems for purified ash applications. With a focus on delivering customized solutions that meet the unique needs of each client, HeadPowder leverages decades of industry experience to develop innovative and efficient systems. The company's team of engineers works closely with clients to assess operational requirements, site conditions, and material characteristics, ensuring that the final system is optimized for performance and longevity. HeadPowder adheres to international standards and rigorous testing protocols, which guarantee the reliability and safety of its products. The company's commitment to quality is reflected in its ability to provide comprehensive support, including installation, training, and after-sales service, to ensure that clients can maximize the benefits of their pneumatic conveying systems.
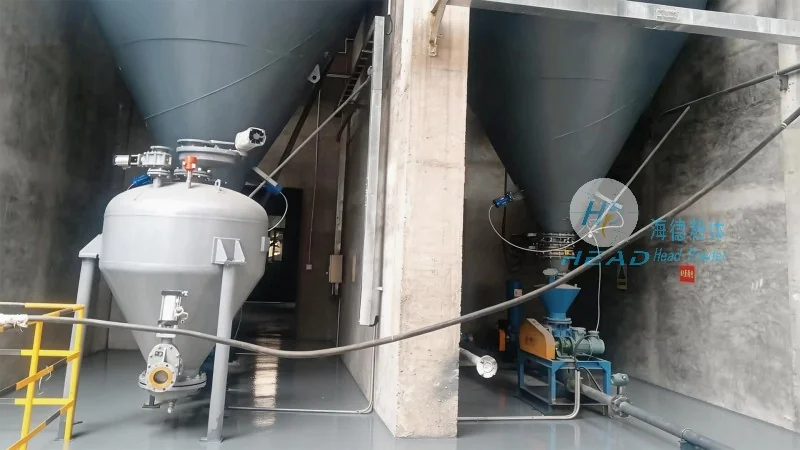
Address and Location
HeadPowder Engineering Co., Ltd. is headquartered in Shandong, China, where the company maintains its research and development facilities and manufacturing operations. The location in Shandong provides easy access to key industrial markets and supply chains, enabling efficient production and delivery of pneumatic conveying systems. The company's presence in this region underscores its dedication to serving the growing demand for advanced material handling solutions in the Asia-Pacific market. HeadPowder's facilities are equipped with state-of-the-art technology and skilled personnel, allowing the company to meet the diverse needs of its global clientele while maintaining high standards of quality and service.