

Principle and Working Scene Characteristics of Coal Ash Powder Conveying Equipment
Coal ash, a byproduct of coal combustion in thermal power plants, presents significant challenges in handling and transportation due to its fine powder nature and potential environmental hazards. Efficient and reliable powder conveying equipment is essential for managing coal ash from generation to disposal or utilization. This article explores the working principle of coal ash powder conveying equipment and highlights its key characteristics in various working scenarios, with a focus on the solutions provided by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field.
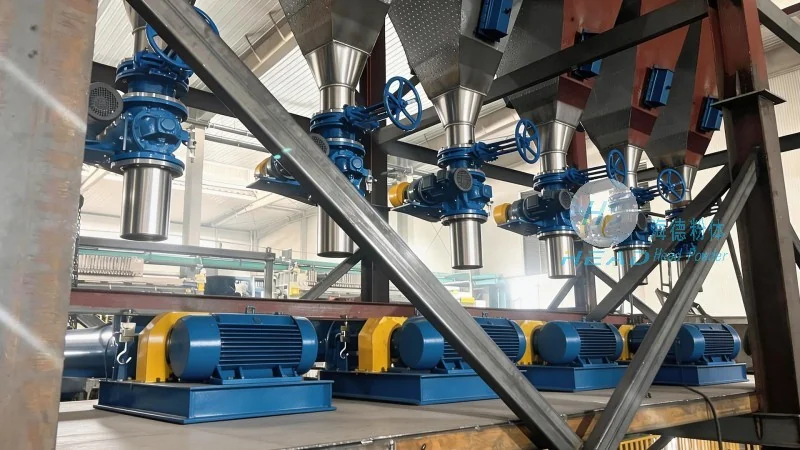
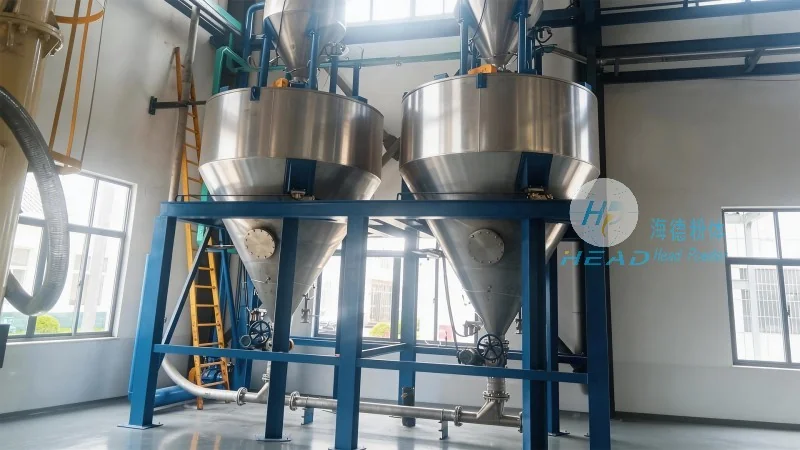
Working Principle of the Equipment
The core of coal ash powder conveying equipment lies in its ability to transport fine powders like coal ash through a closed system, minimizing dust emission and ensuring stable flow. Typically, these systems utilize positive pressure or negative pressure methods to move the material. Positive pressure systems, such as pneumatic conveyors, use compressed air to push the powder through pipes, while negative pressure systems employ vacuum to draw the material. The equipment often includes components like feeders, conveying pipes, airlocks, and dust collectors. The feeders ensure a consistent material flow, the conveying pipes transport the ash, and airlocks prevent backflow and maintain system pressure. Dust collectors are crucial for capturing fine particles and ensuring compliance with environmental regulations. The working principle is designed to handle the abrasive and potentially hazardous nature of coal ash, ensuring safe and efficient operation.
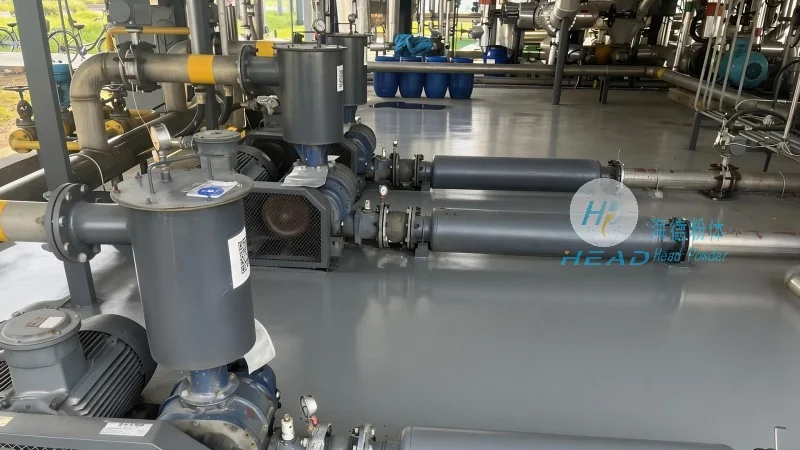
Key Working Scene Characteristics
Coal ash powder conveying equipment is deployed in diverse industrial settings, each with unique requirements that influence the equipment's design and performance. In thermal power plants, the equipment is used to transport ash from the boiler to storage silos or disposal sites, often over long distances. The working scene in this context demands high capacity and durability to handle large volumes of ash. In construction material production facilities, coal ash is used as a raw material for cement and concrete, requiring precise dosing and conveying to maintain product quality. The equipment must ensure accurate material delivery to mixing plants, which is critical for consistent product performance. Additionally, in environmental remediation projects, the equipment is used to transport ash for reuse or disposal, where environmental safety is paramount. The working scene characteristics include varying material flow rates, different pipe lengths and layouts, and the need for integration with existing industrial processes. The equipment's flexibility and adaptability are key to meeting these diverse requirements.
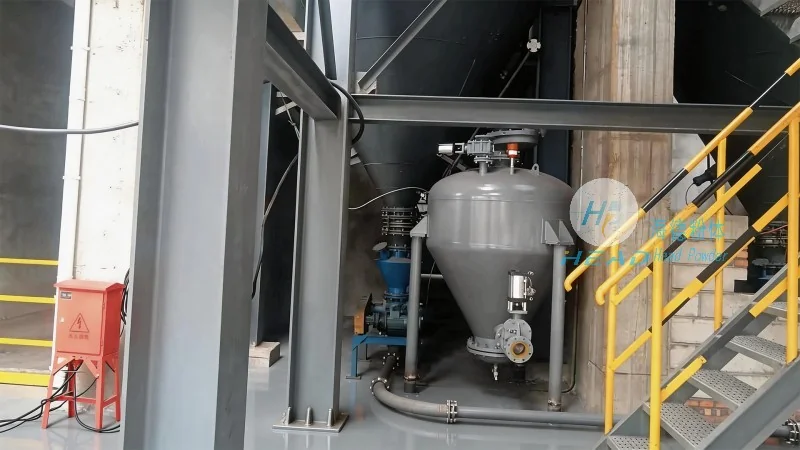
Company Profile and Technical Support
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in the design, manufacturing, and supply of advanced powder conveying equipment tailored for coal ash and other fine materials. The company leverages decades of industry experience to develop solutions that address the specific challenges of coal ash handling, such as dust control, material abrasion, and system reliability. HeadPowder's products are engineered with high-quality materials and advanced control systems to ensure long-term performance and minimal maintenance. The company provides comprehensive technical support, including system design consultation, installation guidance, and after-sales service, to help clients optimize their coal ash handling processes. With a strong commitment to innovation and customer satisfaction, HeadPowder has established itself as a trusted partner in the power and construction industries, delivering reliable and efficient solutions for coal ash powder conveying needs.