

Principle and Application Scenarios of Dry Powder Bulk Material Conveying Systems
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced dry powder bulk material conveying systems. These systems are critical in various industrial sectors, enabling efficient and reliable transportation of dry powders from one location to another. Understanding the underlying principles and diverse application scenarios of such systems is essential for optimizing operational efficiency and ensuring product integrity.
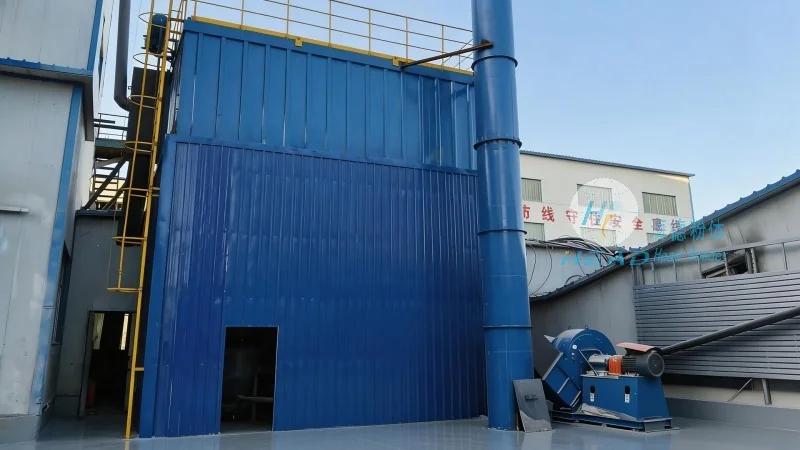
Core Principles of Dry Powder Conveying Systems
Dry powder bulk material conveying lines operate on several fundamental principles, each tailored to specific material characteristics and operational requirements. The primary mechanisms include gravitational, pneumatic, and mechanical methods. Gravitational systems rely on the natural weight of the material to move it through inclined chutes or hoppers, making them suitable for low-density, free-flowing powders. Pneumatic systems, on the other hand, utilize compressed air to transport powders in a sealed pipeline, offering flexibility for both horizontal and vertical movement. Mechanical systems, such as screw conveyors and belt conveyors, employ rotating components to push or pull the material along a fixed path, providing consistent control over flow rates and pressure.
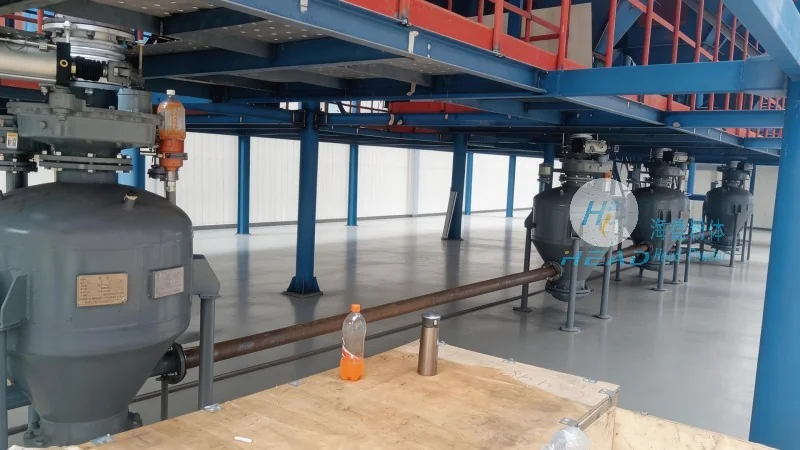
Key Working Scenarios and Industry Applications
The versatility of dry powder conveying systems is evident across multiple industries, each presenting unique challenges and requirements. In the chemical industry, these systems are crucial for transporting raw materials like calcium carbonate and silica to production lines, where precise dosing and minimal contamination are paramount. The food and beverage sector utilizes them to handle ingredients such as flour, sugar, and spices, ensuring hygienic and efficient processing. Pharmaceutical applications demand stringent controls to prevent cross-contamination and maintain product purity, making advanced conveying solutions essential for manufacturing active pharmaceutical ingredients (APIs) and finished dosage forms. Additionally, in the agricultural sector, dry powder conveyors facilitate the handling of fertilizers and pesticides, supporting large-scale farming operations.
Design Considerations and Material Compatibility
Effective design of dry powder conveying systems requires careful consideration of material properties, including particle size, density, and flowability. For cohesive or sticky powders, anti-adhesion coatings and aggressive screw designs are employed to prevent blockages and ensure smooth operation. In contrast, free-flowing powders benefit from smooth, inclined chutes to minimize friction and maintain consistent flow. The choice of conveying method also depends on the system's layout, with pneumatic systems excelling in complex, multi-level facilities and mechanical systems offering simplicity and reliability for straightforward horizontal or vertical transport. HeadPowder's expertise lies in tailoring these solutions to meet the specific needs of each client, ensuring optimal performance and longevity.

Operational Advantages and Industry Standards
Implementing dry powder conveying systems offers numerous operational advantages, including reduced labor costs, minimized material waste, and enhanced safety. By automating the material handling process, industries can achieve higher throughput and lower downtime. Furthermore, these systems contribute to improved product quality by maintaining consistent moisture levels and preventing exposure to contaminants. Compliance with international standards, such as those from the Food and Drug Administration (FDA) and the European Union's Good Manufacturing Practices (GMP), is a critical aspect of modern conveying solutions. HeadPowder adheres to these standards, ensuring that their systems are designed, manufactured, and installed to meet the highest regulatory requirements, providing clients with peace of mind and reliable performance.