

Principle and Working Scene Characteristics of Calcium Carbonate Stone Powder Material Handling Syst
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced material handling systems. This article focuses on the calcium carbonate stone powder material handling system, detailing its operational principles and the specific characteristics of its working environments.
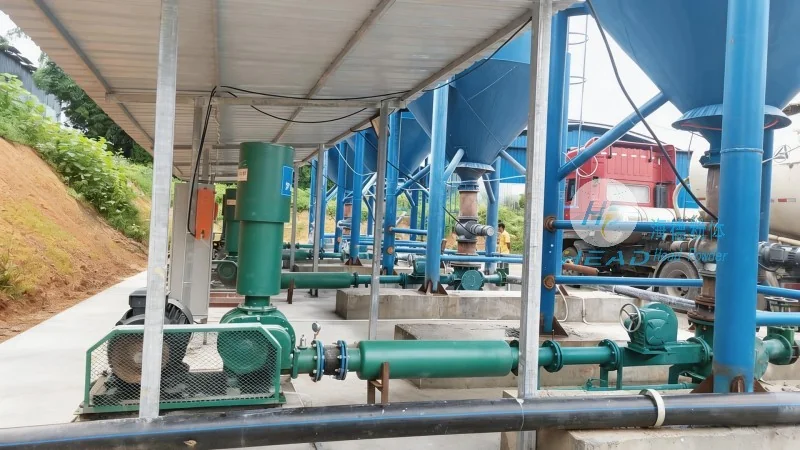
Overview of Calcium Carbonate Stone Powder Material Handling Systems
Calcium carbonate stone powder, commonly used in industries such as papermaking, plastics, and coatings, presents unique challenges during transportation due to its fine particle size and abrasive properties. Traditional methods like belt conveyors may suffer from material buildup and wear, making specialized systems essential for efficient and reliable handling. The calcium carbonate stone powder material handling system from HeadPowder addresses these challenges through a combination of advanced engineering and robust design.
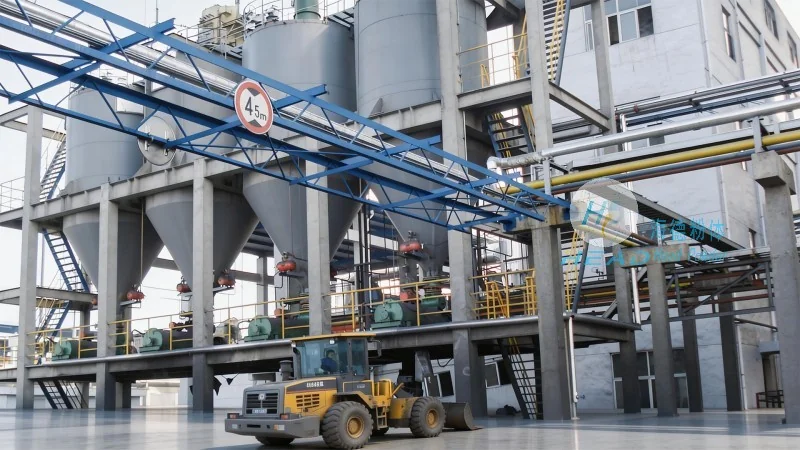
Core Principles of the Material Handling System
The system operates on the principle of controlled material flow, utilizing a network of components that work in tandem to ensure seamless transportation. Key elements include high-efficiency feeders, flexible ducting systems, and intelligent control units. The feeders are designed to handle the fine, powdery nature of calcium carbonate stone powder, preventing blockages and maintaining consistent flow rates. The ducting, often made from corrosion-resistant materials like stainless steel or specialized plastics, minimizes particle degradation and ensures long-term durability. The control unit integrates sensors and automation technology to monitor flow rates, pressure, and system performance, allowing for real-time adjustments and optimal operation.
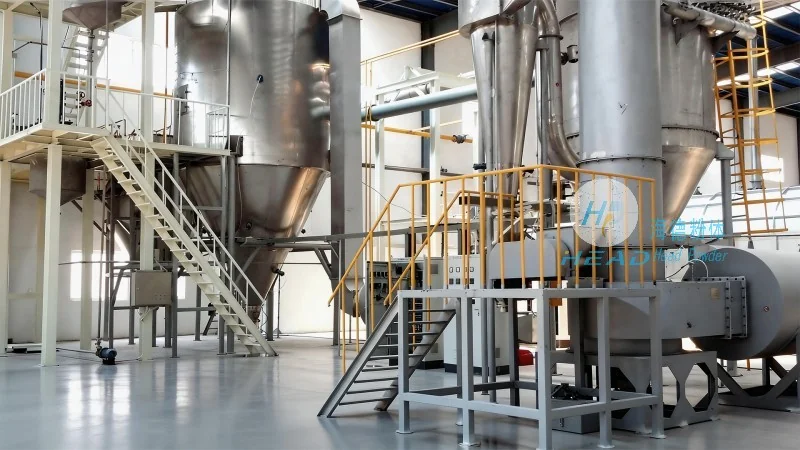
Working Scene Characteristics and Application Scenarios
The working scene characteristics of the calcium carbonate stone powder material handling system are tailored to the demands of industrial production environments. In manufacturing facilities, the system is typically integrated into production lines where the powder is required for mixing, coating, or compounding processes. The system’s ability to handle high volumes with minimal downtime is critical in such settings, as any interruption can impact production efficiency. For example, in the paper industry, the system efficiently transports calcium carbonate filler to the papermaking machines, ensuring uniform distribution and consistent product quality. In the plastic industry, the system supplies the powder to extrusion lines, where it is blended with polymers to enhance material properties. The system’s adaptability also makes it suitable for applications in the construction industry, where calcium carbonate is used as a filler in cement and concrete production.
Advantages in Diverse Operational Environments
One of the key characteristics of the HeadPowder system is its adaptability to various operational environments. Whether in a clean, controlled factory setting or a more rugged industrial plant, the system maintains high performance. The use of sealed ducting prevents dust emissions, ensuring compliance with environmental regulations and providing a safer working environment for personnel. The system’s energy efficiency is another notable feature, with optimized designs reducing power consumption while maintaining high throughput. This makes it an economical choice for long-term operation, especially in large-scale production facilities. Additionally, the modular design allows for easy integration with existing production lines and future expansion, providing flexibility as production needs evolve.

Conclusion and Company Expertise
HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, has established itself as a trusted provider of specialized material handling solutions. The calcium carbonate stone powder material handling system exemplifies the company’s commitment to innovation and reliability. By understanding the unique properties of calcium carbonate stone powder and the specific demands of industrial applications, HeadPowder has developed a system that enhances operational efficiency, reduces maintenance costs, and ensures consistent product quality. For industries relying on calcium carbonate stone powder, this system represents a superior solution for material transportation, supporting sustainable and productive manufacturing processes.