

Principle and Working Scene Characteristics of Coal Ash Material Handling System Equipment
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced material handling systems tailored for industrial applications. This article delves into the core principles of coal ash material handling systems and highlights the key working scene characteristics that define their effectiveness in modern industrial settings.
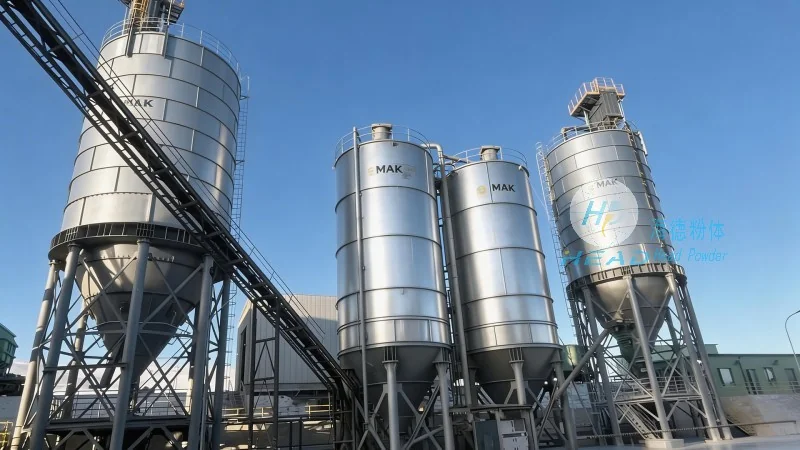
Introduction to Coal Ash Material Handling Systems
Coal ash, a byproduct of coal combustion in power plants and industrial facilities, poses unique challenges for efficient handling and disposal. Traditional methods often involve manual labor or outdated equipment, leading to inefficiencies, safety risks, and environmental concerns. To address these issues, specialized coal ash material handling systems have been developed to streamline the process, ensuring safe, reliable, and cost-effective management of this waste material.
The Core Principles of Coal Ash Material Handling Systems
At the heart of coal ash material handling systems lies a combination of mechanical, pneumatic, and hydraulic technologies designed to handle the abrasive and heavy nature of coal ash. The system typically comprises several key components, including feeders, conveyors, storage silos, and discharge mechanisms. Each component is engineered to work in harmony, ensuring the smooth and continuous transport of coal ash from its source to its final destination. The principle of gravity and mechanical force is often utilized, with conveyors such as belt conveyors, screw conveyors, or pneumatic conveyors being the most common. These systems are designed to minimize friction and wear, extending the operational life of the equipment while maintaining high throughput rates.
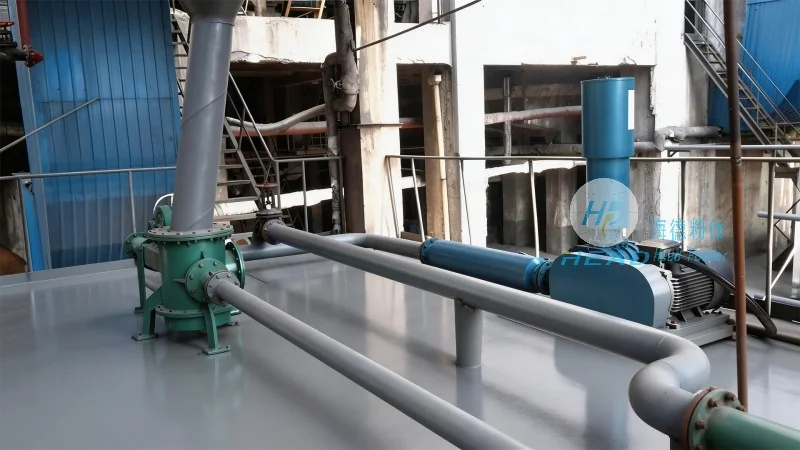
Working Scene Characteristics of Coal Ash Material Handling Systems
The effectiveness of coal ash material handling systems is heavily influenced by the specific working scenes in which they are deployed. These characteristics include the scale of the operation, the type of coal ash being handled, the environmental conditions, and the safety requirements of the facility. In large-scale power plants, for instance, the system must handle massive volumes of ash, often requiring multiple conveyors and storage silos to manage the flow. The working scene may also involve harsh environmental conditions, such as high temperatures or dust, which necessitates robust materials and protective measures to ensure equipment longevity and operator safety. Additionally, the system must integrate seamlessly with existing infrastructure, such as existing pipelines or storage facilities, to avoid disruptions in the overall plant operations.
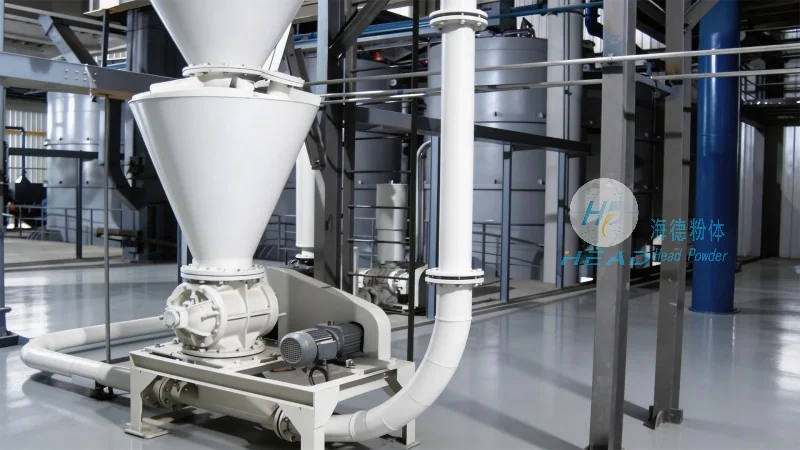
Key Advantages and Applications
Coal ash material handling systems offer several advantages that make them indispensable in industrial settings. Their ability to handle large volumes of material efficiently reduces labor costs and minimizes downtime. The systems are also designed for durability, with components made from wear-resistant materials to withstand the abrasive nature of coal ash. This results in lower maintenance costs and longer operational lifespans. Furthermore, these systems contribute to improved safety by reducing the need for manual handling of heavy and potentially hazardous materials. They are widely used in power generation plants, cement factories, and other industrial facilities where coal ash is a byproduct of combustion processes.
Conclusion
Coal ash material handling systems, as exemplified by the solutions offered by Shandong HeadPowder Engineering Co., Ltd., represent a critical advancement in industrial material management. By understanding the core principles and working scene characteristics, industries can leverage these systems to enhance operational efficiency, ensure safety, and reduce environmental impact. The integration of advanced engineering and robust design ensures that these systems remain reliable and effective in the demanding environments of modern industrial operations.