

Principles and Working Scene Characteristics of Organic Salt Powder Pneumatic Conveying Equipment
HeadPowder, a leading enterprise in the field of powder handling technology, specializes in the design, manufacturing, and application of pneumatic conveying systems tailored for organic salt powders. Based in Shandong, China, the company has established itself as a reliable partner for industries requiring efficient and reliable material transport solutions. This article delves into the fundamental principles behind organic salt powder pneumatic conveying equipment and explores the key characteristics of its operational scenarios.
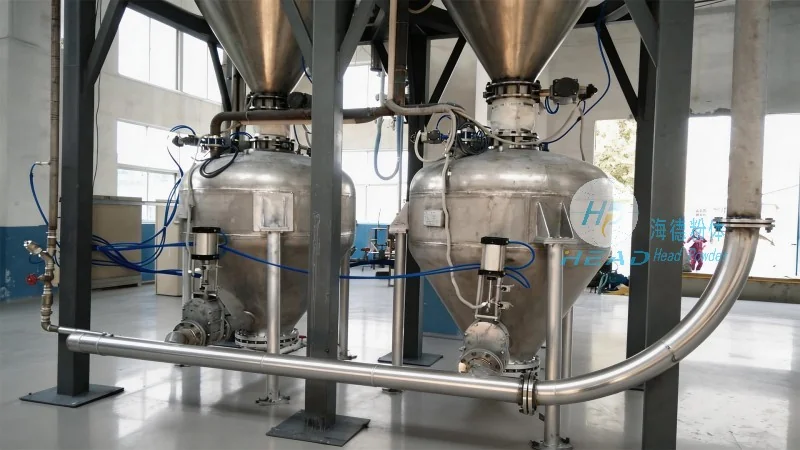
Principles of Organic Salt Powder Pneumatic Conveying Equipment
The core principle of pneumatic conveying for organic salt powders involves the use of air or gas to transport particulate materials through a pipeline system. Unlike mechanical conveying methods, which rely on physical contact and movement of components, pneumatic systems utilize pressure differentials to move the material. In the case of organic salt powders, such as sodium chloride or potassium chloride, the equipment operates by creating a flow of air that draws or pushes the powder particles through the pipeline. The system typically consists of a feeding unit, a conveying line, and a discharge unit, all working in tandem to ensure efficient material transfer.
One of the primary mechanisms employed is the dilute phase pneumatic conveying, where the powder is suspended in the air stream and transported at relatively high velocities. This method is particularly effective for organic salt powders due to their relatively low density and the need for gentle handling to prevent agglomeration or degradation. The conveying process is governed by several key parameters, including air velocity, pressure drop, and the particle size distribution of the organic salt. Proper design of the system ensures that these parameters are optimized to achieve maximum efficiency and minimal wear on the equipment components.
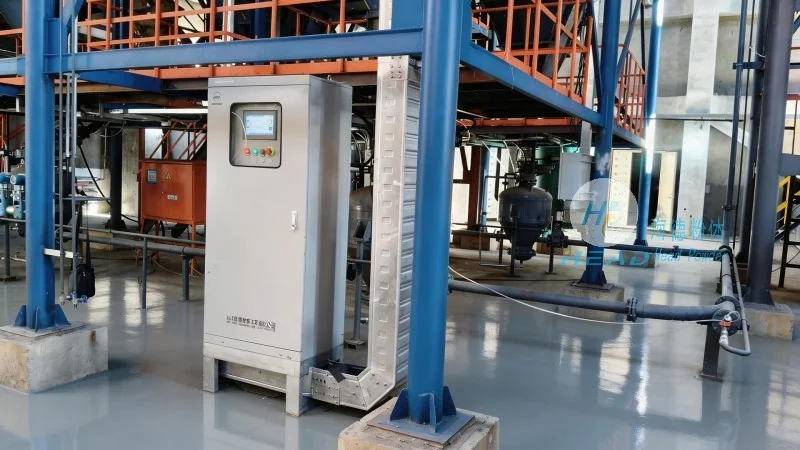
Working Scene Characteristics of Organic Salt Powder Pneumatic Conveying Equipment
The operational scenarios for organic salt powder pneumatic conveying equipment are diverse and tailored to meet the specific needs of various industrial applications. These systems are commonly used in the chemical, food, and pharmaceutical industries, where the handling of organic salt powders requires strict control over moisture, temperature, and contamination. The equipment is designed to operate in environments where hygiene and product purity are paramount, making it suitable for applications such as food processing, where organic salts are used as flavor enhancers or preservatives.
In the chemical industry, organic salt powders are often used as raw materials for the production of other chemicals, and the pneumatic conveying system ensures that these materials are transported safely and efficiently from storage silos to processing units. The system's ability to handle large volumes of material with minimal human intervention makes it ideal for continuous production lines. Additionally, the equipment is capable of operating under varying conditions, such as different particle sizes and moisture levels, which is crucial for maintaining consistent product quality.
Another key characteristic is the flexibility of the system in terms of layout and integration with existing infrastructure. The pneumatic conveying lines can be customized to fit the spatial constraints of a facility, allowing for horizontal, vertical, or combination (horizontal and vertical) conveying paths. This adaptability is essential for industries where space is limited, and the equipment can be installed in a way that optimizes the flow of materials without disrupting existing operations. The system also offers advantages in terms of energy efficiency and cost-effectiveness, as it reduces the need for manual handling and minimizes material loss during transport.
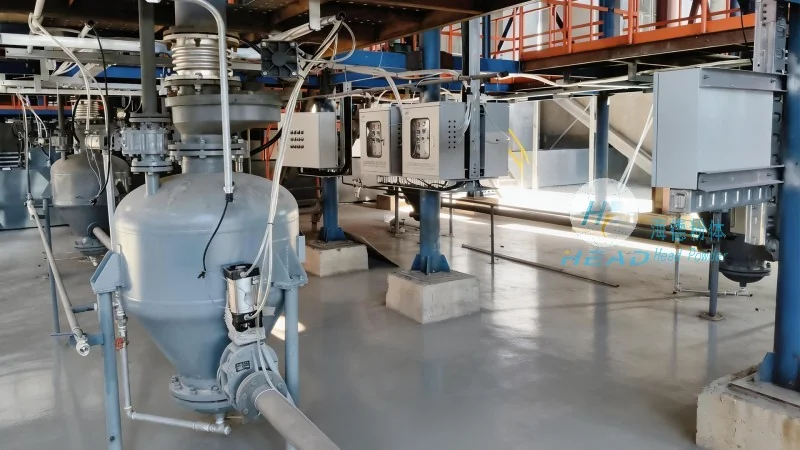
Product Introduction: Organic Salt Powder Pneumatic Conveying Equipment
HeadPowder's organic salt powder pneumatic conveying equipment is engineered to provide reliable and efficient material transport solutions for industries dealing with organic salt powders. The system is designed to handle a wide range of particle sizes and moisture contents, ensuring that the organic salt powders are conveyed without degradation or agglomeration. Key features include a robust feeding mechanism that minimizes material buildup and a high-efficiency air filtration system that maintains product purity. The conveying line is constructed from materials resistant to corrosion and wear, such as stainless steel, which is essential for handling organic salts that may be corrosive or abrasive.
The equipment operates under controlled pressure and temperature conditions, which are critical for maintaining the quality of the organic salt powders. The system includes advanced control panels that allow for real-time monitoring and adjustment of conveying parameters, ensuring optimal performance. This level of control is particularly important in industries where product consistency is non-negotiable, such as food and pharmaceutical manufacturing. Additionally, the equipment is designed for easy maintenance and cleaning, which is essential for meeting regulatory standards and ensuring long-term operational reliability.