

Principle and Working Scene Characteristics of Material Pneumatic Conveying System for Tonne Bag Unl
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, specializes in industrial material handling solutions. The company is headquartered in Shandong, China, and has developed advanced pneumatic conveying systems tailored for tonne bag unloading stations. These systems are designed to efficiently transfer bulk materials from large bags into processing or storage facilities, ensuring smooth and reliable material flow in various industrial applications.
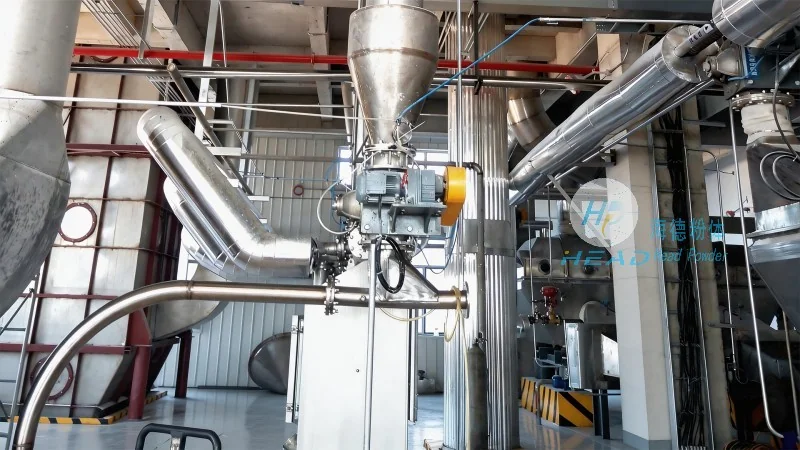
Principle of Pneumatic Conveying for Tonne Bag Unloading
The core principle of the material pneumatic conveying system for tonne bag unloading stations is the use of air pressure or vacuum to transport bulk materials. In a typical setup, a tonne bag is placed on a hopper or a dedicated unloading platform. The system then uses a combination of positive pressure (blowers or compressors) or negative pressure (vacuum pumps) to create a flow of air that carries the material particles through a pipeline network. The system includes components such as bag openers, hoppers, airlocks, and conveying lines, all working in tandem to ensure efficient material transfer. The air velocity and pressure are carefully controlled to prevent material degradation, blockages, or loss during the conveying process. This principle allows for a continuous, automated operation that minimizes manual handling and reduces the risk of dust exposure and material contamination.
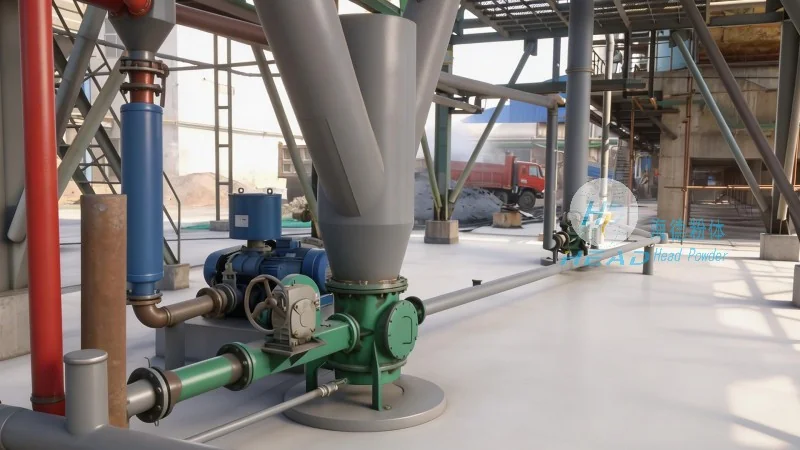
Working Scene Characteristics of the System
The working scene characteristics of the tonne bag unloading station pneumatic conveying system are tailored to meet the demands of industrial environments where bulk materials are frequently handled. These systems are commonly used in sectors such as chemical, food, pharmaceutical, and mining industries, where large quantities of powders or granules need to be transferred from storage bags to processing equipment. The key characteristics include high capacity, which can handle large volumes of material per hour, and flexibility in terms of material types, as the system can be adapted to transport various bulk materials like plastics, chemicals, food products, and minerals. Another important characteristic is the ability to maintain a closed system, which helps in controlling dust emissions and ensuring compliance with environmental regulations. The system also offers easy integration with existing production lines, allowing for seamless material flow from unloading to processing stages. Additionally, the design of the system prioritizes safety and maintenance, with features like automatic bag opening, airlock mechanisms to prevent backflow, and easy access for cleaning and maintenance, ensuring long-term operational reliability.
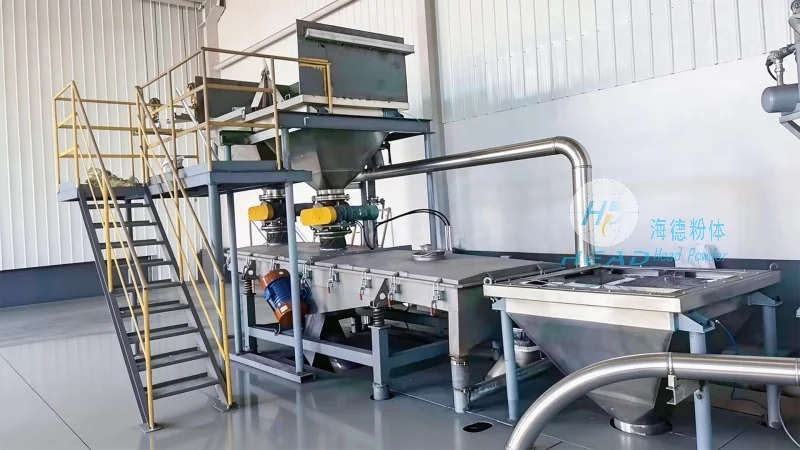
Advantages and Applications in Industrial Settings
The pneumatic conveying system for tonne bag unloading stations offers several advantages that make it a preferred choice in industrial applications. One of the primary benefits is the reduction in manual labor, as the system automates the entire unloading and conveying process, from bag opening to material transfer. This not only improves operational efficiency but also enhances workplace safety by minimizing human exposure to dust and heavy lifting. Another advantage is the ability to handle a wide range of material properties, including fine powders, coarse granules, and even sticky or abrasive materials, without causing damage or blockages. The system also provides a clean and hygienic transfer process, which is crucial in industries like food and pharmaceuticals where contamination control is paramount. In terms of applications, these systems are widely used in chemical plants for transferring raw materials, in food processing facilities for handling ingredients, and in mining operations for transporting ore from storage bags to processing equipment. The adaptability of the system to different material types and production scales makes it a versatile solution for various industrial needs.
Conclusion and Company Expertise
Shandong HeadPowder Engineering Co., Ltd. has established itself as a leading provider of advanced material handling solutions, with a focus on developing efficient and reliable pneumatic conveying systems for tonne bag unloading stations. The company's expertise lies in understanding the specific requirements of industrial applications and designing systems that meet both operational efficiency and safety standards. By leveraging cutting-edge technology and rigorous engineering, headpowder ensures that its pneumatic conveying systems deliver consistent performance, minimal downtime, and long-term value to its clients. The company's commitment to innovation and customer satisfaction has made it a trusted partner in the industrial material handling sector, helping businesses optimize their material flow processes and enhance overall productivity.