

Principle and Application Characteristics of Positive Pressure Dense Phase Pneumatic Conveying Equip
Positive pressure dense phase pneumatic conveying systems represent a sophisticated solution for transporting bulk materials efficiently and reliably. This technology, widely utilized in various industrial sectors, combines the principles of pneumatic transport with dense phase conveying to achieve optimal material handling performance. The core of this system lies in its ability to maintain a high solids concentration within the conveying pipeline, which significantly enhances the efficiency of material transport while minimizing the risk of material degradation or blockage.
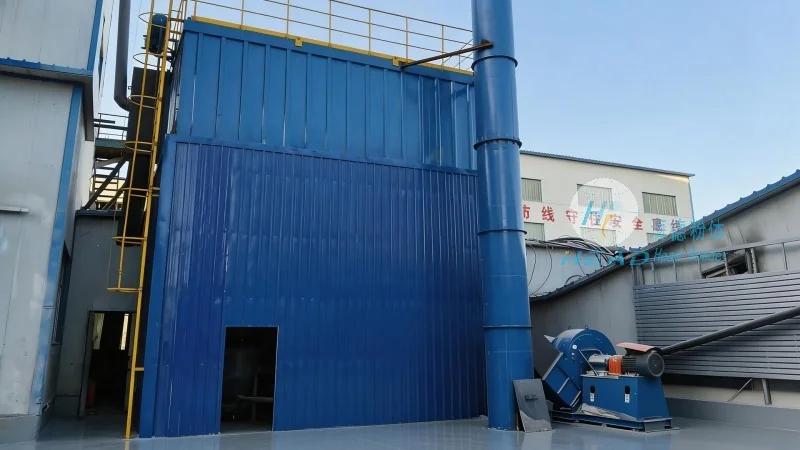
Principle of Positive Pressure Dense Phase Pneumatic Conveying
The fundamental principle of positive pressure dense phase pneumatic conveying involves the use of compressed air to transport bulk materials through a pipeline. Unlike traditional dilute phase systems that rely on low solids concentration and high air velocity, dense phase conveying operates at a much higher solids loading. This is achieved by injecting air at a controlled rate into the conveying line, often near the discharge point, to create a plug flow of material. The positive pressure generated by the air compressor ensures that the material moves forward under pressure, reducing the likelihood of air leakage and ensuring consistent flow rates. The system typically includes a hopper, a rotary valve, a conveying line, and a receiver, all working in tandem to facilitate the smooth transfer of materials.
Key Components and Their Functions
Several critical components are integral to the operation of a positive pressure dense phase pneumatic conveying system. The hopper serves as the storage and feeding unit, where bulk materials are loaded and prepared for transport. The rotary valve, positioned at the bottom of the hopper, controls the flow of material into the conveying line, ensuring a steady and controlled feed rate. The conveying line, usually made of stainless steel or other corrosion-resistant materials, is designed to withstand the pressure and friction from the material flow. The air compressor provides the necessary compressed air, which is regulated to maintain the optimal pressure and flow conditions. The receiver, located at the destination, collects the conveyed material and may include a discharge valve or other equipment for further processing.
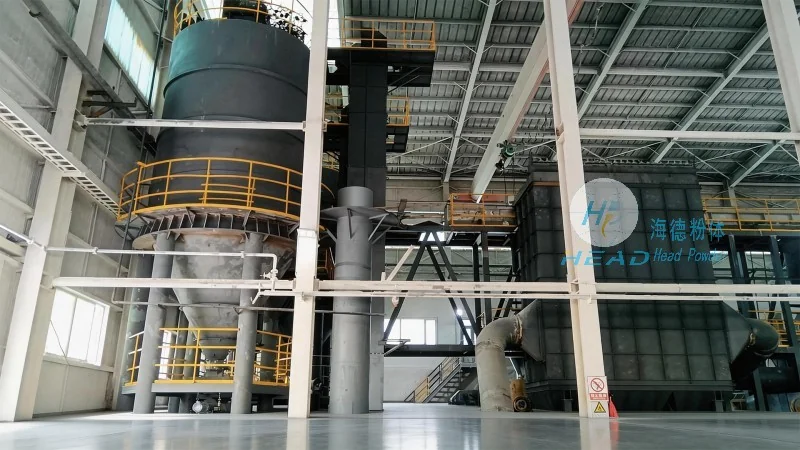
Advantages of Positive Pressure Dense Phase Conveying
Positive pressure dense phase pneumatic conveying offers numerous advantages over other material handling methods. One of the most significant benefits is the ability to transport materials over long distances with minimal degradation. The high solids concentration reduces the exposure of material to air, preventing issues such as caking, agglomeration, or moisture absorption. Additionally, this system is highly efficient in terms of energy consumption, as it requires less air volume compared to dilute phase systems, resulting in lower operational costs. The positive pressure environment also minimizes the risk of material spillage or leakage, enhancing safety and environmental compliance. Furthermore, the system is versatile and can handle a wide range of materials, including powders, granules, and even abrasive or corrosive substances, making it suitable for diverse industrial applications.
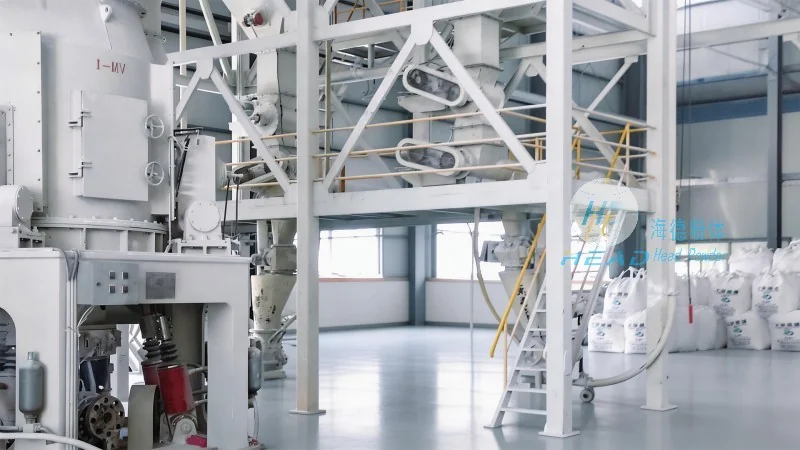
Application Characteristics and Industry Use Cases
The application characteristics of positive pressure dense phase pneumatic conveying make it particularly suitable for specific industrial scenarios. In the chemical industry, for example, this system is commonly used to transport powders and granules that are sensitive to moisture or air exposure, such as pharmaceuticals, food products, and fine chemicals. The ability to maintain a dry and clean environment during transport is crucial in these applications, as it helps preserve the quality and integrity of the materials. In the mining and minerals sector, dense phase conveying is employed to transport bulk ores and concentrates from processing plants to storage facilities or for further processing. The system's ability to handle abrasive materials and maintain high throughput makes it an ideal choice for these demanding applications. Similarly, in the food and beverage industry, positive pressure dense phase conveying is used to transport ingredients like flour, sugar, and spices, ensuring that the materials remain fresh and free from contamination. The system's hygienic design and ability to prevent cross-contamination are key factors in meeting industry standards and regulations.
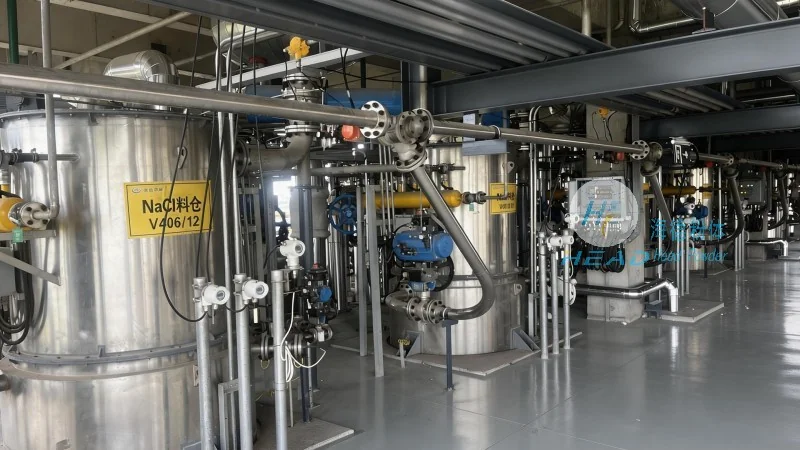
Operational Considerations and Maintenance
While positive pressure dense phase pneumatic conveying offers significant benefits, proper operation and maintenance are essential to ensure optimal performance and longevity of the system. Regular inspection of components such as the rotary valve, conveying line, and air compressor is necessary to detect and address any potential issues before they escalate. The hopper and receiver should be cleaned periodically to prevent material buildup and ensure smooth operation. The air compressor should be maintained according to the manufacturer's specifications to ensure consistent pressure and flow. Additionally, monitoring the system's performance, such as flow rates and pressure levels, can help identify any deviations from normal operation and allow for timely adjustments. Proper training of operators on the system's operation and safety procedures is also critical to prevent accidents and ensure efficient performance.
Conclusion
Positive pressure dense phase pneumatic conveying is a highly effective and versatile material handling solution that offers numerous advantages over traditional methods. Its ability to transport bulk materials efficiently, with minimal degradation and high reliability, makes it an ideal choice for various industrial applications. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality positive pressure dense phase pneumatic conveying systems tailored to the specific needs of clients. With a focus on innovation and customer satisfaction, HeadPowder ensures that its systems meet the highest standards of performance and durability, providing long-term value to its clients in China and beyond.