

Principle and Working Scene Characteristics of River Sand Material Pneumatic Conveying Machine
HeadPowder Engineering Co., Ltd. specializes in the design and manufacturing of advanced pneumatic conveying systems tailored for handling river sand and other granular materials. This article explores the fundamental principles behind these systems and highlights key working scene characteristics that make them suitable for various industrial applications.
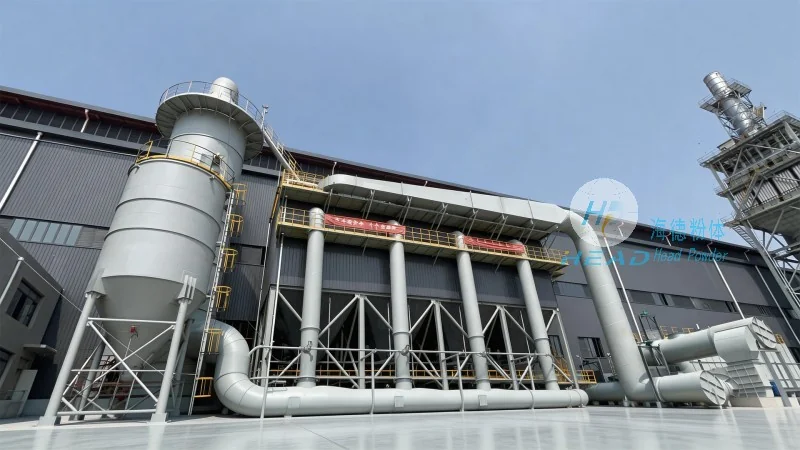
Understanding the Core Principle of Pneumatic Conveying for River Sand
The pneumatic conveying system operates by transporting bulk materials like river sand through a pipeline using pressurized air or vacuum. The process involves several key components, including a material feed hopper, a conveying pipeline, a control valve, and a discharge outlet. When air is introduced into the system, it creates a flow that lifts and moves the sand particles through the pipeline. This method eliminates the need for mechanical components such as belts or buckets, reducing maintenance requirements and increasing operational efficiency. The principle of fluidization, where the sand particles are suspended in the air stream, is central to the effectiveness of the system. By controlling the air pressure and flow rate, operators can precisely regulate the speed and direction of the material transport, ensuring consistent and reliable performance.
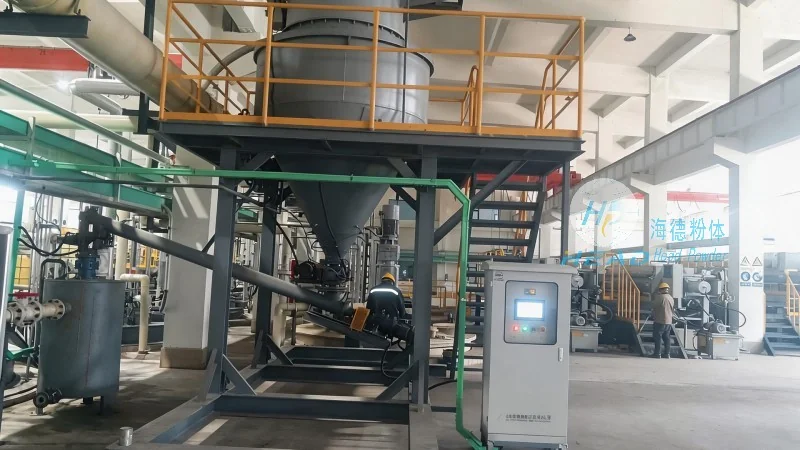
Key Working Scene Characteristics of River Sand Pneumatic Conveying Systems
Several distinct characteristics define the working scenes where river sand pneumatic conveying systems are most effective. First, the system's ability to handle abrasive materials without significant wear on components is a critical advantage. River sand, being a coarse and abrasive granular material, can cause wear on traditional conveyor systems, but pneumatic conveying minimizes this issue by using flexible pipelines and specialized air filtration. Second, the system's adaptability to different operational environments is notable. It can be installed in both indoor and outdoor settings, making it suitable for construction sites, mining operations, and processing plants located in various geographic locations. Third, the system's capacity to transport materials over long distances with minimal loss is another key characteristic. Unlike traditional belt conveyors, which may experience material spillage or degradation over extended distances, pneumatic conveying maintains the integrity of the river sand, ensuring that the material reaches its destination in optimal condition. Fourth, the system's integration with other processing equipment is seamless. It can be easily connected to storage silos, processing units, or packaging machinery, enabling a streamlined workflow from material intake to final product delivery. Finally, the system's energy efficiency compared to other transport methods is a significant benefit. By using compressed air as the primary power source, the system operates with lower energy consumption and reduced operational costs, making it an economically viable solution for large-scale river sand handling.

Applications and Operational Scenarios
River sand pneumatic conveying systems are widely used in various operational scenarios across different industries. In the construction sector, these systems are commonly employed to transport sand from stockpiles to mixing plants or concrete production facilities. The ability to move large volumes of sand quickly and efficiently supports the high demand for construction materials in urban and rural areas. In the mining industry, the system is utilized to transport sand from mining sites to processing plants or storage areas, ensuring a continuous supply of raw materials for further processing. Additionally, in the manufacturing of building materials, such as cement or plaster, the pneumatic conveying system plays a crucial role in transporting sand to mixing and grinding units, contributing to the production of high-quality building products. The versatility of the system allows it to adapt to different operational scales, from small-scale construction projects to large industrial operations, making it a reliable choice for various applications.
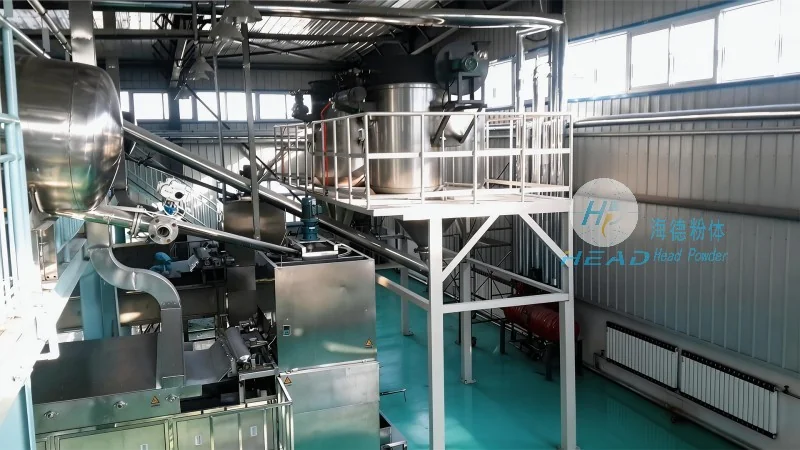
Company Overview: HeadPowder Engineering Co., Ltd.
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a leading manufacturer of pneumatic conveying systems for bulk material handling. The company specializes in customizing solutions to meet the specific needs of clients, particularly in the handling of river sand and other challenging granular materials. With a focus on innovation and quality, HeadPowder provides advanced equipment that combines efficiency, durability, and reliability. The company's products are designed to withstand the harsh conditions associated with river sand handling, ensuring long-term performance and minimal downtime. HeadPowder's commitment to customer satisfaction and technical excellence has established it as a trusted partner in the industry, providing solutions that enhance operational efficiency and reduce costs for its clients.