

Operation Process and Working Principle of Phosphate Powder Material Conveying System
Phosphate fertilizer powder is a critical raw material in the agricultural sector, and efficient transportation of this material is essential for maintaining production efficiency and ensuring product quality. The phosphate powder conveying system, designed by Shandong HeadPowder Engineering Co., Ltd., addresses the unique challenges associated with handling fine, abrasive powders like phosphate. This system integrates advanced engineering principles to ensure reliable, low-maintenance operation while minimizing material loss and environmental impact.
Key Components and Their Roles
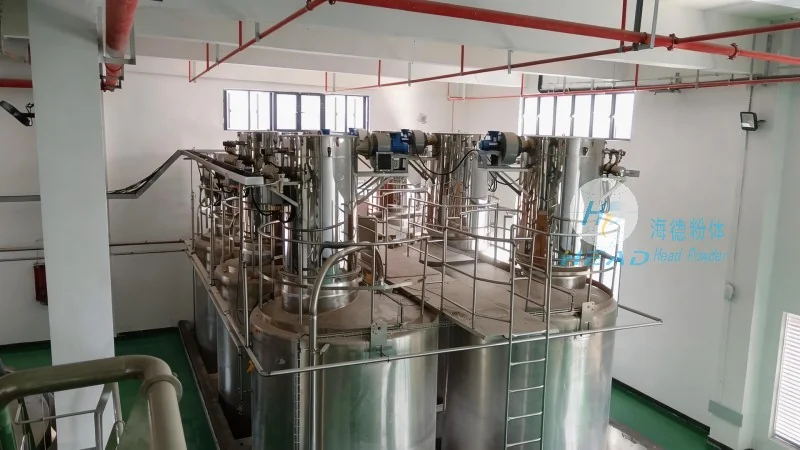
The phosphate powder conveying system consists of several key components, each playing a vital role in the overall operation. The primary components include a hopper for material storage, a feeder to control the flow rate, a conveyor mechanism (such as a screw conveyor or pneumatic system), and a control panel for monitoring and adjusting the process. The hopper is designed with a sloped bottom to facilitate material discharge, while the feeder ensures a consistent and controlled feed rate, preventing overloading or underfeeding of the conveyor. The conveyor mechanism transports the phosphate powder from the storage area to the processing or packaging units. The control panel allows operators to adjust parameters such as flow rate, pressure, and speed, ensuring optimal performance under varying load conditions.
Operation Process: Step-by-Step
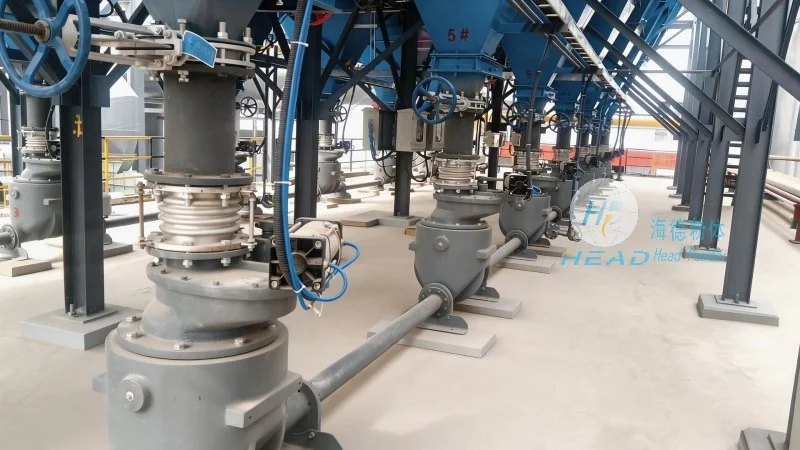
The operation of the phosphate powder conveying system follows a systematic process to ensure smooth and efficient material transport. The process begins with material loading into the hopper. The material is then discharged from the hopper into the feeder, where the flow rate is controlled by adjusting the feeder's speed or position. The feeder delivers the phosphate powder to the conveyor mechanism, which transports the material to the next stage of the process. The conveyor system may use a screw or belt mechanism, depending on the specific design, to move the powder through the system. The material is then discharged at the receiving end, where it is further processed or packaged. Throughout the process, the control panel monitors key parameters such as pressure, flow rate, and temperature, providing real-time feedback to the operator. Any deviations from the set parameters are immediately detected and corrected, ensuring consistent performance.

Working Principle: How It Functions
The working principle of the phosphate powder conveying system is based on mechanical or pneumatic forces to move the material. In mechanical systems, a screw or belt conveyor uses rotational motion to push the powder forward. The screw conveyor, for example, consists of a rotating screw inside a tube, which moves the material along the length of the conveyor. The speed of the screw and the diameter of the tube determine the flow rate and capacity of the system. In pneumatic systems, compressed air is used to create a flow of air that carries the phosphate powder through a pipeline. The air pressure and flow rate are controlled to ensure the material is transported efficiently without clogging or degradation. The system also incorporates features such as air locks and filters to prevent material leakage and maintain air quality. The control system integrates sensors and actuators to regulate the operation, ensuring the system operates within safe and efficient parameters.
Advantages of the Phosphate Powder Conveying System
Shandong HeadPowder Engineering Co., Ltd.'s phosphate powder conveying system offers several advantages over traditional methods of material transport. The system is designed to handle fine, abrasive powders without causing wear and tear on components, extending the lifespan of the equipment. The controlled flow rate and consistent operation reduce material loss and improve product quality. The system is also energy-efficient, with minimal power consumption compared to other conveying methods. Additionally, the system is easy to maintain, with accessible components and simple adjustment mechanisms. The integration of a control panel allows for real-time monitoring and adjustment, reducing downtime and increasing overall productivity. The system is also environmentally friendly, with features such as air filters and sealed containers to minimize dust emissions and prevent environmental contamination.
Company Information and Contact
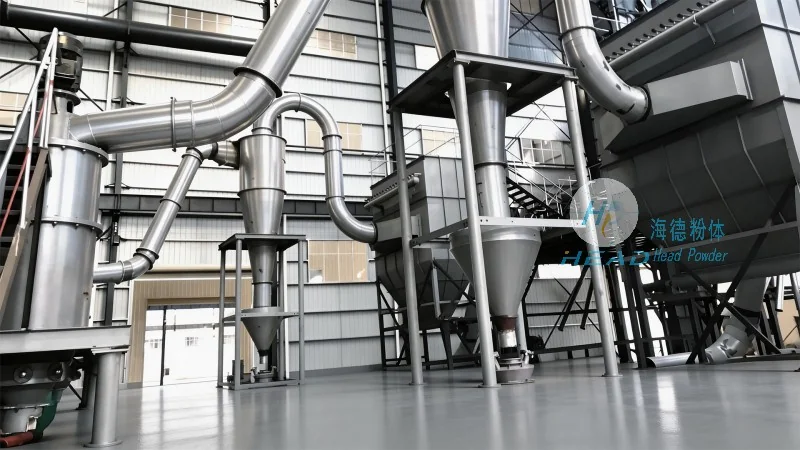
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer of phosphate powder conveying systems, specializing in the design and production of equipment for the agricultural and fertilizer industries. The company is located in Shandong, China, and has a strong reputation for quality, reliability, and customer satisfaction. HeadPowder provides comprehensive solutions for material handling, including conveyor systems, storage tanks, and processing equipment. The company's team of engineers and technicians is dedicated to developing innovative solutions that meet the specific needs of clients, ensuring optimal performance and efficiency. For more information about the phosphate powder conveying system or other products, please contact HeadPowder directly.