

Operation Process and Working Principle of Environmental-Friendly Powder Pneumatic Conveying
Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in the field of powder handling technology, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems. Based in Shandong, China, the company focuses on providing environmentally friendly solutions for the efficient and safe transport of bulk powders. This article delves into the operation process and working principle of their environmental-friendly powder pneumatic conveying systems, highlighting the key components, operational steps, and the underlying technology that ensures optimal performance and sustainability.
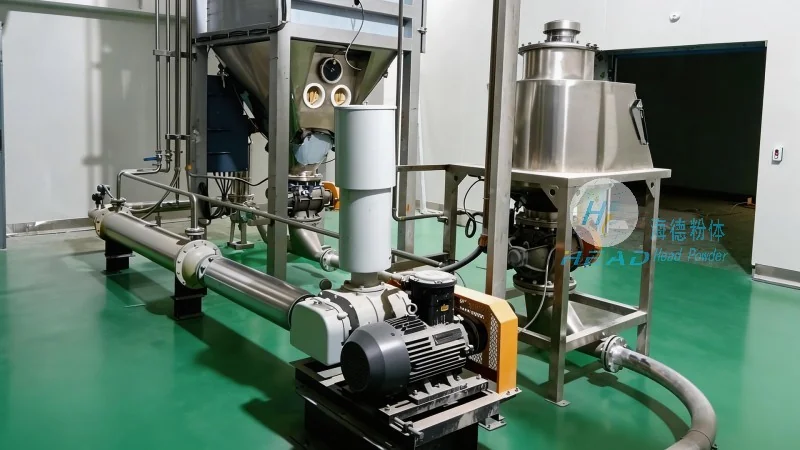
The Core Components of the Pneumatic Conveying System
The environmental-friendly powder pneumatic conveying system by HeadPowder typically consists of several critical components that work in tandem to achieve efficient material transport. These components include a dust collector, a blower or compressor, a conveying line (often equipped with bends and filters), and a receiving hopper or container. Each component plays a vital role in the overall system, ensuring that the process is both effective and environmentally responsible.
Operation Process of the Environmental-Friendly Powder Pneumatic Conveying System
The operation process of the system begins with the loading of the bulk powder into the hopper or feeding device. The powder is then drawn into the conveying line by the air flow generated by the blower. As the air moves through the system, it carries the powder particles along the pipeline. The system is designed to maintain a consistent air velocity to prevent particle segregation and ensure smooth transport. At the receiving end, the powder is deposited into the target container, while the air is filtered and returned to the system or released safely. This continuous cycle allows for the reliable and efficient transfer of powders without the need for mechanical parts that may cause wear or contamination.
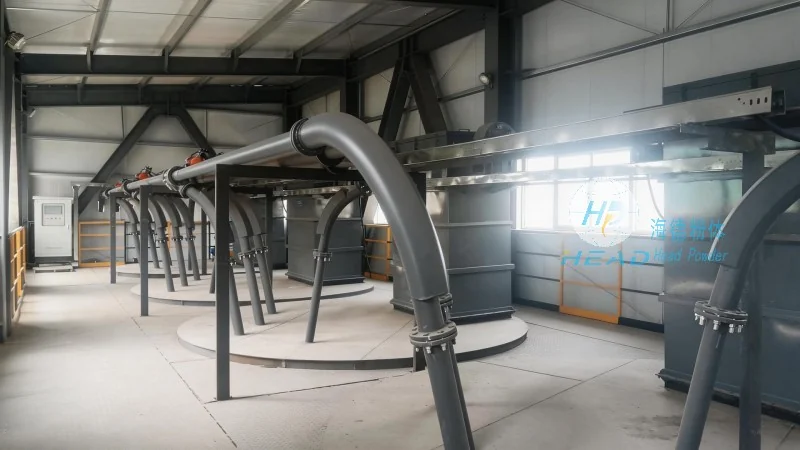
The Working Principle of the Pneumatic Conveying System
The working principle of the environmental-friendly powder pneumatic conveying system is based on the fundamental physics of fluid dynamics and particle movement. The system utilizes compressed air or gas to create a flow that propels the powder particles through the conveying line. The key to its operation lies in the balance between the air velocity and the particle size, density, and moisture content. By maintaining an appropriate air velocity, the system can transport powders over long distances and through complex layouts without the need for additional mechanical equipment. The environmental aspect is addressed through the use of efficient filtration systems that capture dust and particulate matter, ensuring that the air released back into the environment is clean and compliant with regulatory standards. This approach not only enhances the safety of the operation but also reduces the environmental impact associated with traditional bulk material handling methods.
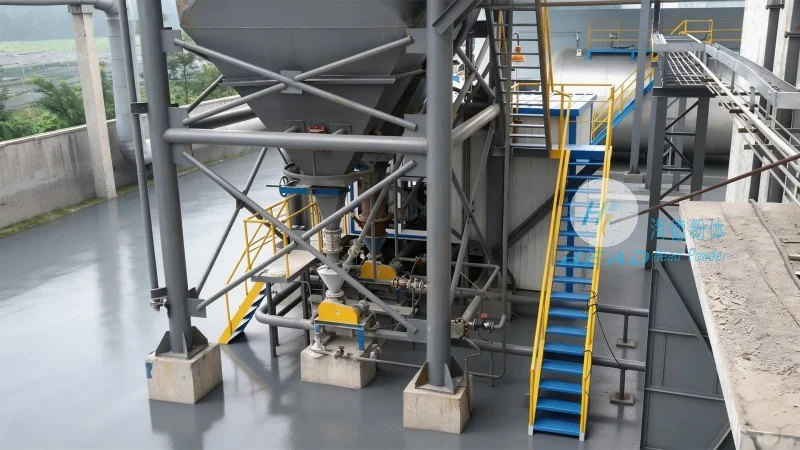
Key Advantages and Environmental Benefits
HeadPowder's environmental-friendly powder pneumatic conveying systems offer several advantages over traditional mechanical conveying methods. The primary benefit is the reduction in the need for moving parts, which minimizes wear and tear and lowers maintenance costs. Additionally, the system eliminates the risk of cross-contamination between different powders, as the air is filtered and recycled. From an environmental perspective, the system significantly reduces dust emissions compared to traditional methods, contributing to better air quality and compliance with environmental regulations. The use of energy-efficient blowers and optimized air flow further enhances the sustainability of the operation, making it a cost-effective and eco-friendly solution for bulk powder handling.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. provides advanced and environmentally friendly powder pneumatic conveying solutions that are designed to meet the needs of modern industrial applications. By understanding the operation process and working principle of these systems, users can appreciate the efficiency, reliability, and sustainability that HeadPowder's technology offers. Whether for pharmaceutical, food, or industrial applications, the company's systems ensure that bulk powders are transported safely and effectively, while minimizing the environmental impact and operational costs.