

Pneumatic Conveying Solutions for Stone Material Transport
Efficient and reliable transport of stone materials such as aggregates, gravel, and crushed stone is a critical aspect of operations in the construction, mining, and aggregate industries. Traditional methods like conveyor belts and trucks often face challenges related to maintenance, space constraints, and material loss. Pneumatic conveying systems offer a modern solution by utilizing air pressure to move bulk materials through a network of pipes, providing a seamless and enclosed transport process. This approach not only enhances operational efficiency but also reduces labor costs and environmental impact. For businesses seeking to optimize their material handling processes, pneumatic conveying systems present a compelling alternative to conventional methods.
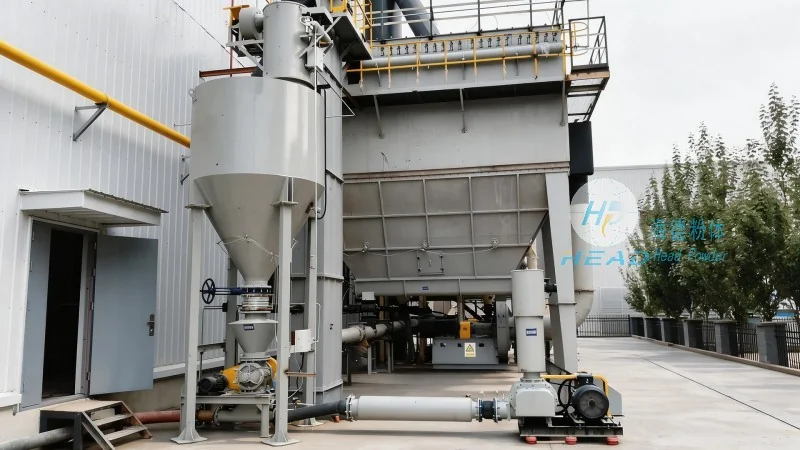
About HeadPowder Engineering Co., Ltd.
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a leading engineering firm specializing in the design and implementation of material handling solutions. With headquarters in Shandong, China, the company has built a strong reputation for delivering high-quality, customized pneumatic conveying systems tailored to the unique needs of the stone industry. HeadPowder’s team of experienced engineers and technicians brings extensive knowledge in fluid dynamics, material science, and industrial automation, enabling the development of innovative solutions that address the specific challenges faced by clients. The company’s commitment to customer satisfaction and technical excellence has made it a preferred choice for businesses looking to enhance their operational capabilities.
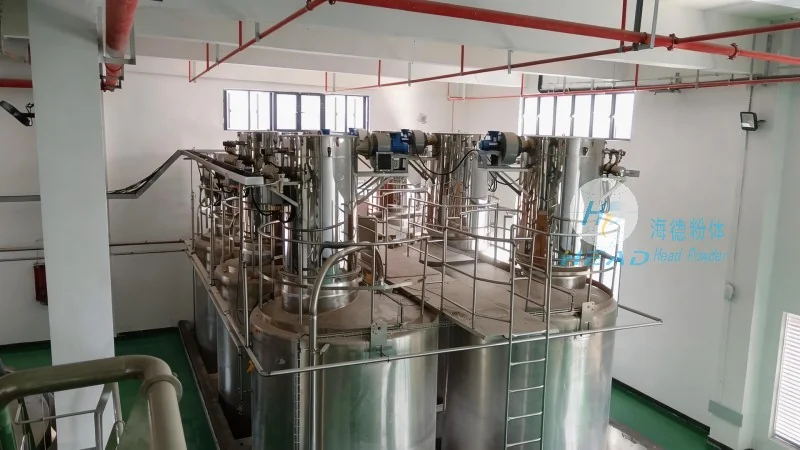
Key Features of Stone Pneumatic Conveying Solutions
HeadPowder’s pneumatic conveying solutions for stone materials are engineered with several advanced features that ensure optimal performance and durability. The systems are designed to handle a wide range of particle sizes, from fine powders to large aggregates, with consistent and reliable transport. Advanced control systems, including variable frequency drives and pressure sensors, allow for precise regulation of air flow and pressure, minimizing energy consumption while maintaining efficient material movement. The use of high-grade stainless steel and corrosion-resistant materials ensures long-term reliability, reducing the need for frequent maintenance and extending the system’s service life. Additionally, the enclosed design of the conveying lines helps in controlling dust emissions and preventing material spillage, which is essential for maintaining environmental compliance and product quality.
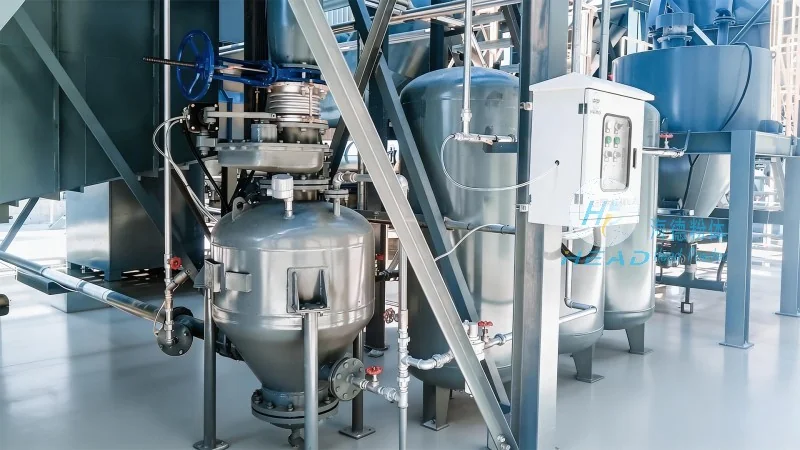
Applications in the Stone Industry
The versatility of pneumatic conveying systems makes them suitable for a variety of applications within the stone industry. In quarry operations, these systems are used to transport raw aggregates from extraction sites to processing facilities, streamlining the material flow and reducing transportation time. For construction sites, pneumatic conveyors can efficiently deliver stone materials to different work areas, such as foundations, roads, and buildings, improving workflow and reducing manual labor. In mining operations, the systems help in transporting crushed stone from processing plants to storage or shipping locations, enhancing operational productivity and reducing reliance on external transport. Furthermore, the systems are ideal for processing plants where stone materials need to be moved between different stages of production, such as crushing, screening, and storage.
Customization and Integration Services
HeadPowder understands that each project has unique requirements, and therefore, the company offers comprehensive customization and integration services to ensure that the pneumatic conveying system perfectly aligns with the client’s operational needs. This includes designing systems that can be integrated with existing infrastructure, such as existing pipelines or storage silos, minimizing the need for new construction. The company also provides support for installation, commissioning, and ongoing maintenance, ensuring that the system operates at peak efficiency from day one. By working closely with clients, HeadPowder’s engineering team can tailor the system’s design, including the type of air mover (e.g., rotary lobe blowers, positive displacement blowers), the pipe layout, and the control system, to meet specific performance criteria and budget constraints. This collaborative approach ensures that the final solution is not only efficient but also cost-effective and scalable for future growth.
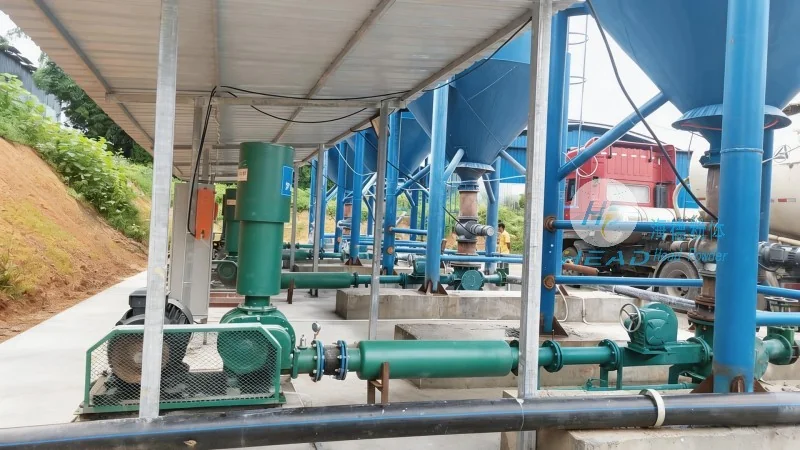
Benefits of Choosing HeadPowder’s Pneumatic Conveying Solutions
Implementing a pneumatic conveying system for stone material transport offers numerous advantages that can significantly impact a business’s bottom line. Firstly, the systems reduce operational costs by minimizing labor requirements and eliminating the need for additional equipment like trucks or conveyor belts. The enclosed nature of the conveying process also reduces material loss and dust emissions, leading to lower waste management costs and improved environmental performance. Additionally, the energy efficiency of modern pneumatic conveying systems results in lower utility bills compared to traditional methods, contributing to long-term cost savings. Furthermore, the compact design of the systems allows for installation in limited spaces, making them suitable for urban or space-constrained environments where traditional conveyors may not fit. The reliability of these systems, with minimal downtime and maintenance needs, ensures consistent production and reduces the risk of project delays. Overall, HeadPowder’s pneumatic conveying solutions provide a sustainable and efficient approach to stone material transport, helping businesses enhance their operational capabilities and achieve their strategic goals.