

What is Sugar Cane White Sugar Pneumatic Conveying? An Introduction to the Working Principle of Powd
White sugar, a staple in the food and beverage industry, often requires efficient and hygienic transportation from production to packaging. Pneumatic conveying, a method that uses air to move bulk materials like sugar, offers a solution that combines speed, cleanliness, and minimal product contamination. This article delves into the mechanics of sugar cane white sugar pneumatic conveying, explaining how such systems operate and why they are essential in modern powder handling.
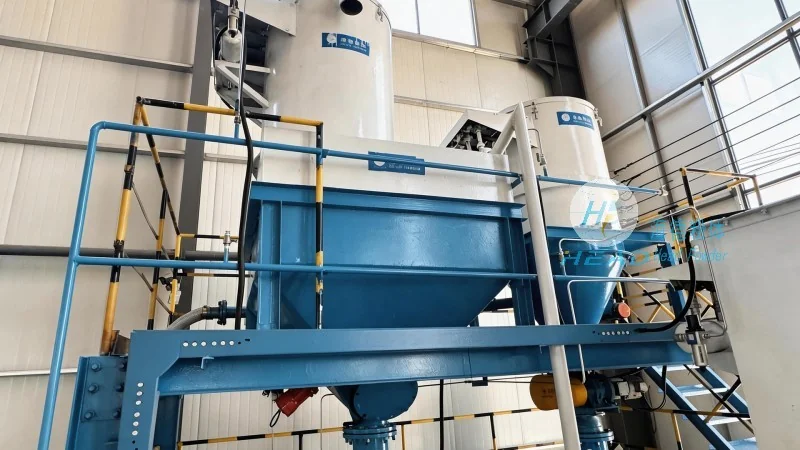
About HeadPowder: Your Expert in Powder Handling Solutions
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, is a leading provider of advanced powder handling systems. With a focus on innovation and reliability, the company specializes in designing, manufacturing, and installing pneumatic conveying equipment tailored to the unique needs of the sugar and food processing industries. Their expertise ensures that clients receive systems that are not only efficient but also compliant with industry standards for hygiene and safety.
The Core Components of a Pneumatic Conveying System for Sugar
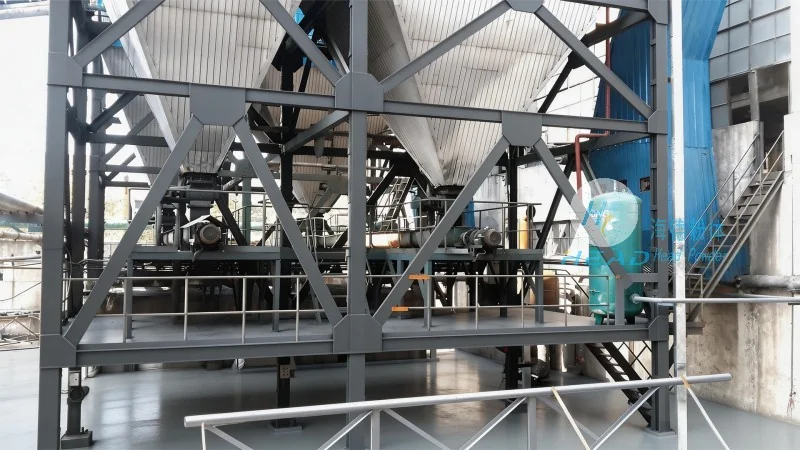
A typical pneumatic conveying system for white sugar consists of several key components that work in tandem to move the product. The primary elements include a hopper or storage silo, a conveyor line (either positive or negative pressure), a dust collector, and a control system. The hopper stores the sugar, feeding it into the system as needed. The conveyor line, which can operate under positive pressure (where air pushes the sugar forward) or negative pressure (where air is drawn through the system), is the heart of the operation. A dust collector is crucial for maintaining air quality and preventing product loss, while the control system manages the flow rate and pressure to ensure smooth operation.
How the Pneumatic Conveying Process Works
The process begins with the sugar being discharged from the storage hopper into the conveyor line. In a positive pressure system, a fan or blower generates high-pressure air that forces the sugar particles through the pipeline. The air-sugar mixture travels to the destination, such as a silo or packaging machine, where the air is separated from the product. In a negative pressure system, a vacuum pump creates a low-pressure environment that draws the sugar into the pipeline. The air then carries the sugar to the receiving point, where it is deposited. The system is designed to maintain consistent flow rates, preventing clogging and ensuring that the sugar reaches its destination without degradation.
Benefits of Using Pneumatic Conveying for White Sugar
Implementing a pneumatic conveying system for white sugar offers numerous advantages over traditional methods like bucket elevators or belt conveyors. One of the most significant benefits is the hygienic nature of the process. The enclosed system minimizes exposure to contaminants, making it ideal for food-grade products. Additionally, pneumatic conveying is faster and more efficient, reducing downtime and increasing overall productivity. The system also reduces product degradation by minimizing friction and exposure to air, which can affect the quality of the sugar. Furthermore, the flexibility of the system allows for easy integration with existing production lines, making it a cost-effective solution for businesses looking to upgrade their powder handling capabilities.
Applications in the Sugar Industry
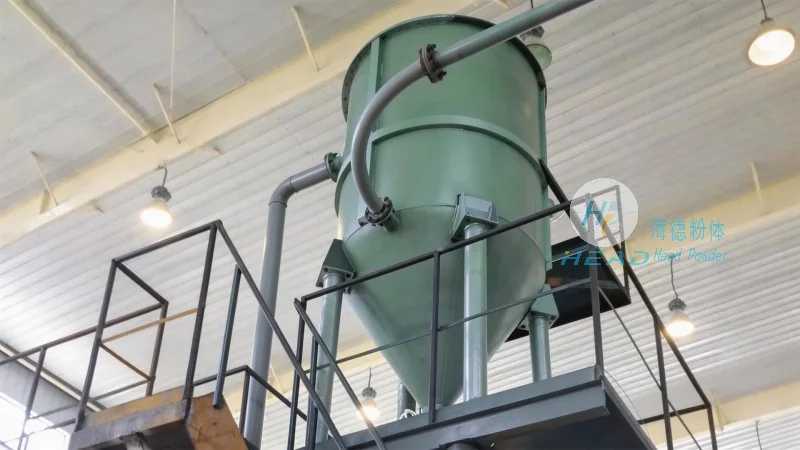
Pneumatic conveying systems are widely used in various stages of the sugar production and processing chain. From raw sugar storage and transport to refining and packaging, these systems play a critical role in maintaining the quality and consistency of the final product. In storage facilities, the systems ensure that sugar is moved from silos to processing units without the risk of cross-contamination. During refining, the systems transport refined sugar to packaging lines, where it is converted into the final consumer product. The ability to handle different sugar types, including white sugar, brown sugar, and powdered sugar, makes these systems versatile and adaptable to various production needs.
Conclusion: Choosing the Right Pneumatic Conveying Solution
For businesses in the sugar industry, selecting the right pneumatic conveying system is essential for maintaining efficiency, quality, and compliance. With companies like Shandong HeadPowder Engineering Co., Ltd. offering specialized solutions, businesses can benefit from tailored systems that meet their specific requirements. By understanding the working principles and benefits of pneumatic conveying, companies can make informed decisions that enhance their operations and ensure the long-term success of their sugar production processes.