

What is an Intelligent Tonne Bag Loading Station Powder Conveying Machine? What are its Design Princ
When it comes to handling bulk powders in industrial settings, the intelligent tonne bag loading station with a powder conveying machine represents a significant advancement in material management technology. This equipment is designed to streamline the process of receiving, storing, and transferring large quantities of powdered materials from bulk bags (tonne bags) into processing systems. Understanding its functionality and the underlying design principles is crucial for industries that rely on consistent and efficient material flow.
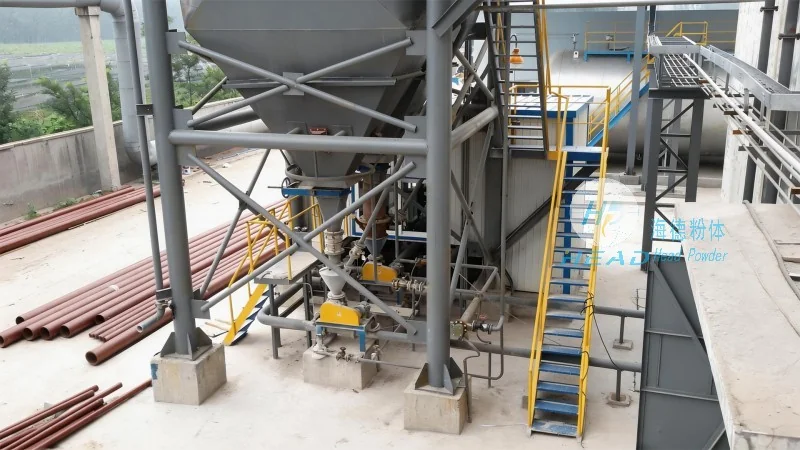
What is a Tonne Bag Loading Station? Its Core Function and Role
A tonne bag loading station is a specialized system engineered to handle the entire workflow associated with bulk bag operations. It typically includes components such as a hopper, a discharge valve, and a conveyor system that can transport the material from the bag into a storage silo or directly into a production line. The primary role of this station is to automate the process of unloading and transferring powders, reducing manual labor and minimizing the risk of contamination or material loss. For industries like pharmaceuticals, food processing, and chemical manufacturing, where material purity and safety are paramount, this equipment is indispensable.
The Design Principles Behind the Powder Conveying System
The design of an intelligent tonne bag loading station adheres to several key principles to ensure optimal performance. First, it emphasizes safety and compliance with industry standards, incorporating features like dust suppression systems and explosion-proof designs where necessary. Second, it prioritizes efficiency, using advanced control systems to manage the flow of material and reduce downtime. Third, it focuses on adaptability, allowing for integration with existing production lines and the ability to handle a wide range of powder types and bag sizes. These principles collectively contribute to a system that is both reliable and user-friendly.
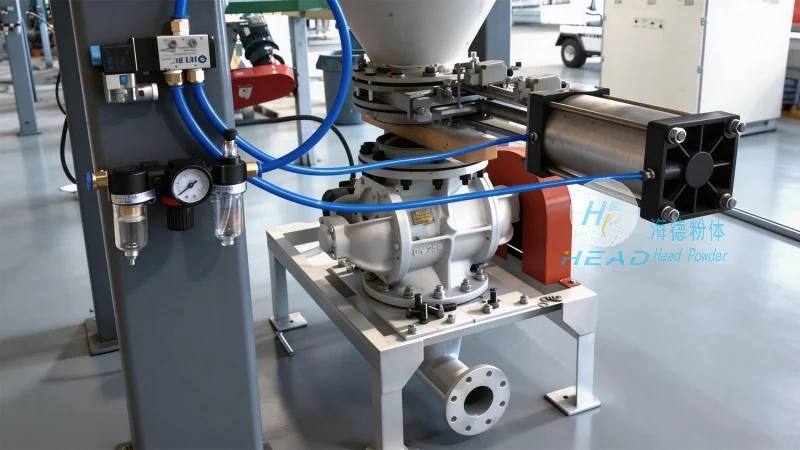
Key Components and Their Operational Mechanisms
The intelligent tonne bag loading station consists of several critical components, each playing a vital role in the overall operation. The bulk bag discharge unit, equipped with a mechanical or pneumatic valve, allows for controlled release of the material from the bag. The hopper, often lined with a suitable material to prevent material buildup or contamination, collects the discharged powder. The powder conveying machine, which can be a screw conveyor, pneumatic conveyor, or a combination of both, transports the material from the hopper to the next stage of the process. Advanced control panels enable operators to monitor and adjust the system parameters in real-time, ensuring precise control over the material flow rate and pressure.
How the System Ensures Efficient and Safe Material Handling
Efficiency in material handling is achieved through the seamless integration of all components. The system can operate continuously, processing multiple bags without the need for manual intervention between cycles. This not only increases throughput but also reduces labor costs. Safety features, such as automatic shut-off mechanisms in case of blockages or overpressure, protect both the equipment and the operators. Additionally, the system is designed to minimize dust generation, using enclosed hoppers and suction systems to maintain a clean and safe working environment. These measures ensure that the equipment meets the stringent safety and environmental regulations prevalent in modern industrial settings.
Applications and Industries Where This Equipment is Essential
The intelligent tonne bag loading station with a powder conveying machine is widely used across various industries that deal with bulk powders. In the pharmaceutical industry, it is used to handle active pharmaceutical ingredients (APIs) and excipients, ensuring that the materials are handled in a sterile and controlled environment. In the food processing sector, it is employed for handling ingredients like flour, sugar, and spices, maintaining product quality and safety. The chemical industry also benefits from this equipment when processing raw materials like fertilizers, pigments, and catalysts. In each of these applications, the system's ability to handle large volumes of material while maintaining precision and safety makes it an essential asset.
The Role of HeadPowder in Providing Advanced Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer based in Shandong, China, specializing in the design and production of advanced powder handling equipment. With years of experience in the industry, headpowder has developed a range of intelligent tonne bag loading stations that incorporate the latest technological advancements. The company's commitment to quality and innovation has made its products a preferred choice for businesses seeking reliable and efficient material handling solutions. By focusing on customer needs and adhering to international standards, headpowder ensures that its equipment not only meets but exceeds industry expectations, providing long-term value and performance.