

What is a Mobile Powder Conveying System? And What Are Its Design Principles?
Mobile powder conveying systems are essential equipment in various industrial sectors, particularly for transporting bulk powders efficiently and safely. These systems are designed to handle a wide range of powder materials, from fine powders to bulkier granules, ensuring smooth and reliable material transfer. Understanding the functionality and design principles of such equipment is crucial for industries that rely on consistent and efficient powder handling processes.
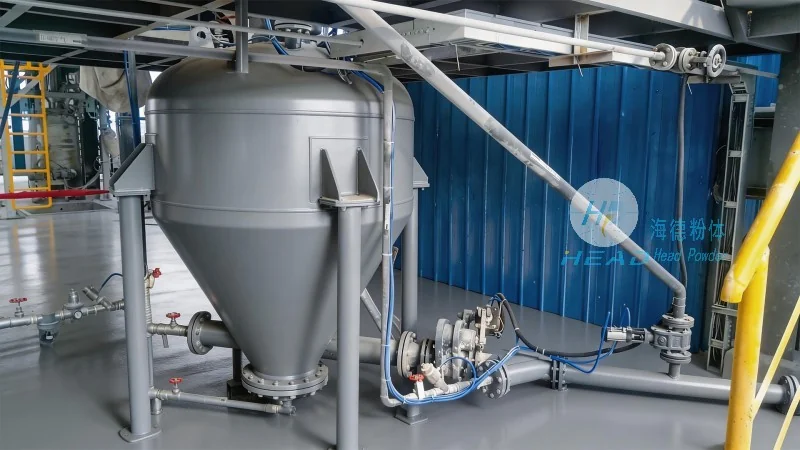
At Shandong HeadPowder Engineering Co., Ltd., we specialize in the design, manufacturing, and supply of advanced mobile powder conveying solutions. Our headquarters is located in Shandong, China, where we leverage years of industry experience to develop innovative equipment tailored to meet the diverse needs of our clients. Our team of engineers and technicians works diligently to ensure that each system we produce adheres to the highest standards of quality and performance.
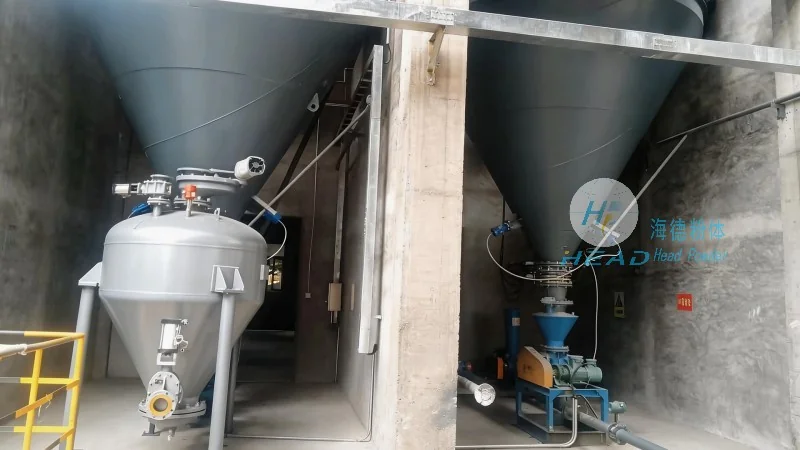
Key Design Principles of Mobile Powder Conveying Systems
The design of a mobile powder conveying system involves several critical components and principles that work in harmony to achieve efficient material transport. The primary goal is to minimize material degradation, ensure consistent flow rates, and maintain operational safety. A typical mobile system includes a hopper for material storage, a conveyor mechanism (such as a screw or pneumatic system), and a control unit for monitoring and adjusting the conveying process. The hopper is designed with a sloped bottom to facilitate smooth material discharge, preventing clogging and ensuring continuous flow. The conveyor mechanism is engineered to handle different powder characteristics, including moisture content, particle size, and density, by adjusting speed and pressure as needed. Additionally, the system incorporates safety features like overload protection and emergency stop buttons to prevent accidents and protect both personnel and equipment.
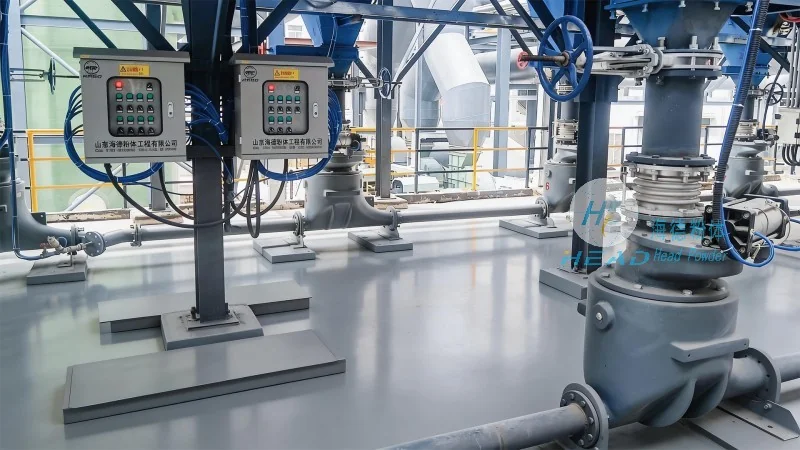
How Mobile Powder Conveying Systems Operate
Mobile powder conveying systems operate by utilizing either mechanical or pneumatic forces to move powder from the source to the destination. Mechanical systems, such as screw conveyors, rely on rotating screws to push material forward through a tube or trough. This method is ideal for transporting dry, free-flowing powders and is commonly used in industries like food processing, pharmaceuticals, and chemical manufacturing. Pneumatic systems, on the other hand, use compressed air to create a flow of material through a pipeline. These systems are particularly effective for handling fine powders or materials that are sensitive to mechanical stress, as they minimize particle breakage and contamination. The control unit in the system allows operators to adjust parameters such as conveyor speed, air pressure, and material feed rate, ensuring optimal performance under varying conditions. This flexibility makes mobile systems adaptable to different production requirements and operational environments.
Applications and Benefits of Mobile Powder Conveying Systems
Mobile powder conveying systems find applications in a wide array of industries, including food and beverage, pharmaceuticals, chemicals, and mining. In the food industry, these systems are used to transport ingredients like flour, sugar, and spices from storage to processing lines, ensuring hygienic and efficient handling. In pharmaceutical manufacturing, they are crucial for moving raw materials and finished products, maintaining strict quality control standards. The chemical industry utilizes mobile systems to handle various powders, from catalysts to pigments, while the mining sector relies on them for transporting ore and other bulk materials. The benefits of mobile powder conveying systems include increased productivity, reduced labor costs, and improved safety. By automating the material handling process, these systems minimize human error and exposure to hazardous materials, leading to a more efficient and secure operation. Additionally, the mobility of the equipment allows for easy repositioning, making it suitable for both fixed and temporary production setups.
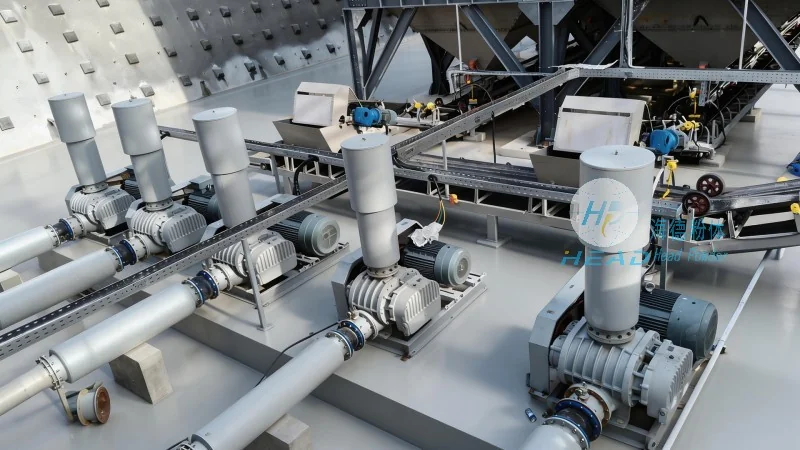
Customization and Maintenance Considerations
At Shandong HeadPowder Engineering Co., Ltd., we understand that each client has unique requirements, which is why we offer customized mobile powder conveying systems. Our engineers work closely with clients to assess their specific needs, such as material type, flow rate, and operational environment, to design a system that meets their exact specifications. We also provide comprehensive maintenance services to ensure the longevity and reliability of our equipment. Regular maintenance, including cleaning, lubrication, and component inspection, is essential to prevent breakdowns and maintain optimal performance. Our team of technicians is trained to handle all aspects of maintenance, from routine checks to major repairs, ensuring that our clients' systems operate at peak efficiency. By offering both customization and maintenance support, we aim to provide long-term solutions that enhance our clients' productivity and profitability.