

What is a Positive Pressure Powder Conveyor? And What Are Its Design Principles?
For industrial applications that require the safe and efficient transportation of bulk powders, positive pressure powder conveyors have emerged as a critical solution. These systems are designed to handle a wide range of powder types, from fine powders to bulkier materials, while ensuring minimal product loss and maintaining product integrity throughout the conveying process. Understanding the functionality and design principles of such equipment is essential for industries like pharmaceuticals, food processing, and chemical manufacturing, where material handling efficiency and safety are paramount.

Introduction to Positive Pressure Powder Conveyors
Positive pressure powder conveyors are mechanical systems that use compressed air or gas to transport dry powders in a sealed environment. The core principle involves creating a positive pressure within the conveyor line, which forces the powder from the source to the destination. This method is particularly effective for handling powders that are prone to caking, dusting, or contamination, as it prevents exposure to external air and maintains a controlled atmosphere. The system typically consists of a hopper, a conveyor tube, and a control unit, all working in tandem to ensure smooth and reliable material transport.
Key Components and Their Functions
The primary components of a positive pressure powder conveyor include the material hopper, the conveying tube, the air compressor, and the control panel. The hopper serves as the storage and feeding unit, where the powder is loaded and then discharged into the conveyor line. The conveying tube is usually made of flexible or rigid material, depending on the application, and is designed to withstand the pressure and temperature of the conveyed material. The air compressor generates the necessary pressure to move the powder, while the control panel allows operators to monitor and adjust the system's performance, such as flow rate and pressure levels. Each component plays a vital role in ensuring the efficient and safe operation of the conveyor.
Design Principles Behind Positive Pressure Conveyors
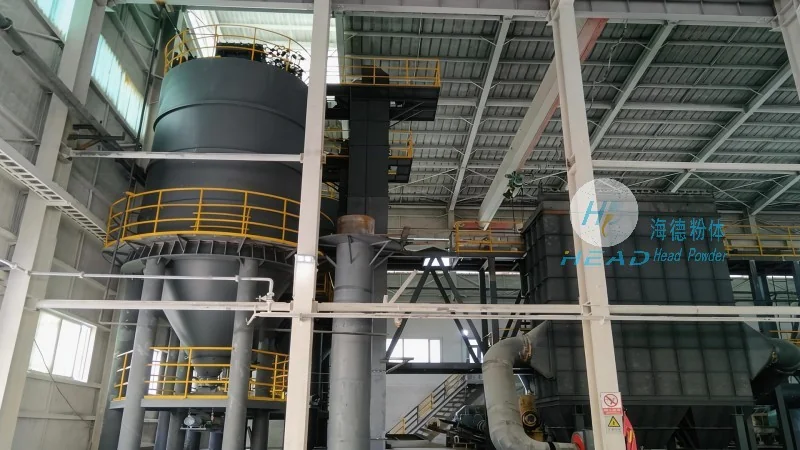
The design of a positive pressure powder conveyor is based on several key principles that optimize performance and reliability. One of the most important principles is maintaining a positive pressure gradient throughout the system. This means that the pressure inside the conveyor line is higher than the ambient pressure, which prevents air from entering the system and causing product degradation or contamination. Another critical principle is the use of a sealed system, which ensures that the powder remains contained and does not escape into the environment. The system also incorporates features like air filters and moisture control to maintain the quality of the conveyed material. Additionally, the design considers factors such as material compatibility, where the conveyor components are made from materials that do not react with the powder being transported, ensuring product purity.
Advantages of Using Positive Pressure Conveyors
Positive pressure powder conveyors offer several advantages over traditional conveying methods. One of the main benefits is the ability to handle a wide variety of powder types, including those that are sensitive to moisture or air exposure. The sealed system prevents contamination and maintains product quality, which is crucial in industries like pharmaceuticals and food processing. Another advantage is the reduced risk of product loss, as the system minimizes dust and spillage. Additionally, positive pressure conveyors are more energy-efficient compared to other methods, as they use less power to move the material. The system also allows for precise control over the flow rate, enabling operators to adjust the speed of material transport according to specific requirements. These advantages make positive pressure conveyors a preferred choice for many industrial applications.

Applications in Different Industries
Positive pressure powder conveyors are widely used across various industries due to their versatility and effectiveness. In the pharmaceutical industry, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients, ensuring that the materials remain sterile and free from contamination. In the food processing industry, they are employed to handle powders like flour, sugar, and spices, maintaining the quality and safety of the final products. The chemical industry also utilizes positive pressure conveyors to transport chemicals, including those that are hazardous or reactive. Additionally, these systems are used in the agricultural sector to handle bulk materials like fertilizers and seeds. The adaptability of positive pressure conveyors makes them suitable for a wide range of applications, from small-scale operations to large industrial plants.
Maintenance and Operational Considerations
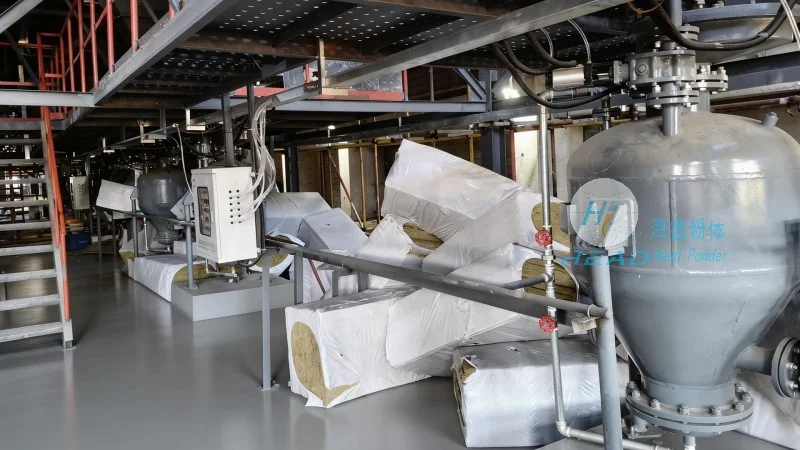
Proper maintenance is essential to ensure the long-term performance and reliability of a positive pressure powder conveyor. Regular checks of the air compressor, conveying tube, and control panel are necessary to identify and address any issues before they become major problems. The system should be cleaned regularly to prevent the buildup of powder residue, which can affect performance and product quality. Additionally, operators should monitor the pressure and flow rate to ensure that the system is operating within the recommended parameters. Proper training of personnel is also important to ensure that the system is used correctly and safely. By following these maintenance and operational guidelines, the lifespan of the conveyor can be extended, and the risk of downtime or product loss can be minimized.
As a leading manufacturer of positive pressure powder conveyors, Shandong HeadPowder Engineering Co., Ltd. specializes in providing high-quality equipment tailored to the specific needs of various industries. With a focus on innovation and customer satisfaction, the company has developed advanced systems that meet the most stringent standards for material handling. Based in Shandong, China, HeadPowder Engineering Co., Ltd. offers comprehensive solutions for bulk powder transportation, including design, manufacturing, and after-sales support. The company's commitment to quality and reliability has made it a trusted partner for many businesses in need of efficient and safe powder conveying solutions.