

What is a Red Sugar Material Handling System? What are its Design Principles?
For sugar manufacturers, the efficient and reliable transportation of raw materials and finished products is a critical factor in ensuring production efficiency and product quality. A red sugar material handling system is a specialized solution designed to handle the unique characteristics of red sugar, including its granular structure, moisture content, and handling requirements. This system integrates various components such as conveyors, storage silos, and processing equipment to streamline the entire production process from raw material intake to final product packaging.
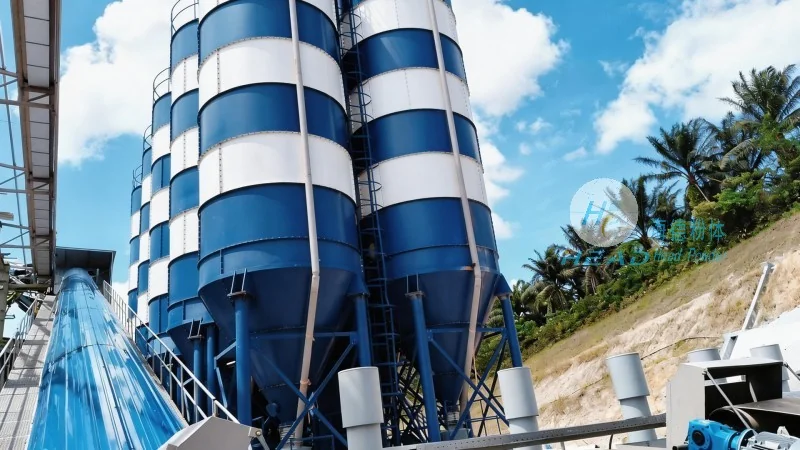
Understanding the Red Sugar Material Handling System
At the core of any red sugar material handling system is the ability to manage the flow of materials in a controlled and efficient manner. The system is typically composed of several key components that work in tandem to achieve optimal performance. These components include bulk material feeders, conveyor systems (such as belt conveyors or screw conveyors), storage silos, and processing units. Each component is carefully designed to handle the specific properties of red sugar, ensuring minimal product degradation and maximum operational efficiency.
Design Principles of the Red Sugar Material Handling System
The design of a red sugar material handling system follows several fundamental principles aimed at maximizing performance, safety, and longevity. First, the system must be constructed from materials that are resistant to corrosion and wear, as red sugar can be abrasive and may contain moisture that could lead to rust or material buildup. Common materials used include stainless steel and high-grade alloys, which provide durability and hygiene compliance. Second, the system is designed to minimize product contamination and cross-contamination risks. This is achieved through sealed conveyor systems, proper ventilation, and the use of sanitary design features that prevent the accumulation of dust or foreign particles. Third, the system is engineered for easy maintenance and cleaning, with components that can be easily disassembled and sanitized to meet food safety regulations. Finally, the system is optimized for energy efficiency, using variable speed drives and efficient motor systems to reduce operational costs while maintaining high performance.
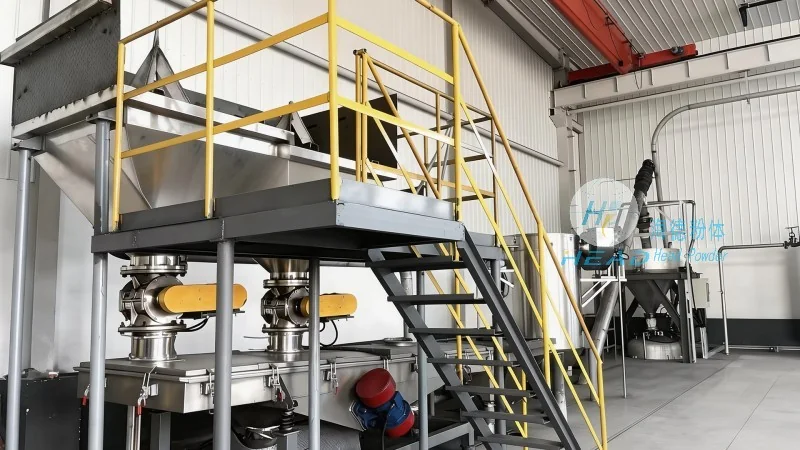
Key Components and Their Functions
Each component of the red sugar material handling system plays a crucial role in the overall operation. The bulk material feeder is responsible for uniformly feeding raw red sugar into the conveyor system, ensuring a consistent flow rate that prevents overloading or underloading of the conveyor. The conveyor system, often a belt conveyor or a screw conveyor, transports the sugar from the feeder to the storage silo or processing unit. The storage silo provides a large capacity for storing raw materials, allowing for continuous production even when raw material delivery is interrupted. The processing unit may include equipment such as classifiers, mixers, or packaging machines, which further refine the sugar and prepare it for final distribution.
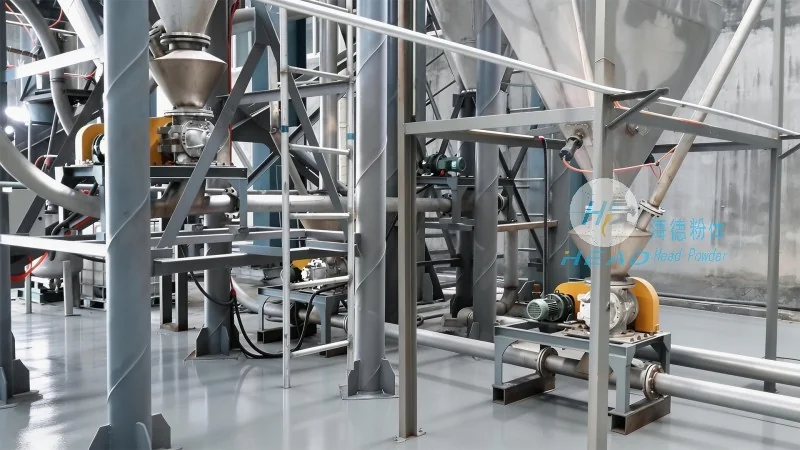
Benefits of an Efficient Red Sugar Material Handling System
Implementing a well-designed red sugar material handling system offers numerous benefits for sugar manufacturers. Firstly, it significantly improves production efficiency by reducing downtime and increasing the throughput of raw materials and finished products. The system's ability to handle large volumes of material in a continuous manner minimizes manual intervention and labor costs. Secondly, it enhances product quality by minimizing product degradation, contamination, and moisture loss during transportation. This ensures that the final red sugar product meets the highest quality standards and consumer expectations. Thirdly, the system improves workplace safety by reducing the need for manual handling of heavy or bulky materials, thereby minimizing the risk of workplace injuries. Finally, the system contributes to cost savings through energy efficiency and reduced maintenance requirements, making it a valuable investment for any sugar production facility.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of specialized material handling systems for the food and chemical industries. With a strong focus on innovation and customer satisfaction, HeadPowder has established itself as a trusted partner for companies seeking reliable and efficient solutions for their material handling needs. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with advanced technology and skilled engineering teams. HeadPowder's commitment to quality and customer service has earned it a reputation for delivering high-performance systems that meet the unique requirements of its clients. Whether for red sugar processing or other bulk material handling applications, HeadPowder provides tailored solutions that enhance operational efficiency and product quality.