

What is a Feather Powder Pneumatic Conveying System? And What Are Its Design Principles?
Feather powder pneumatic conveying systems represent a specialized and efficient method for transporting fine powders, particularly those with delicate characteristics like feather powders. These systems leverage the principles of pneumatic transport to move materials through a closed pipeline using compressed air or other gas streams. Understanding the design principles behind such systems is crucial for optimizing performance, ensuring material integrity, and maintaining operational efficiency.
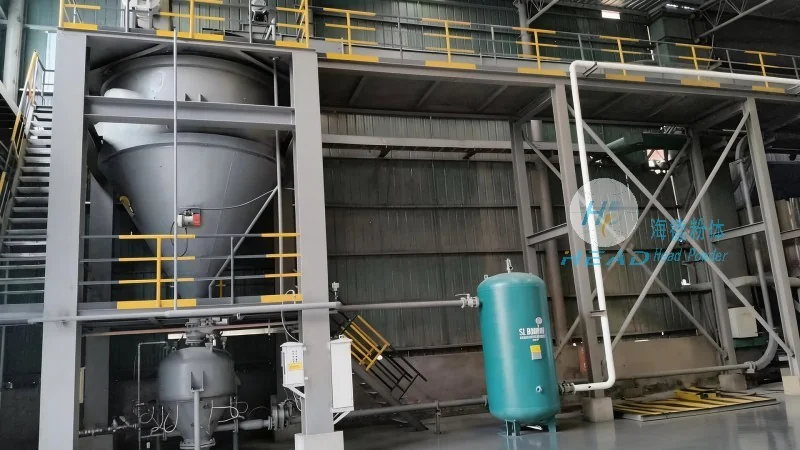
Core Components of a Feather Powder Pneumatic Conveying System
At the heart of a feather powder pneumatic conveying system are several key components that work in tandem to facilitate material transport. The primary components typically include a material feeder, a conveying line (often equipped with pressure vessels or vacuum units), a control system, and a discharge unit. The material feeder is designed to handle the delicate nature of feather powders, ensuring consistent and controlled feeding to prevent agglomeration or damage to the powder particles. The conveying line, which may be pressure or vacuum-based, is constructed from materials that are compatible with the powder's properties, such as stainless steel or specialized coatings to avoid contamination or particle degradation. The control system monitors and regulates the air flow, pressure, and material flow rates, ensuring stable operation and preventing system overloads. Finally, the discharge unit safely releases the powder at the destination, often with features to minimize dust and maintain material quality.
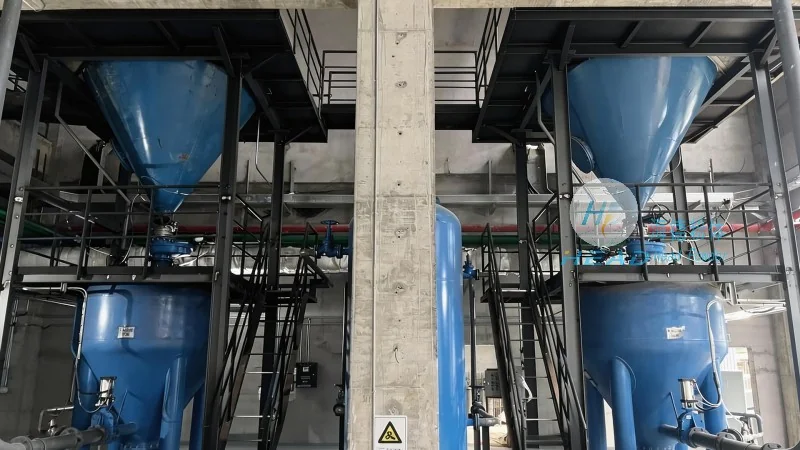
Design Principles for Optimal Performance
The design of a feather powder pneumatic conveying system is guided by several critical principles aimed at maximizing efficiency and preserving the quality of the powder. First, the system must be designed to handle the specific physical and chemical properties of feather powders, including their particle size, density, and moisture content. This involves selecting appropriate air velocities and pressure levels to prevent particle degradation or caking. Second, the system's design must prioritize material integrity, ensuring that the powder remains in its original state throughout the conveying process. This includes minimizing particle attrition, avoiding exposure to harsh environments, and controlling temperature fluctuations. Third, the system should be optimized for energy efficiency, as pneumatic conveying can be energy-intensive. This is achieved through careful selection of air flow rates, pipeline diameters, and pressure differentials, as well as the use of efficient compressors and control mechanisms. Fourth, the design must incorporate safety features to protect both personnel and equipment, such as pressure relief valves, dust collection systems, and proper ventilation. Finally, the system's scalability and adaptability are important considerations, allowing for future expansion or integration with other processing equipment.
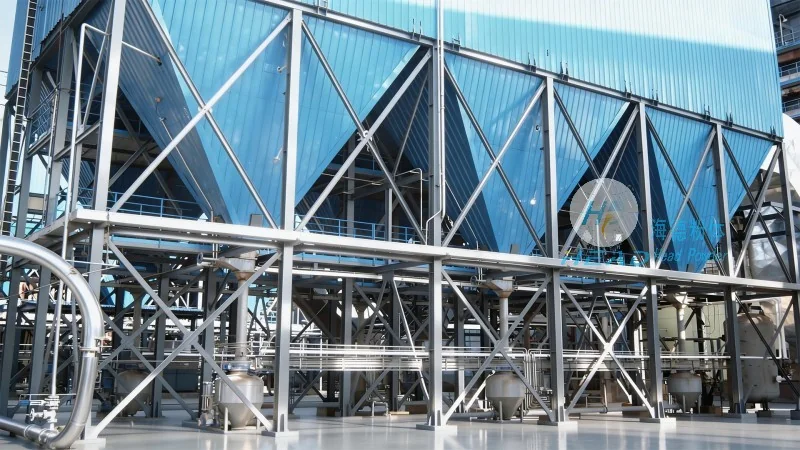
Application and Operational Considerations
Feather powder pneumatic conveying systems are widely used in various industries, including food processing, pharmaceuticals, and chemical manufacturing, where the delicate nature of the powder requires gentle handling. The operational considerations for these systems include maintaining consistent air pressure and flow rates to avoid system surges or drops in material transport. Regular maintenance is also essential to ensure the system operates at peak efficiency, including cleaning of the conveying line, inspection of components for wear and tear, and calibration of the control system. Additionally, the system's design must account for the potential for dust accumulation, as feather powders can be fine and easily suspended in the air. Proper dust collection and filtration systems are therefore critical to maintaining a safe and clean working environment.
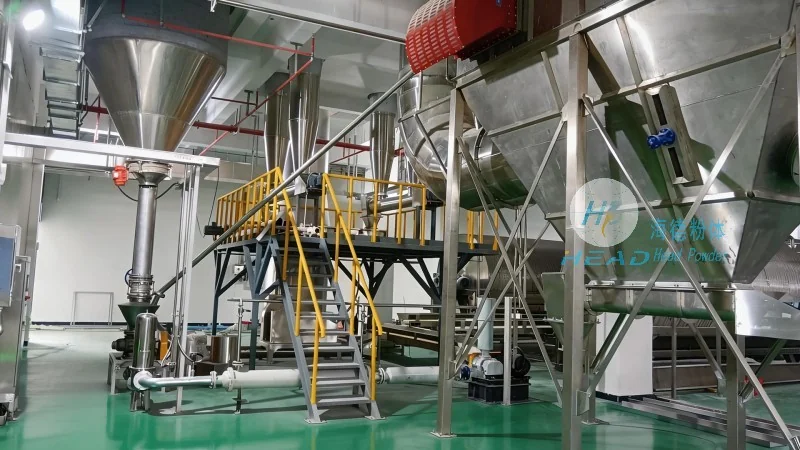
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of specialized pneumatic conveying systems, including those designed for feather powders. With a focus on innovation and quality, the company has developed advanced solutions that meet the unique challenges of transporting delicate powders. HeadPowder's systems are engineered to provide reliable, efficient, and safe operation, ensuring that clients can achieve their production goals while maintaining the highest standards of material quality. The company's expertise in material handling and pneumatic transport technology, combined with its commitment to customer satisfaction, makes it a trusted partner for businesses in need of reliable conveying solutions. HeadPowder operates from China, providing comprehensive support and service to clients worldwide.