

What is an Eco-friendly Powder Pneumatic Conveying Equipment? What Are Its Design Principles?
Understanding the role of eco-friendly powder pneumatic conveying equipment is crucial for industries dealing with bulk solid materials. This equipment efficiently transports powders and granules through a pressurized or vacuum system, offering a sustainable alternative to traditional methods like belt conveyors or bucket elevators. The design of such equipment focuses on minimizing environmental impact while ensuring high efficiency and reliability in material handling processes.
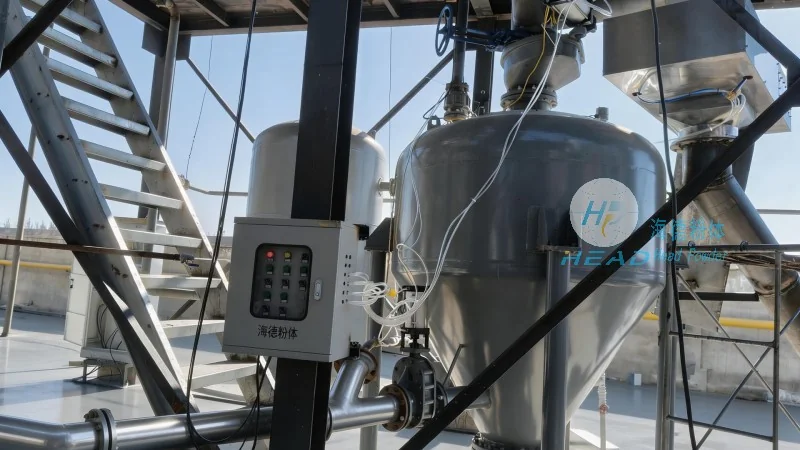
About HeadPowder: A Leader in Sustainable Material Handling Solutions
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a prominent manufacturer based in Shandong, China. The company specializes in developing advanced pneumatic conveying systems tailored to meet the evolving needs of various industries, including food, pharmaceuticals, chemicals, and minerals. HeadPowder's commitment to sustainability is reflected in the design and operation of their equipment, which adheres to stringent environmental standards and promotes energy efficiency.
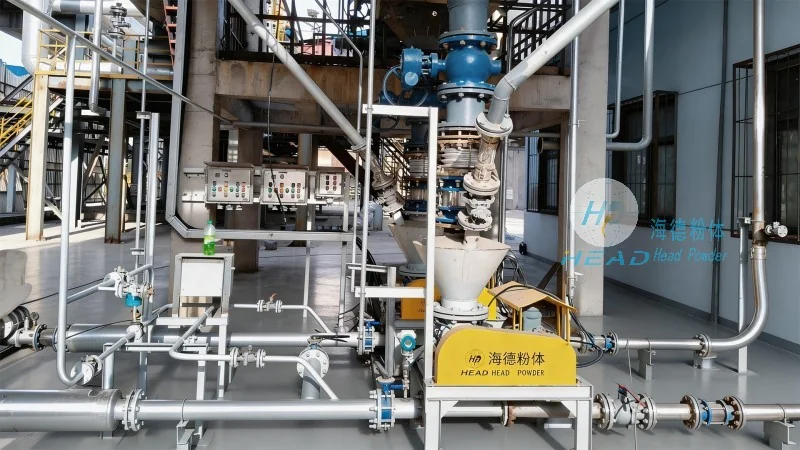
Design Principles of Eco-friendly Powder Pneumatic Conveying Equipment
The core design principles of eco-friendly powder pneumatic conveying equipment revolve around optimizing material flow, reducing energy consumption, and minimizing emissions. One key principle is the use of efficient air compression and filtration systems. These systems ensure that the conveying air is clean and free from dust, preventing contamination of the transported materials and protecting the environment. Additionally, the equipment incorporates energy-saving components, such as variable frequency drives (VFDs), which adjust the air flow rate based on the material demand, thus reducing unnecessary energy use.
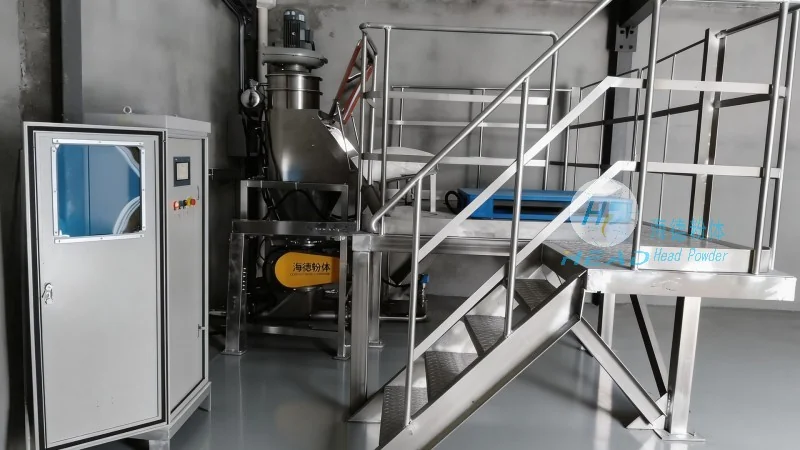
Key Components and Their Functions in the Equipment
The eco-friendly powder pneumatic conveying equipment consists of several critical components, each playing a vital role in the overall operation. The primary components include the air compressor, which generates the necessary pressure or vacuum to move the powder; the hopper or feed hopper, which stores and feeds the material into the system; the pipeline system, which transports the material from the source to the destination; and the receiver or discharge hopper, which collects the material at the end of the conveying line. The filtration system is another essential component, designed to capture any fine particles and return clean air back to the compressor, thus maintaining air quality and preventing environmental pollution.
Advantages of Using Eco-friendly Powder Pneumatic Conveying Equipment
Implementing eco-friendly powder pneumatic conveying equipment offers numerous benefits for businesses. Firstly, it significantly reduces the risk of dust explosions and contamination, which are common issues with traditional bulk material handling methods. Secondly, the equipment enhances process efficiency by providing a continuous and reliable flow of materials, minimizing downtime and improving overall productivity. Thirdly, the design focuses on energy efficiency, leading to lower operational costs and reduced carbon footprint. Moreover, the equipment is versatile and can handle a wide range of materials, from fine powders to coarse granules, making it suitable for various industrial applications.
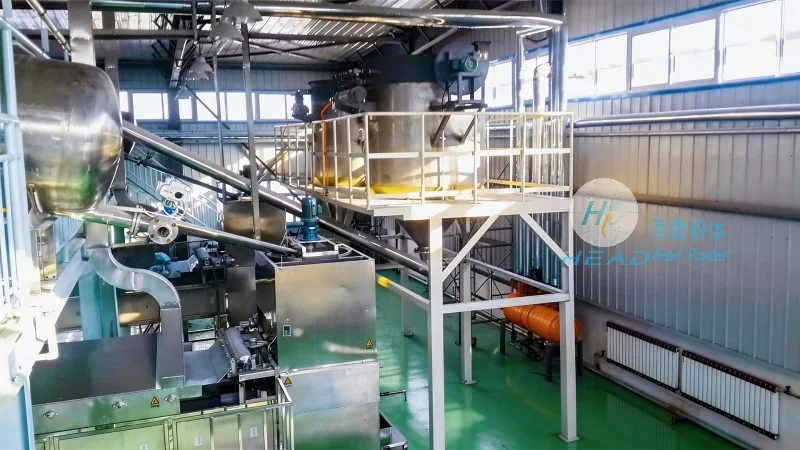
Application Scenarios and Industry Impact
Eco-friendly powder pneumatic conveying equipment is widely used in industries where the handling of powders and granules is essential. In the food industry, for example, such equipment is used to transport ingredients like flour, sugar, and spices, ensuring food safety and quality. In the pharmaceutical sector, the equipment is employed to convey active pharmaceutical ingredients (APIs) and excipients, maintaining the purity and integrity of the materials. The chemical industry also benefits from this technology, as it efficiently handles hazardous powders while minimizing environmental exposure. Overall, the adoption of eco-friendly pneumatic conveying systems contributes to a more sustainable and efficient industrial landscape.