

Working Principle and Features of Dust-Free Bag Opening Material Conveying Systems
Efficient and clean material handling is a critical requirement in modern industrial processes, particularly in sectors such as pharmaceuticals, food processing, and electronics manufacturing. The dust-free bag opening material conveying system, developed by Shandong HeadPowder Engineering Co., Ltd. based in China, represents a sophisticated solution designed to meet stringent cleanliness standards while ensuring seamless material transfer. This article explores the working principles and key features of this advanced system, highlighting how it addresses the challenges of maintaining a contamination-free environment during material handling operations.
Understanding the Working Principle of Dust-Free Bag Opening Material Conveying
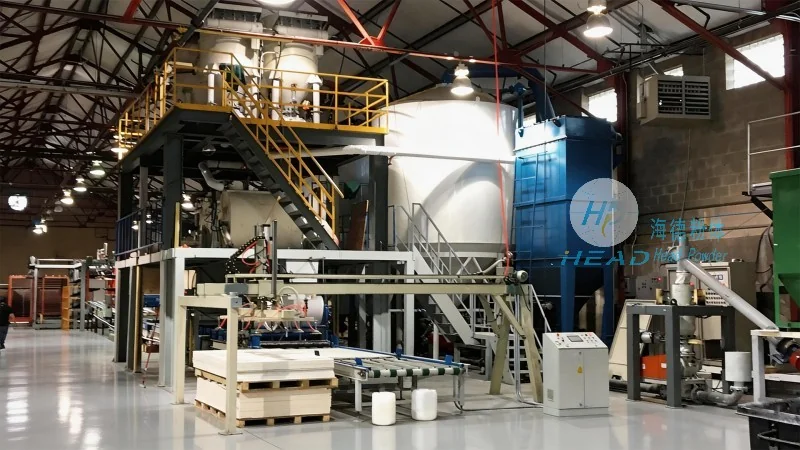
The core of the dust-free bag opening material conveying system lies in its integrated approach to bag opening, material extraction, and subsequent transport. The process begins with the placement of sealed bags onto a designated loading platform. Advanced mechanical or pneumatic mechanisms then facilitate the controlled opening of the bags without generating dust or particulate matter. This is typically achieved through specialized cutting or tearing tools that are designed to minimize particle dispersion. Once the bag is opened, the internal material is transferred into a hopper or collection chamber. From there, a series of conveyor belts or pneumatic transport systems move the material to the next processing stage. The entire operation is enclosed within a sealed housing, often equipped with HEPA filters or other air filtration systems to maintain an ultra-clean environment. The system’s control panel allows for precise regulation of speed, pressure, and other parameters to ensure consistent performance and prevent material loss or contamination.
Key Features of the Dust-Free Bag Opening Material Conveying System
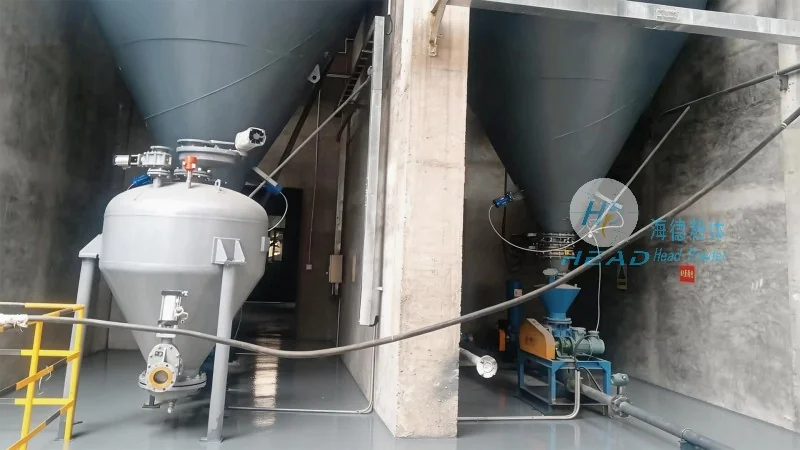
Shandong HeadPowder Engineering Co., Ltd. has incorporated several notable features into their dust-free bag opening material conveying system to enhance functionality and reliability. One of the primary features is the use of stainless steel and other corrosion-resistant materials for the internal components, which not only ensures durability but also facilitates easy cleaning and maintenance. The system is equipped with automatic bag detection sensors that can identify the presence of bags and initiate the opening process, reducing manual intervention and improving operational efficiency. Additionally, the design includes a dust collection and filtration system that captures any particles generated during the bag opening process, ensuring that the air within the enclosure remains clean and compliant with regulatory standards. The conveyor system is designed to handle a wide range of material types, including powders, granules, and bulk solids, with adjustable feed rates to accommodate varying material properties. Another important feature is the integration of safety mechanisms, such as emergency stop buttons and interlocked access panels, to protect operators and prevent accidents. The system also offers customizable options, allowing clients to tailor the equipment to their specific production needs, including different bag sizes, material capacities, and output speeds.
Benefits and Applications of the Dust-Free Bag Opening Material Conveying System
The implementation of a dust-free bag opening material conveying system offers numerous benefits to industrial operations. By maintaining a contamination-free environment, it helps to preserve the quality and integrity of sensitive materials, which is particularly crucial in industries like pharmaceuticals where product purity is paramount. The system’s high efficiency in material transfer reduces processing time and labor costs, leading to increased productivity. Furthermore, the enclosed design minimizes the risk of dust exposure to personnel, improving workplace safety and compliance with occupational health regulations. The system is widely applicable in various industries, including pharmaceutical manufacturing, food processing, chemical production, and electronics assembly. In pharmaceutical facilities, it is used to handle raw materials and intermediates, ensuring that the final products meet stringent quality standards. In food processing plants, it helps to maintain hygiene standards while efficiently transferring ingredients. The system’s versatility also makes it suitable for use in research and development laboratories, where precise material handling is required for experimental work. Overall, the dust-free bag opening material conveying system provides a reliable and efficient solution for industries that demand high levels of cleanliness and material integrity in their production processes.
Conclusion and Company Overview
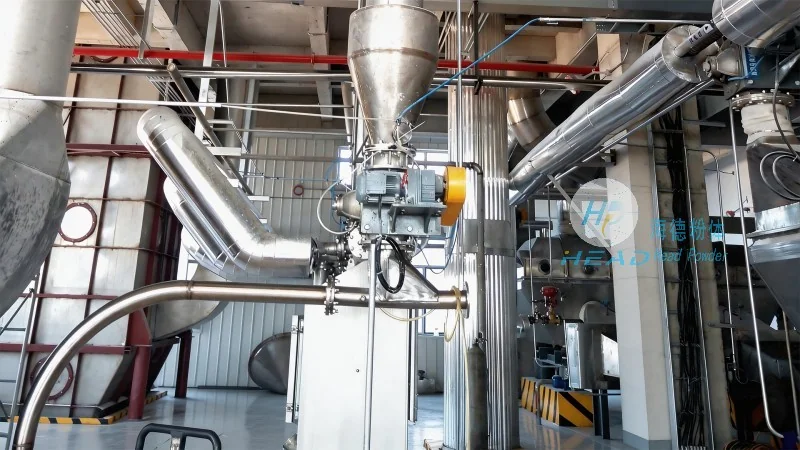
Shandong HeadPowder Engineering Co., Ltd., based in China, has developed a state-of-the-art dust-free bag opening material conveying system that combines advanced technology with robust design to meet the demanding requirements of modern industrial applications. The system’s working principle, which involves enclosed bag opening and material transport, ensures minimal dust generation and maintains a clean environment. Key features such as stainless steel construction, automatic bag detection, and integrated filtration systems enhance its performance and reliability. The benefits of this system, including improved product quality, increased efficiency, and enhanced safety, make it an essential component for industries that prioritize cleanliness and material integrity. As a leading manufacturer in the field, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and provide customized solutions to meet the evolving needs of its clients, ensuring that their material handling processes remain efficient, safe, and compliant with industry standards.