

Working Principle and Features of Cement Fly Ash Material Handling Systems
For industrial applications involving the transport of cement and fly ash, efficient material handling systems are crucial for maintaining production efficiency and operational safety. The cement fly ash material handling system, developed by Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, is engineered to address the specific challenges of handling these materials, which are commonly used in construction and manufacturing processes.

Overview of the Cement Fly Ash Material Handling System
The system is designed to facilitate the seamless transfer of cement and fly ash from storage silos or processing units to various points of use, such as mixing plants, storage facilities, or processing lines. It integrates components like conveyors, feeders, and control systems to ensure reliable and continuous material flow. The design emphasizes durability, low maintenance, and adaptability to varying material characteristics and operational conditions.
Working Principle of the Material Handling System
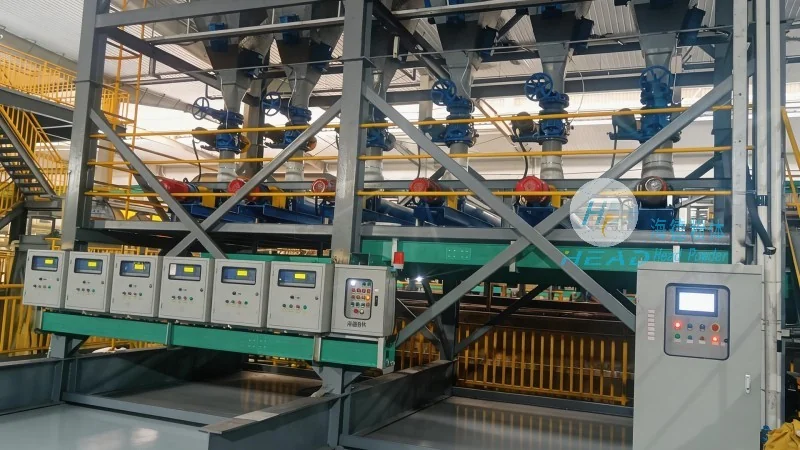
The core working principle of the cement fly ash material handling system involves the use of mechanical conveying equipment to transport bulk materials. The process typically starts with material being discharged from a storage silo or hopper. A feeder, often a rotary or vibratory type, regulates the flow rate of the material into the conveyor system. The conveyor, which may be a belt conveyor, screw conveyor, or pneumatic conveyor depending on the specific application, then transports the material to the desired destination. Control systems monitor and adjust the flow rate, ensuring consistent performance and preventing overloading or underflow. The entire operation is automated, with sensors and controls maintaining optimal conditions for material handling.
Key Features and Advantages
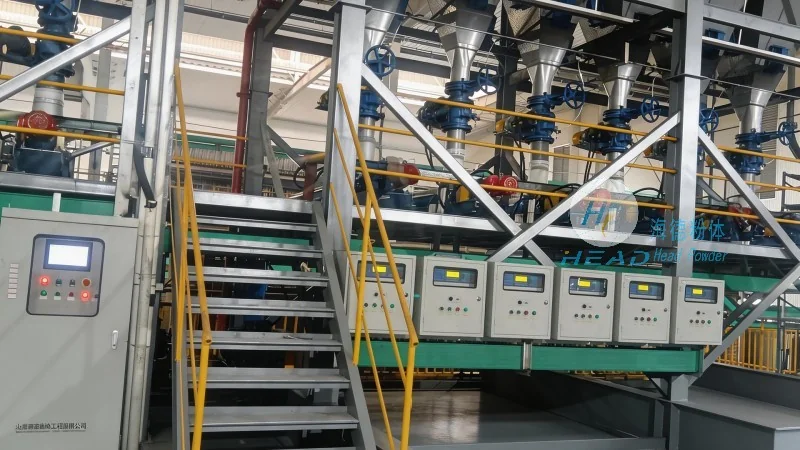
One of the primary features of the cement fly ash material handling system is its ability to handle abrasive and fine materials like cement and fly ash without excessive wear or blockages. The system incorporates wear-resistant components, such as lined hoppers and conveyor belts, to extend the service life of the equipment. Additionally, the design allows for easy integration with existing production lines, reducing installation time and costs. The system also offers high capacity and low energy consumption, contributing to operational efficiency and cost savings. Another notable feature is the robust control system, which provides real-time monitoring and adjustment of parameters, ensuring safe and reliable operation. The system is also designed for easy maintenance, with accessible components and modular design that simplifies repairs and replacements.
Application and Operational Benefits
The cement fly ash material handling system is widely used in cement plants, power stations, and construction material manufacturing facilities. Its ability to handle large volumes of material efficiently supports high production rates and reduces downtime. The system's reliability minimizes the risk of material loss or contamination, which is critical for maintaining product quality. Furthermore, the system's low maintenance requirements and energy efficiency make it a cost-effective solution for long-term operation. By streamlining the material transport process, the system enhances overall operational efficiency and contributes to improved productivity in industrial settings.