

Working Principle and Features of Mung Bean Material Handling System Equipment
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in providing advanced solutions for material handling in agricultural processing. The company’s expertise lies in developing efficient and reliable equipment tailored to the specific needs of industries dealing with mung beans and other similar agricultural products. This article explores the working principle and key features of the mung bean material handling system equipment, highlighting how it enhances operational efficiency and product quality.
Company Overview and Expertise
HeadPowder, as the company is commonly known, is headquartered in Shandong, China. With years of experience in the engineering and manufacturing sector, the company has built a strong reputation for delivering high-quality machinery that meets international standards. The team at HeadPowder comprises skilled engineers and technicians who are dedicated to innovation and customer satisfaction. Their commitment to using advanced technology and robust materials ensures that each piece of equipment is built to last and perform optimally under demanding conditions.
Understanding the Mung Bean Material Handling System
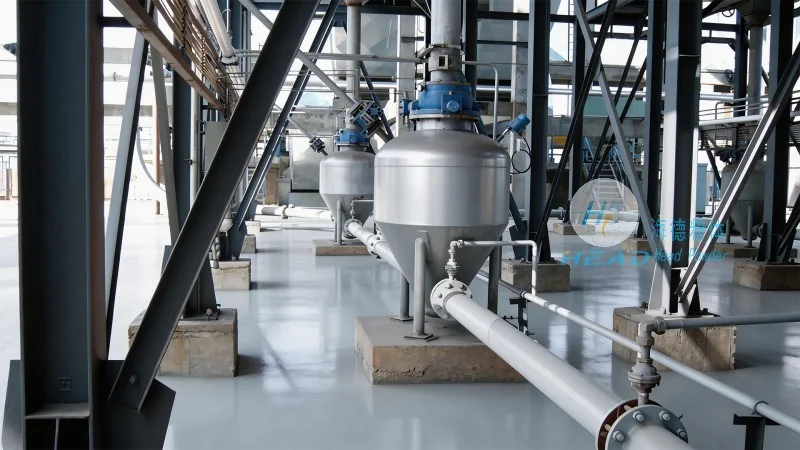
The mung bean material handling system is a comprehensive solution designed to streamline the entire process of handling, transporting, and processing mung beans from raw material reception to final product packaging. This system integrates various components such as conveyors, elevators, classifiers, and storage units, all working in harmony to ensure smooth and continuous operation. The equipment is engineered to handle the unique characteristics of mung beans, including their size, shape, and moisture content, while maintaining the integrity of the product.
Working Principle of the Material Handling System
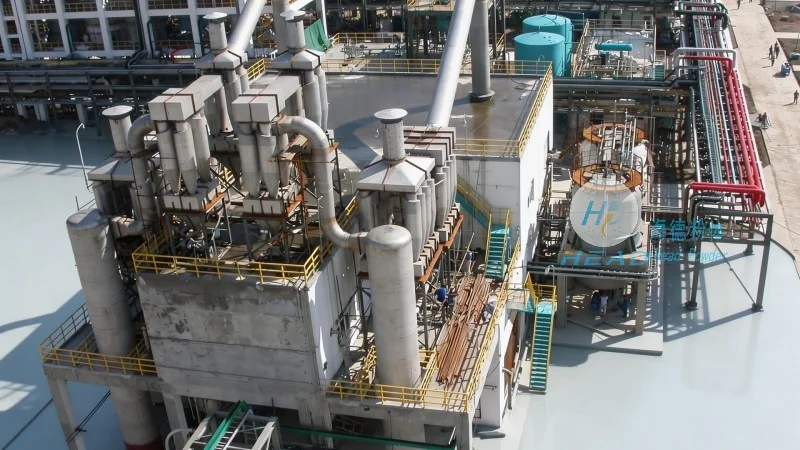
The core of the mung bean material handling system is its automated workflow, which is designed to minimize manual intervention and maximize productivity. The process typically begins with the reception of raw mung beans, which are then fed into a hopper or storage silo. From there, the beans are transferred to a series of conveyors that move them through different stages of processing. The system may include a combination of belt conveyors, screw conveyors, and bucket elevators, each chosen based on the specific requirements of the operation. For example, belt conveyors are ideal for transporting large quantities of beans over short to medium distances, while screw conveyors are effective for vertical or inclined movement with minimal spillage. Bucket elevators are used to lift the beans to higher levels, ensuring efficient vertical transport without compromising product quality.
During the transport process, the system may incorporate screening or sorting mechanisms to remove impurities such as stones, dust, or foreign materials. These classifiers use vibrating screens or air classifiers to separate the good beans from the contaminants, ensuring that only high-quality mung beans proceed to the next stage. The system is equipped with sensors and control panels that monitor the flow rate, temperature, and other critical parameters, allowing for real-time adjustments to maintain optimal performance. This automation not only improves efficiency but also reduces the risk of human error and product contamination.
Key Features and Advantages
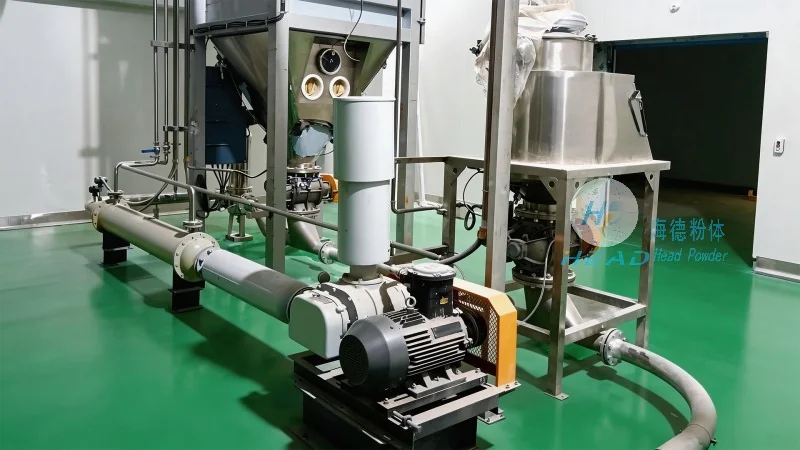
The mung bean material handling system from HeadPowder is characterized by several key features that set it apart from conventional solutions. One of the most notable advantages is its high efficiency, which is achieved through the integration of multiple components and automated controls. The system can handle large volumes of mung beans at a consistent rate, reducing processing time and increasing overall throughput. This efficiency is particularly beneficial for large-scale operations where speed and productivity are critical.
Another important feature is the system's durability and reliability. Constructed from high-quality materials such as stainless steel and heavy-duty plastics, the equipment is designed to withstand the rigors of continuous operation in agricultural processing environments. The components are built to last, minimizing the need for frequent maintenance and repairs, which in turn reduces downtime and operational costs. This durability ensures that the system provides long-term value to the user.
The system also emphasizes energy efficiency, incorporating features such as variable speed drives and optimized conveyor designs to reduce energy consumption. By minimizing energy use, the equipment helps businesses lower their operational costs while contributing to environmental sustainability. Additionally, the system is designed with easy maintenance in mind, featuring accessible components and clear operational indicators that allow for quick troubleshooting and repairs.

Furthermore, the mung bean material handling system is highly customizable to meet the specific needs of different clients. HeadPowder offers tailored solutions that can be adjusted in terms of capacity, speed, and integration with existing processing lines. This flexibility allows businesses to adapt the system to their unique production requirements, ensuring optimal performance and cost-effectiveness.
Conclusion
In conclusion, the mung bean material handling system from Shandong HeadPowder Engineering Co., Ltd. represents a sophisticated and efficient solution for the processing of mung beans. By combining advanced automation, robust construction, and customizable features, the system enhances operational efficiency, product quality, and cost-effectiveness for businesses in the agricultural sector. With its headquarters in Shandong, China, HeadPowder continues to lead the industry in providing reliable and innovative material handling equipment that meets the evolving needs of modern agricultural processing.