

Working Principle and Features of Vacuum Suction Material Pneumatic Conveying Equipment
When it comes to efficient material handling in industrial settings, vacuum suction pneumatic conveying equipment stands out as a reliable and versatile solution. This technology is widely used for transporting dry bulk materials such as powders, granules, and fine particles over short to medium distances. Understanding the working principle and key features of this equipment is crucial for selecting the right system for specific applications. This article delves into the fundamental aspects of vacuum suction material pneumatic conveying, highlighting how it operates and what makes it an attractive choice for various industries.
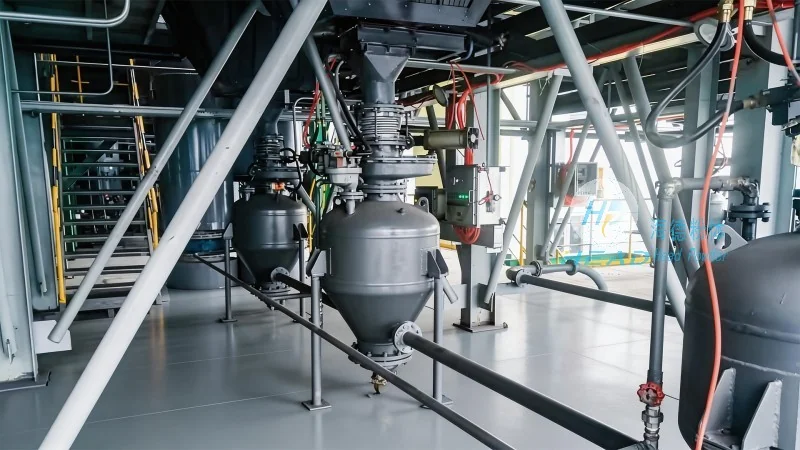
Key Working Principle of the Vacuum Suction Conveying System
The core of a vacuum suction pneumatic conveying system lies in its ability to create a negative pressure environment. A vacuum pump or a series of fans is used to generate a pressure differential between the material source and the receiving container. By pulling air and the material particles through a pipeline, the system effectively transports the material from the source to the destination. The process typically involves several key components, including a vacuum source, a material feed hopper, a conveying line, and a receiving vessel. The vacuum pump draws air from the receiving end of the pipeline, creating a suction force that pulls the material particles along with the air stream. As the material is drawn into the pipeline, it is suspended in the air and transported to the collection point. The system ensures that the material is conveyed without direct contact with the conveying line, minimizing wear and tear and preventing contamination.
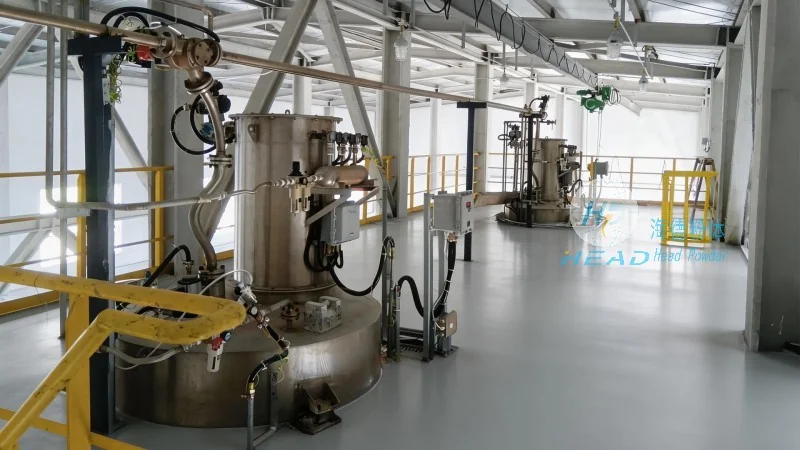
Main Features and Advantages of Vacuum Suction Pneumatic Conveying Equipment
One of the primary advantages of vacuum suction material pneumatic conveying is its ability to handle a wide range of materials, from fine powders to larger granules. The system is particularly effective for materials that are prone to dust generation or require gentle handling to avoid degradation. The vacuum operation also helps in maintaining a clean and controlled environment, as the material is contained within the pipeline and not exposed to the ambient air. Additionally, this type of conveying system is relatively compact and can be easily integrated into existing industrial setups. The low noise operation and minimal maintenance requirements make it a cost-effective solution for many applications. Another key feature is the flexibility in system design, allowing for multiple material sources and destinations to be connected through a network of pipelines. This makes it suitable for complex material handling scenarios where materials need to be transferred from various locations to a central processing unit.
Applications and Industries Benefiting from Vacuum Suction Conveying
Vacuum suction pneumatic conveying equipment is widely adopted across various industries due to its adaptability and efficiency. In the pharmaceutical and food processing sectors, the system is used to transport sensitive materials that require sterile and hygienic handling. The gentle conveying action prevents product degradation and maintains product quality. In the chemical industry, it is used for handling powders and granules that may be hazardous or reactive. The vacuum operation ensures that no material is released into the environment, enhancing safety and compliance with environmental regulations. The construction and mining industries also benefit from this technology for transporting bulk materials such as sand, gravel, and cement over short distances. The system's ability to handle abrasive materials without significant wear on the equipment makes it a durable and long-lasting solution. Furthermore, in the agricultural sector, vacuum suction conveying is used for transporting grains and other agricultural products, ensuring efficient and clean handling from storage to processing facilities.
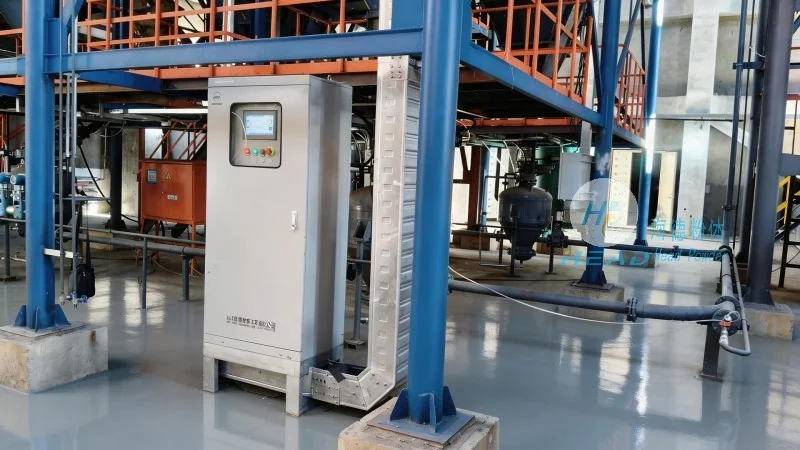
Conclusion and Company Overview
Overall, vacuum suction material pneumatic conveying equipment offers a robust and efficient solution for material handling needs. Its working principle, based on creating a negative pressure environment, enables the reliable transport of various dry bulk materials. The key features, including flexibility, low maintenance, and gentle handling, make it an attractive option for diverse industrial applications. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality vacuum suction pneumatic conveying systems tailored to meet the specific requirements of different industries. With a focus on innovation and customer satisfaction, HeadPowder ensures that their equipment delivers optimal performance and longevity, contributing to the efficiency and productivity of industrial operations. The company's commitment to quality and technical expertise makes it a trusted partner for businesses seeking reliable material handling solutions.