

Principle and Working Scene Characteristics of Calcium Nitrite Powder Handling Equipment
Calcium nitrite is a critical chemical compound widely used in various industrial applications, including concrete admixtures, water treatment, and as a corrosion inhibitor. The efficient handling and transportation of calcium nitrite powder are essential for maintaining product quality and operational efficiency in industrial settings. This article explores the principle and working characteristics of specialized equipment designed for calcium nitrite powder handling, focusing on its operational mechanisms and typical application scenarios.
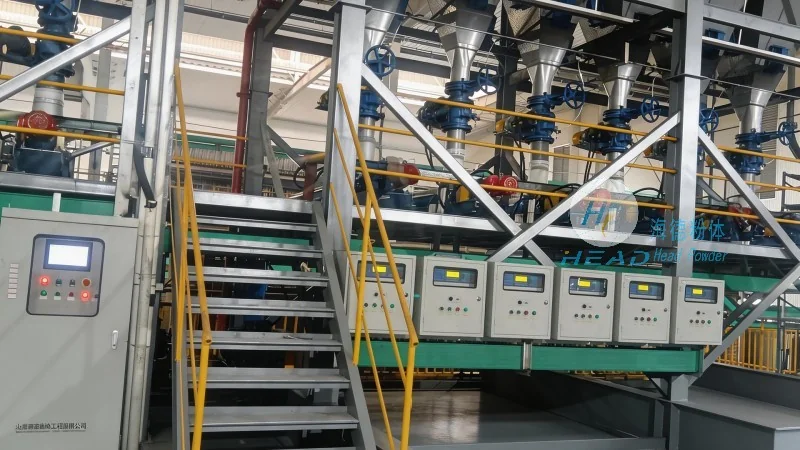
Overview of Calcium Nitrite Powder Handling Equipment
The calcium nitrite powder handling equipment, developed by Shandong HeadPowder Engineering Co., Ltd., is engineered to address the unique challenges associated with transporting and storing this reactive chemical. The system integrates advanced pneumatic conveying technology, ensuring precise control over powder flow, pressure, and temperature to prevent degradation or caking of the material. Key components include a hopper for material storage, a rotary valve for controlled discharge, and a pipeline system equipped with pressure regulators and filters to maintain consistent performance.
Working Principle of the Powder Handling System
The core principle of the calcium nitrite powder handling equipment is pneumatic conveying, where air is used as the medium to transport the powder through a closed pipeline system. The process begins with the material being fed into the hopper, where it is held under controlled conditions to prevent moisture absorption or agglomeration. A rotary valve then regulates the flow of powder into the conveying line, ensuring a steady and uniform feed rate. Compressed air, supplied by an air compressor, is introduced into the pipeline, creating a pressure differential that propels the powder particles forward. The system employs a combination of positive and negative pressure zones to optimize the conveying efficiency, minimizing energy consumption while maintaining high throughput rates. The use of specialized filters and moisture-proofing measures within the pipeline helps maintain the purity and stability of the calcium nitrite powder throughout the transport process.
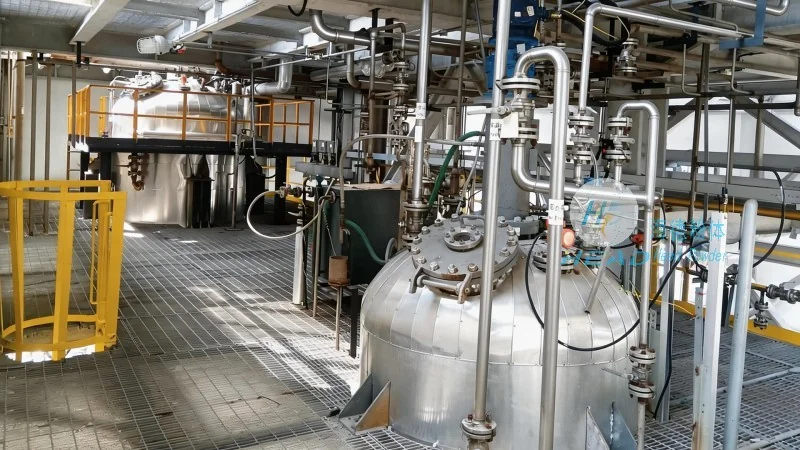
Key Working Scene Characteristics
The calcium nitrite powder handling equipment is designed for versatility and adaptability across different industrial environments. It is particularly suitable for applications requiring the safe and efficient transfer of calcium nitrite from storage silos to processing units, or between production lines. The equipment's compact design and modular construction allow for easy integration into existing facilities, reducing installation time and costs. In addition, the system's ability to handle varying powder flow rates and pressure conditions makes it suitable for both continuous and batch processing operations. The operational characteristics also include low maintenance requirements, with self-cleaning features in the hopper and pipeline to prevent material buildup, and advanced monitoring systems that provide real-time feedback on pressure, flow, and temperature parameters, ensuring optimal performance and safety.
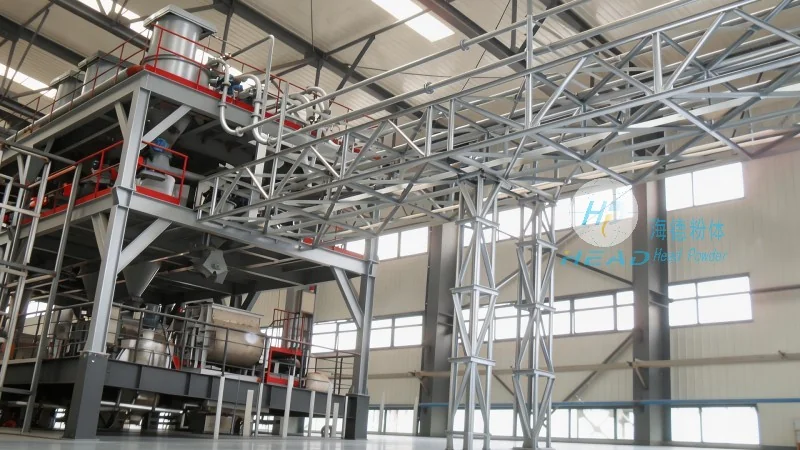
Application Scenarios and Operational Benefits
The calcium nitrite powder handling equipment is widely used in concrete production facilities, where calcium nitrite is added as an admixture to enhance the durability and corrosion resistance of concrete structures. The system's ability to deliver precise dosages of the powder ensures consistent quality in the final product, meeting stringent industry standards. In water treatment plants, the equipment facilitates the controlled addition of calcium nitrite to water treatment processes, improving the effectiveness of corrosion control and water purification. Additionally, in industrial manufacturing settings, the equipment supports the seamless transfer of calcium nitrite between different stages of production, such as from storage to mixing or from mixing to packaging. The operational benefits of this equipment include improved safety due to enclosed handling systems, reduced material waste through precise control, and enhanced productivity through automated operation. The system's reliability and durability, coupled with its low operational costs, make it a preferred choice for industries that require consistent and high-quality powder handling solutions.
Conclusion and Company Information
Shandong HeadPowder Engineering Co., Ltd. specializes in the design and manufacturing of advanced powder handling equipment tailored to the specific needs of chemical and industrial applications. The calcium nitrite powder handling equipment exemplifies the company's commitment to innovation and quality, providing reliable and efficient solutions for the transportation and storage of critical chemical powders. With its headquarters in Shandong, China, HeadPowder leverages years of industry experience to deliver customized equipment that meets the unique requirements of each client. The company's focus on customer satisfaction and product performance ensures that its equipment continues to be a trusted solution for industries relying on calcium nitrite and other sensitive chemical powders.