

[Principle and Working Scene Characteristics of Automatic Weighing and Material Conveying System Equ
HeadPowder, a leading provider in the field, specializes in advanced equipment designed for precise material handling and processing. This article delves into the core principles and operational scenarios of their automatic weighing and material conveying systems, highlighting how these technologies enhance efficiency and accuracy in various industrial applications.
Company Overview
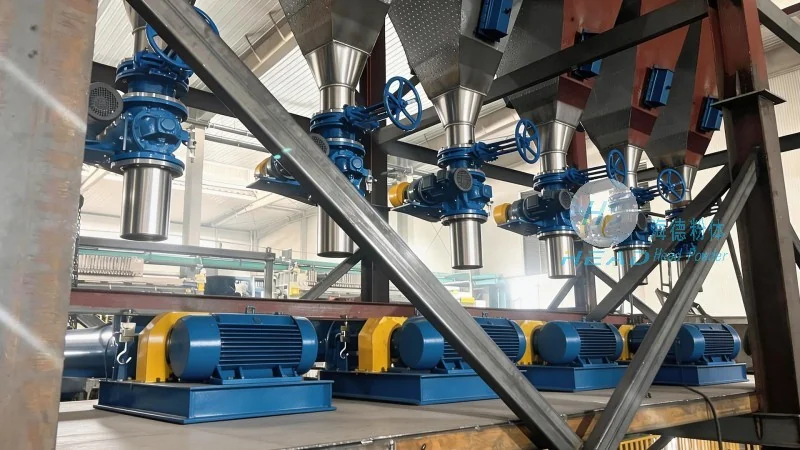
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China. The company has established itself as a trusted name in engineering solutions, focusing on the development and manufacturing of high-quality equipment tailored to meet the demands of modern industrial sectors. With a commitment to innovation and precision, HeadPowder delivers systems that optimize material flow and weighing processes, ensuring reliability and performance in diverse operational environments.
Core Principles of the Automatic Weighing System
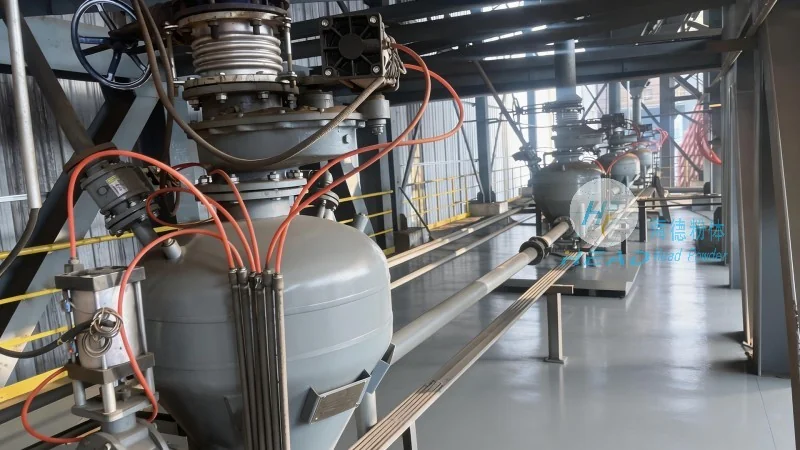
The automatic weighing system at the heart of the material conveying equipment operates on a sophisticated principle of precision measurement and control. Utilizing advanced sensors and digital control technologies, the system ensures accurate weight measurement for each batch of material. The process begins with the material being fed into the weighing hopper, where it is evenly distributed to achieve consistent weight readings. The system then processes these readings, comparing them against pre-set targets to determine the exact amount of material required. This precision is crucial for applications where exact proportions are essential, such as in chemical manufacturing, food processing, and pharmaceutical production. The integration of real-time data processing allows for immediate adjustments, minimizing errors and enhancing overall operational efficiency.
Material Conveying Mechanisms
Complementing the weighing system, the material conveying component plays a vital role in the seamless transport of materials from one stage to another. The equipment employs a combination of conveyor belts, screw conveyors, and pneumatic systems, depending on the material characteristics and processing requirements. For bulk materials, screw conveyors provide reliable vertical and horizontal transport, ensuring smooth movement without material degradation. Conveyor belts are ideal for handling lighter or more delicate materials, offering gentle transport that preserves product integrity. Pneumatic conveying systems are utilized for fine powders and granules, enabling efficient and dust-free transport over longer distances. Each conveying method is carefully selected based on the material's density, flowability, and the specific workflow of the production line, ensuring optimal performance and minimal downtime.
Working Scene Characteristics
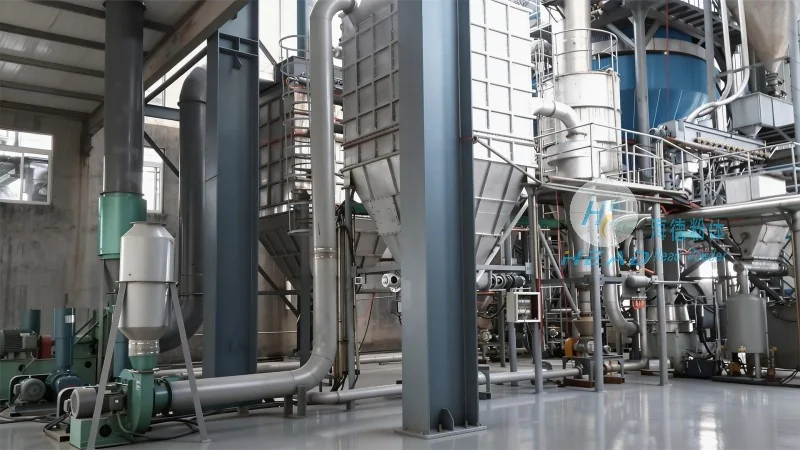
The operational scenarios of these systems are diverse and tailored to meet the unique needs of different industries. In chemical plants, the automatic weighing and conveying systems are integral to the production of fertilizers, pesticides, and other chemical compounds, where precise ingredient ratios are critical for product quality and safety. In the food industry, these systems are employed in the processing of cereals, snacks, and beverages, ensuring consistent flavor profiles and nutritional content. The pharmaceutical sector also benefits significantly, as the systems enable the accurate dispensing of active ingredients and excipients, adhering to stringent regulatory standards. Additionally, in the mining and mineral processing industries, the equipment is used for the handling and weighing of raw ores and concentrates, optimizing the extraction and processing of valuable minerals. Each working scene is characterized by high throughput, consistent accuracy, and the ability to handle a wide range of materials, making the systems versatile and adaptable to various production environments.