

Operation Process and Working Principle of Quartz Stone Pneumatic Conveying Machine
Quartz stone is a widely used material in various industrial applications, and the efficient transportation of this material is crucial for production efficiency. The quartz stone pneumatic conveying machine, developed by Shandong HeadPowder Engineering Co., Ltd. (headpowder), offers a reliable solution for handling quartz stone with precision and minimal maintenance. This equipment is designed to meet the demands of modern industrial processes, ensuring smooth material transfer while maintaining product integrity. The company, based in Shandong, China, specializes in engineering and manufacturing advanced material handling solutions, including pneumatic conveying systems for diverse bulk materials.
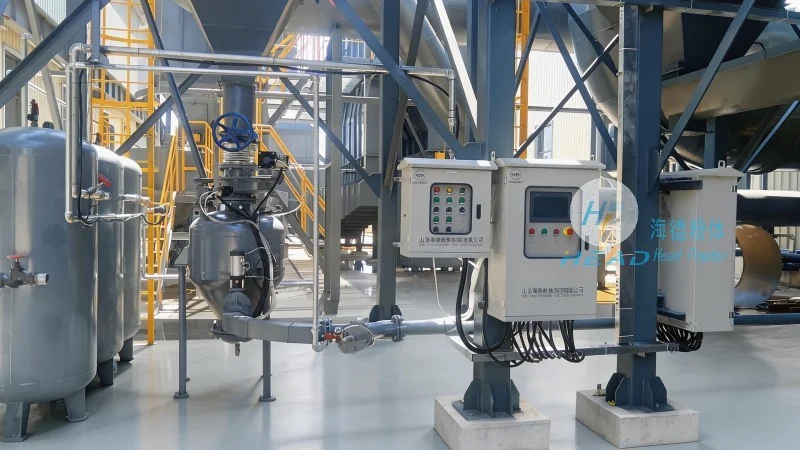
Overview of Quartz Stone Pneumatic Conveying Equipment
Quartz stone pneumatic conveying machines are specialized devices used to transport dry bulk materials like quartz stone through a pipeline system using air pressure. The core components of this equipment include a hopper, a conveying line, a control system, and a dust collection unit. The machine operates by creating a pressure differential between the hopper and the discharge point, allowing the material to be moved without direct contact with mechanical parts. This method not only reduces wear and tear on the material but also minimizes the risk of contamination, making it ideal for applications where product purity is essential.
Key Components and Their Functions
The quartz stone pneumatic conveying machine consists of several critical components, each playing a vital role in the overall operation. The hopper is the primary container where quartz stone is stored before being fed into the system. It is equipped with a feeder that controls the flow rate of the material, ensuring a consistent supply to the conveying line. The conveying line, typically made of stainless steel or other corrosion-resistant materials, is designed to withstand the abrasive nature of quartz stone. The control system monitors and regulates the air pressure and flow rate, maintaining optimal conditions for efficient material transport. Additionally, a dust collection unit is integrated to capture any fine particles, improving air quality and preventing environmental contamination.
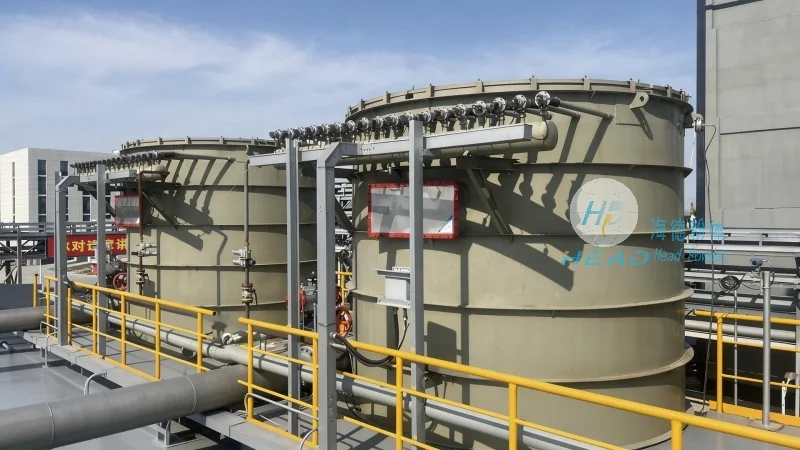
Operation Process of Quartz Stone Pneumatic Conveying Machine
The operation of the quartz stone pneumatic conveying machine follows a systematic process that ensures efficient material transfer. First, the quartz stone is loaded into the hopper. The feeder then regulates the flow of the material into the conveying line. Simultaneously, the control system activates the air compressor, which generates the necessary air pressure to move the material. As the air flows through the conveying line, it carries the quartz stone particles along the pipeline. The material is then discharged at the desired location, such as a storage silo or processing unit. The entire process is automated, with the control system adjusting parameters in real-time to maintain optimal performance. This automated operation reduces the need for manual intervention, enhancing productivity and reducing labor costs.
Working Principle of the Pneumatic Conveying System
The working principle of the quartz stone pneumatic conveying machine is based on the principle of fluidization and air movement. The system operates by creating a negative pressure (suction) or positive pressure (blowing) in the conveying line. In the suction method, the air is drawn from the discharge point, creating a vacuum that pulls the quartz stone particles into the line. In the blowing method, the air is pushed from the hopper end, pushing the material forward. The choice between suction and blowing depends on the application requirements, such as the distance and height of the material transport. The machine uses a combination of these principles to achieve efficient and reliable material transfer. The air flow rate and pressure are carefully controlled to prevent material blockages and ensure smooth operation. This principle allows the equipment to handle various particle sizes and densities of quartz stone, making it versatile for different industrial applications.
Advantages of Using Quartz Stone Pneumatic Conveying Equipment
Implementing quartz stone pneumatic conveying equipment offers several advantages over traditional mechanical conveying methods. Firstly, it eliminates the need for mechanical components like belts or buckets, reducing maintenance costs and extending the equipment's lifespan. The absence of moving parts also minimizes the risk of material contamination, which is critical for applications where product purity is paramount. Additionally, the system is highly flexible, allowing for changes in the conveying route without major modifications. The automated control system ensures consistent performance, reducing downtime and increasing overall productivity. Furthermore, the equipment is energy-efficient, as it uses compressed air to move the material, which can be optimized to reduce energy consumption. These advantages make the quartz stone pneumatic conveying machine a preferred choice for industries dealing with quartz stone, such as glass manufacturing, ceramics, and construction materials.
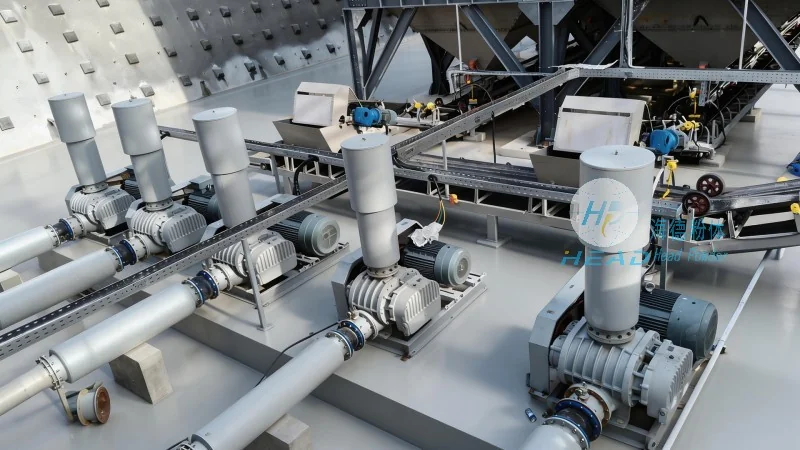
Application Scenarios and Industrial Use Cases
The quartz stone pneumatic conveying machine is widely used in various industrial sectors due to its versatility and efficiency. In the glass industry, it is used to transport quartz stone from storage to the melting furnace, ensuring a continuous supply of raw material. The equipment's ability to handle abrasive materials without wear and tear makes it suitable for this high-temperature environment. In the ceramics industry, quartz stone is used as a raw material for making tiles and ceramics, and the pneumatic conveying machine efficiently transports it to the production lines. The construction industry also benefits from this equipment, as quartz stone is used in concrete and mortar production, and the machine helps in the efficient transfer of the material to the mixing plants. Additionally, the equipment is used in pharmaceutical and food processing industries where product purity is essential, as it prevents contamination and maintains the quality of the material.
Maintenance and Operational Considerations
Proper maintenance is essential to ensure the long-term performance and reliability of the quartz stone pneumatic conveying machine. Regular inspections of the hopper, conveying line, and control system are necessary to identify any potential issues. The feeder should be checked for blockages or wear, as it directly affects the material flow rate. The air compressor and filters should be maintained to ensure optimal air quality and pressure. The dust collection unit should be cleaned regularly to prevent clogging and maintain its efficiency. Operational considerations include monitoring the air pressure and flow rate, as fluctuations can affect the material transport. Additionally, the machine should be operated within the recommended parameters to avoid overloading or damage. By following these maintenance and operational guidelines, the equipment can operate efficiently for extended periods, minimizing downtime and maximizing productivity.