

Operation Process and Working Principle of Sodium Hydroxide Powder Conveying System
The Sodium Hydroxide Powder Conveying System is a specialized industrial equipment designed for the efficient and safe transportation of sodium hydroxide (NaOH) powder. As a key component in various chemical processing applications, this system ensures reliable material handling from storage to processing units. The system is engineered to meet the stringent requirements of industries such as chemical manufacturing, pulp and paper production, and water treatment, where precise and controlled powder handling is critical for operational efficiency and safety.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, the manufacturer of this advanced conveying system, is a leading engineering company based in Shandong, China. With years of experience in the chemical processing equipment sector, HeadPowder specializes in developing customized solutions that enhance operational performance and safety. The company's commitment to quality and innovation has positioned it as a trusted partner for businesses seeking reliable powder handling systems. HeadPowder's engineering team leverages extensive expertise to design systems tailored to specific industrial needs, ensuring optimal performance and longevity.
System Components and Design
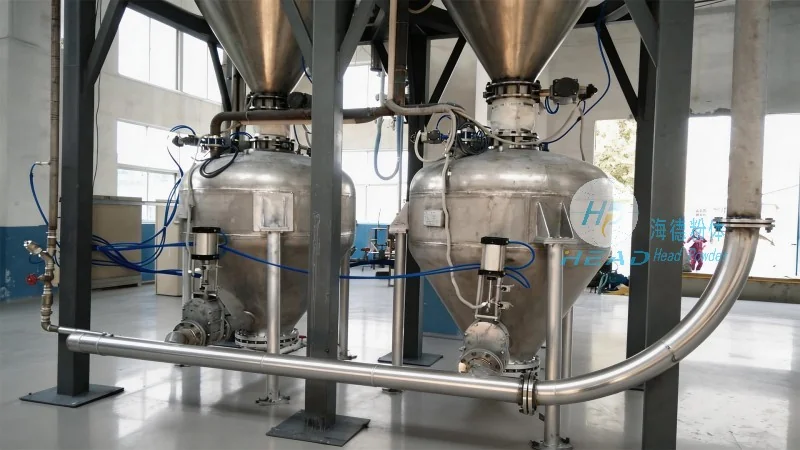
The Sodium Hydroxide Powder Conveying System comprises several key components, each playing a crucial role in the overall operation. The system typically includes a hopper for material storage, a feeder mechanism to control the flow rate, a conveyor (such as a screw conveyor or pneumatic conveyor) for transporting the powder, and a discharge unit for delivering the material to the processing line. The design emphasizes durability and corrosion resistance, as sodium hydroxide is a highly caustic substance that can degrade standard materials over time. Advanced materials, including stainless steel and specialized coatings, are used to protect the system from chemical exposure and mechanical stress.
Working Principle of the Conveying Process
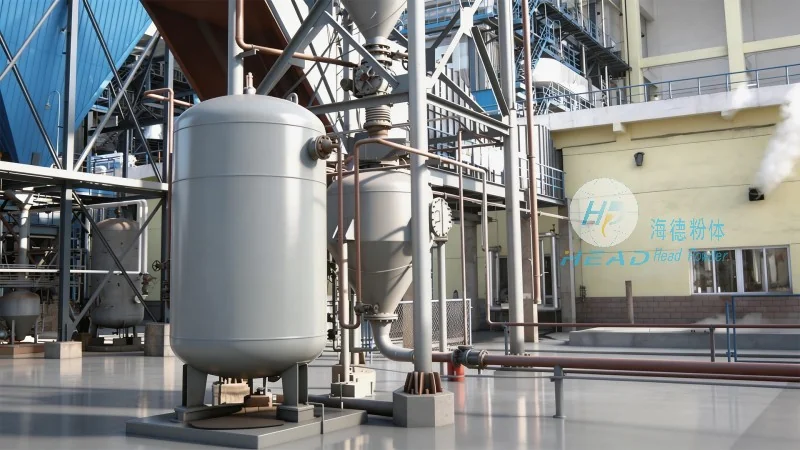
The operation of the Sodium Hydroxide Powder Conveying System follows a systematic process to ensure smooth and continuous material flow. The process begins with the storage of sodium hydroxide powder in the hopper. A feeder, often a rotary valve or a vibratory feeder, regulates the amount of powder released into the conveyor. The conveyor then transports the powder through a series of tubes or a screw mechanism, moving it from the hopper to the discharge point. The system is equipped with sensors and control mechanisms to monitor flow rates, pressure, and material levels, providing real-time feedback to maintain optimal operation. This closed-loop control system helps prevent overfilling, underflow, or blockages, ensuring consistent performance.
Key Features and Benefits
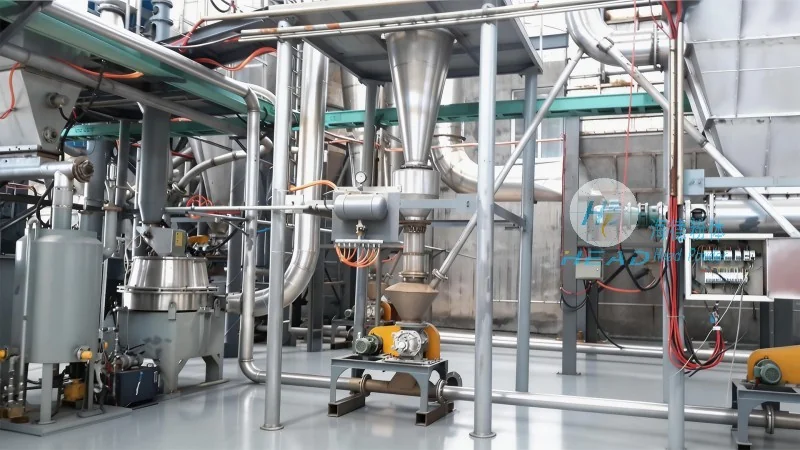
HeadPowder's Sodium Hydroxide Powder Conveying System offers several advantages that enhance industrial operations. The system's robust design minimizes maintenance requirements and extends equipment lifespan, reducing long-term operational costs. The use of corrosion-resistant materials ensures safety and compliance with industry standards, even when handling highly aggressive chemicals. Additionally, the system's modular design allows for easy integration with existing processing lines, facilitating upgrades and modifications as production needs evolve. The precise control of powder flow helps maintain consistent product quality and reduces waste, contributing to higher overall efficiency.
Application Examples and Industry Impact
The Sodium Hydroxide Powder Conveying System is widely used in various industrial applications. In the chemical manufacturing sector, it facilitates the transport of sodium hydroxide to reactors and processing units, enabling efficient production of downstream products such as caustic soda solutions. In the pulp and paper industry, the system supports the handling of sodium hydroxide used in bleaching and pulping processes, improving the quality and consistency of paper products. In water treatment facilities, the system ensures the accurate delivery of sodium hydroxide for pH adjustment and water purification, contributing to cleaner and safer water supplies. By optimizing powder handling, the system enhances operational efficiency, reduces downtime, and improves overall productivity across these industries.