

Operation Process and Working Principle of Organic Salt Powder Conveying System
Organic salt powder conveying systems are critical in industrial applications where the efficient and safe transport of organic salt powders is essential. These systems are designed to handle various organic salt types, ensuring reliable performance in diverse operational environments. The system's design integrates advanced engineering principles to meet the specific demands of modern industrial processes.
Key Components and Their Functions
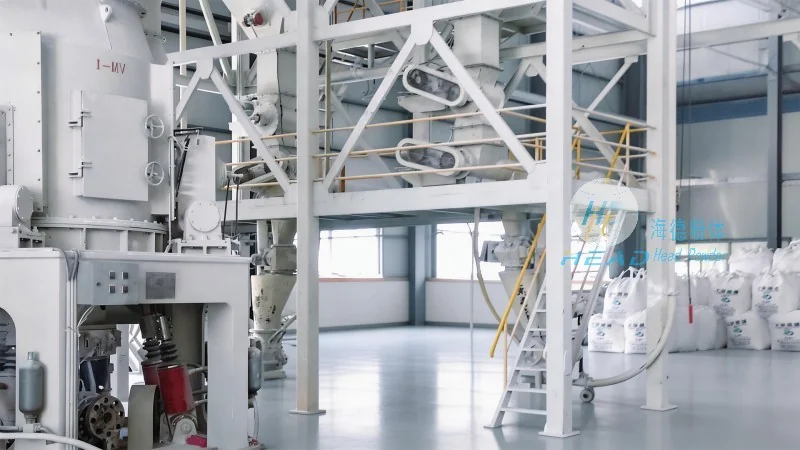
The organic salt powder conveying system comprises several key components, each playing a vital role in the overall operation. The primary components include the hopper for material storage, the conveyor mechanism (such as screw or pneumatic conveyors), the control system for process regulation, and the safety features to prevent material spillage or equipment failure. Each component is carefully selected to ensure compatibility with organic salt properties, such as moisture content, particle size, and chemical stability.
The Operation Process of the System
The operation process of the organic salt powder conveying system begins with material loading into the hopper. The control system monitors the material level and initiates the conveyor when the hopper reaches a predetermined threshold. The conveyor then transports the organic salt powder to the desired destination, such as a storage silo or processing unit. During transport, the system maintains consistent flow rates and pressure levels to prevent clogging or material degradation. The process concludes when the material reaches the target location, with the control system automatically shutting down the conveyor to conserve energy and prevent unnecessary operation.
Working Principle Explained
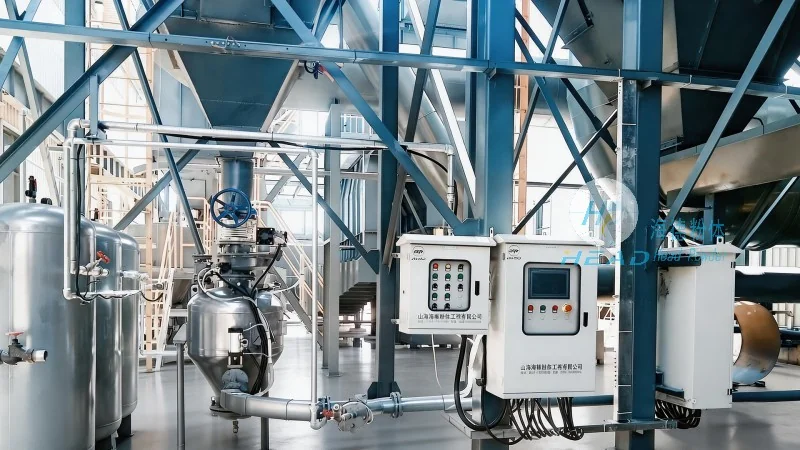
The working principle of the organic salt powder conveying system is based on mechanical or pneumatic force to move the powder. For mechanical conveyors, a rotating screw or auger pushes the material forward, utilizing friction and gravity to maintain flow. Pneumatic systems use compressed air to create a pressure differential, drawing the powder through the pipeline. The system's design ensures that the conveying pressure and velocity are optimized to handle organic salt's characteristics, minimizing particle degradation and ensuring efficient transport. The control system continuously monitors parameters like pressure, flow rate, and temperature to adjust the operation in real-time, enhancing system reliability and performance.
Technical Specifications and Performance
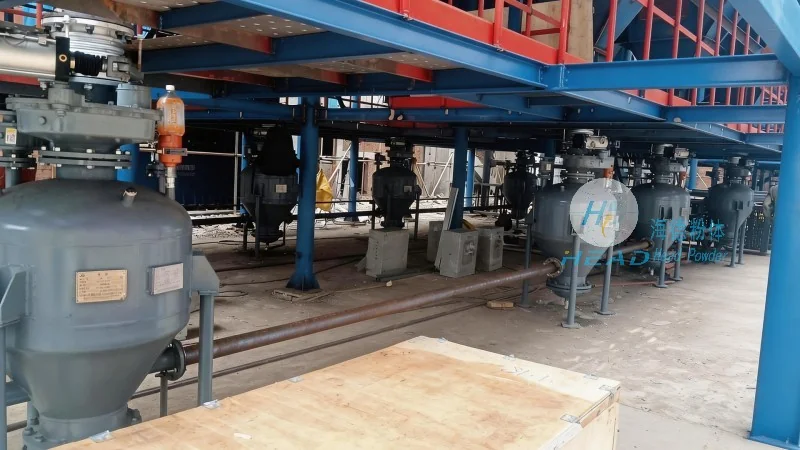
Technical specifications of the organic salt powder conveying system vary based on the application requirements. Key specifications include the conveying capacity (measured in tons per hour), the maximum particle size (typically up to 5 mm for most organic salts), the operating pressure (ranging from low to high depending on the system design), and the power consumption. The system is engineered to handle organic salts with varying moisture content, ensuring that the material remains dry and free-flowing throughout the conveying process. Additionally, the system incorporates corrosion-resistant materials to withstand the chemical properties of organic salts, extending the equipment's service life and reducing maintenance costs.
Application Scenarios and Benefits
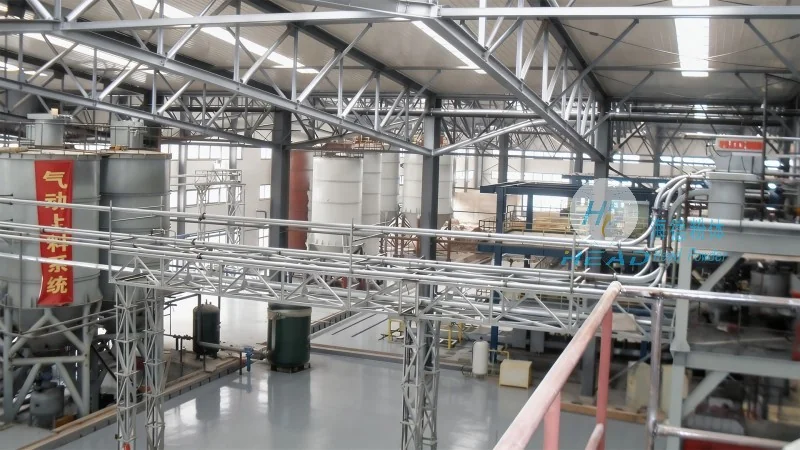
Organic salt powder conveying systems are widely used in various industries, including chemical manufacturing, food processing, and pharmaceutical production. In chemical plants, these systems transport organic salts used in the production of fertilizers, detergents, and other chemical products. In food processing facilities, they handle organic salts like sodium bicarbonate or potassium chloride for baking and seasoning applications. The system's versatility allows it to adapt to different production scales, from small-scale batch processing to large-scale continuous operations. The benefits of using such systems include improved operational efficiency, reduced labor costs, and enhanced safety by minimizing manual handling of organic salts.
Company Information and Contact Details
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in the design, manufacturing, and installation of advanced powder conveying systems. With a focus on innovation and quality, the company has established itself as a leading provider of organic salt powder conveying solutions. Headpowder's systems are engineered to meet international standards and are tailored to the specific needs of each client. The company's headquarters is located in Shandong, China, where it maintains a state-of-the-art manufacturing facility and a dedicated research and development team. Headpowder's commitment to customer satisfaction and technical excellence has earned it a reputation for delivering reliable and efficient powder conveying systems to clients worldwide.