

Operation Process and Working Principle of Metering Bin Pump Powder Conveying System Equipment
HeadPowder, a leading provider in the field of powder handling technology, specializes in the design, manufacturing, and integration of advanced metering bin pump systems. These systems are engineered to efficiently transport bulk powders with precision and reliability, catering to various industrial applications. The following content delves into the operational process and underlying working principles of such equipment, highlighting the key components and their functions.
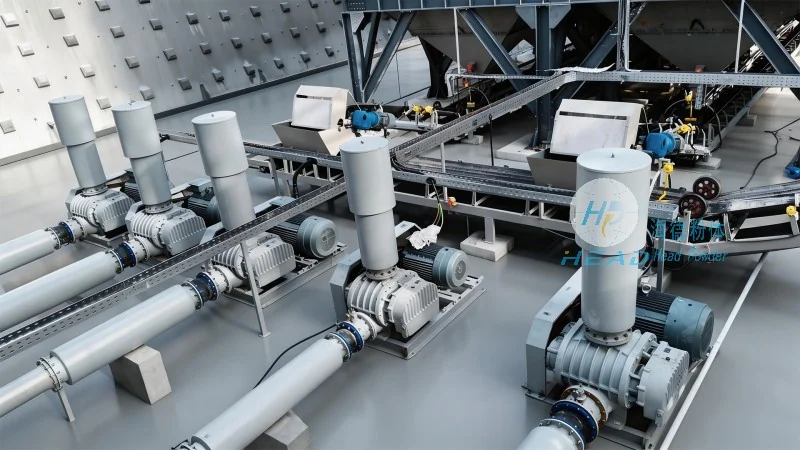
Key Components of the Metering Bin Pump System
The metering bin pump system typically comprises several critical components that work in concert to ensure optimal performance. These include the metering bin, the pump body, the actuator system, the control panel, and various auxiliary devices such as valves, sensors, and piping. Each component plays a vital role in the overall functionality of the system. The metering bin serves as the storage vessel for the bulk powder, while the pump body houses the mechanism that generates the necessary pressure to move the material. The actuator system, often hydraulic or pneumatic, controls the movement of the pump plunger or diaphragm, enabling the precise metering and discharge of the powder. The control panel integrates sensors and control logic to monitor and regulate the operation, ensuring safety and efficiency. Auxiliary devices like check valves, pressure relief valves, and flow meters assist in maintaining system stability and providing feedback on the material flow.
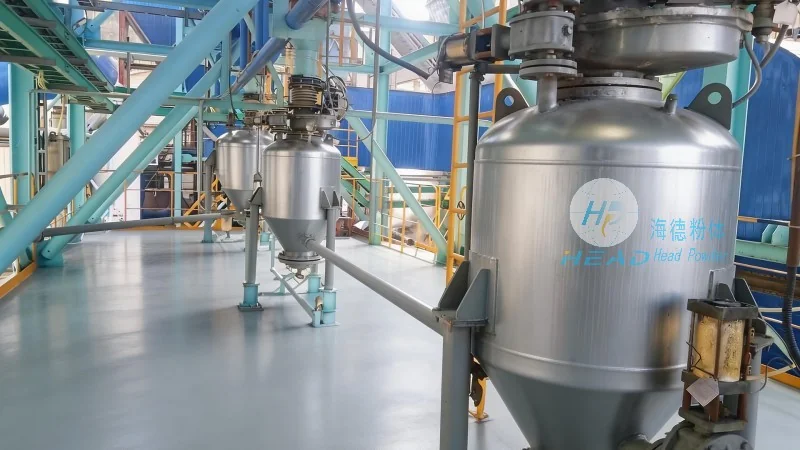
Operation Process of the Metering Bin Pump
The operation of the metering bin pump follows a systematic sequence that ensures consistent and accurate powder delivery. The process begins with the loading of the bulk powder into the metering bin. Once the bin is filled, the system prepares for the conveying operation. The control panel initiates the actuation sequence, which involves the movement of the pump plunger or diaphragm. In the suction phase, the pump creates a vacuum to draw the powder from the bin into the pump chamber. This is followed by the compression phase, where the actuator forces the plunger or diaphragm to push the powder through the discharge line. The discharge phase involves the release of the material under pressure into the downstream process or storage. The cycle repeats as needed, with the control system adjusting the frequency and duration of the actuation to maintain the desired flow rate. This continuous operation allows for precise control over the quantity of powder conveyed, making it suitable for applications requiring exact dosing or batching.
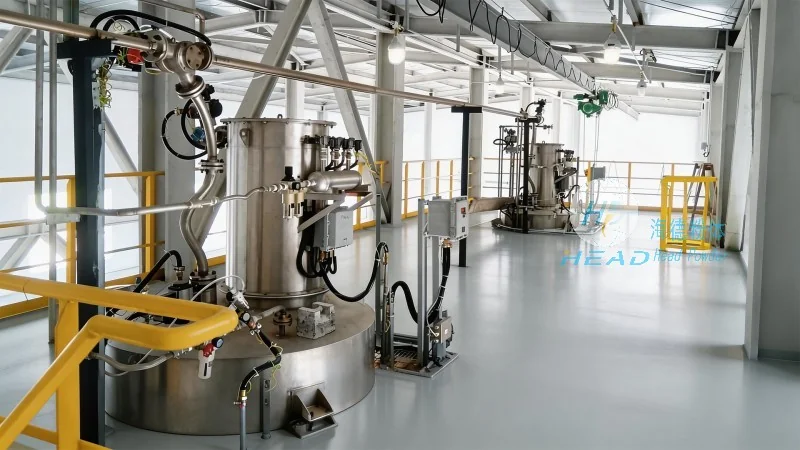
Working Principle of the Metering Bin Pump
The working principle of the metering bin pump is based on the displacement of a fluid or solid within a confined space, utilizing the principles of pressure and volume change. In the case of a diaphragm pump, for example, the actuator moves the diaphragm back and forth, creating a series of compression and expansion cycles. During the compression stroke, the diaphragm pushes against the powder in the pump chamber, increasing the pressure and forcing the material out through the discharge valve. The suction stroke then occurs as the diaphragm retracts, creating a low-pressure area that draws the powder from the metering bin into the chamber. This cyclical motion ensures a consistent flow of powder, with the volume of material displaced per cycle being directly proportional to the pump's design and the actuation speed. The control system monitors parameters such as pressure, flow rate, and cycle time to maintain the desired performance, adjusting the actuator speed or stroke length as necessary. The overall principle ensures that the system can handle a wide range of powder characteristics, including different particle sizes, densities, and flowabilities, while maintaining high efficiency and reliability.
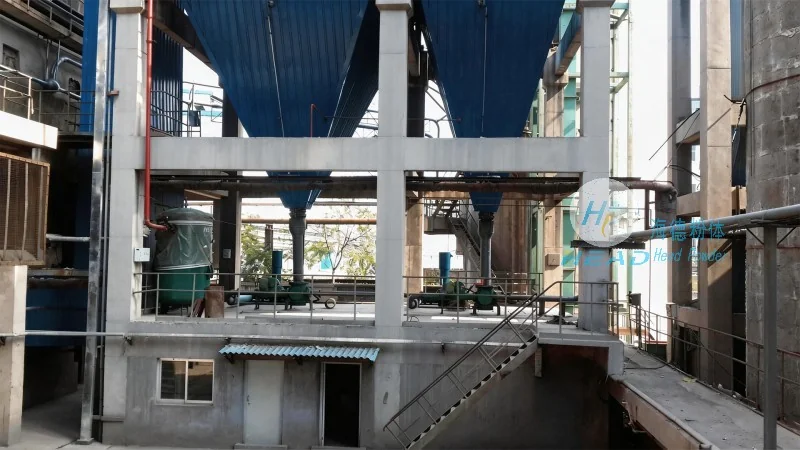
Advantages and Applications of the Metering Bin Pump System
The metering bin pump system offers several advantages that make it a preferred choice for bulk powder handling in various industries. These include high accuracy in powder metering, which is crucial for applications requiring precise dosing, such as pharmaceutical manufacturing, food processing, and chemical production. The system also provides reliable and continuous operation, with minimal downtime due to its robust design and automated control features. Additionally, the equipment is versatile and can handle a wide range of powder types, from fine powders to bulk materials, without the need for extensive modifications. The system's ability to operate under different pressure and flow conditions makes it suitable for both low and high-volume applications. In industrial settings, the metering bin pump is commonly used in processes such as material feeding, batching, and transfer, where consistent and controlled powder flow is essential. The system's integration with other process equipment, such as mixers, reactors, and conveyors, enhances overall process efficiency and reduces manual intervention.