

Operation Process and Working Principle of Small Bag Unpacking Powder Conveying System Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced small bag unpacking powder conveying systems. These systems are engineered to efficiently handle the handling, unpacking, and transportation of bulk powders from sealed bags, ensuring seamless integration into industrial production lines. The equipment is widely used in sectors such as chemical, food, pharmaceutical, and agricultural industries, where reliable and hygienic powder handling is critical.
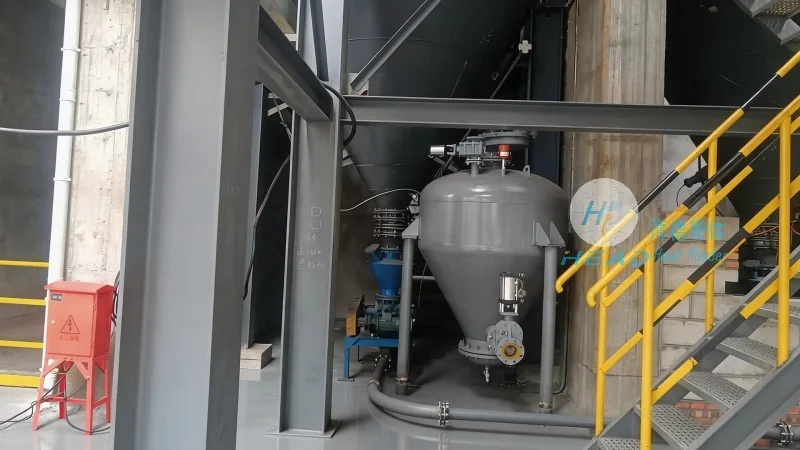
Overview of the Small Bag Unpacking Powder Conveying System
The small bag unpacking powder conveying system is a sophisticated piece of industrial equipment designed to automate the process of receiving, unpacking, and transporting bulk powders from small bags. The system typically consists of several key components, including a bag opening mechanism, a weighing or dosing unit, a conveying system (often pneumatic or mechanical), and a control panel. Each component works in tandem to ensure precise and efficient powder handling, minimizing human intervention and reducing the risk of contamination.
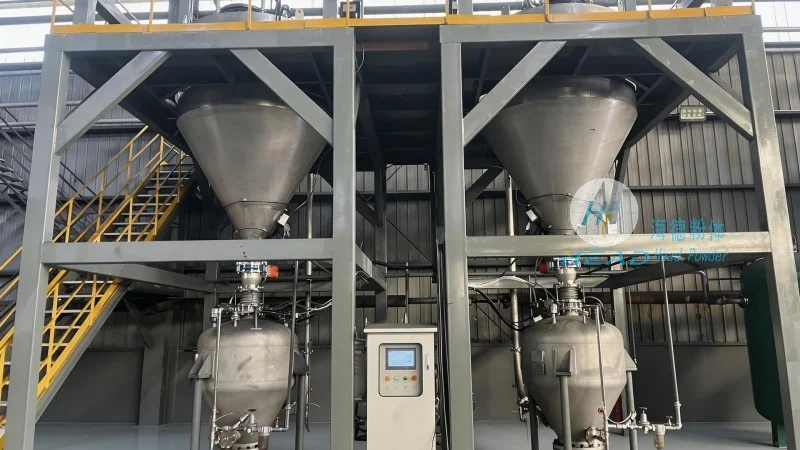
Operation Process of the Small Bag Unpacking Powder Conveying System
The operation of the small bag unpacking powder conveying system follows a systematic sequence of steps, each designed to ensure accuracy and efficiency. The process begins with the placement of a sealed bag onto the system's loading platform. The bag is then positioned under the opening mechanism, which uses mechanical or pneumatic tools to cut or tear the bag open, releasing the powder into a hopper or collection chamber. Following the bag opening, the system may perform a weighing or dosing operation to measure the exact amount of powder, which is crucial for applications requiring precise quantities. Once the required amount is determined, the powder is transferred to the conveying system, which transports it to the next stage of the production process, such as mixing, blending, or packaging. The entire operation is controlled by an advanced control system, which monitors each step and adjusts parameters as needed to maintain optimal performance.
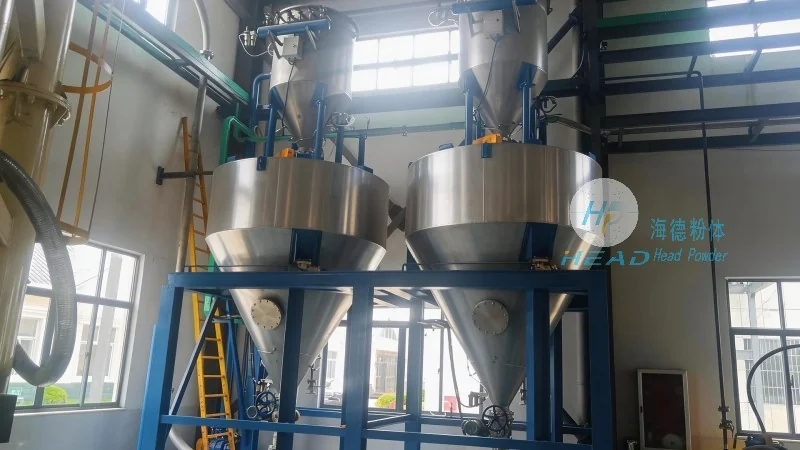
Working Principle of the Small Bag Unpacking Powder Conveying System
The working principle of the small bag unpacking powder conveying system is based on the integration of mechanical, pneumatic, and electronic components, all coordinated by a central control unit. The bag opening mechanism, which may include blades, air nozzles, or cutting tools, is activated to access the powder inside the bag. The powder then falls into a hopper, where it is either stored temporarily or directly fed into the conveying system. The conveying system, often utilizing air pressure or mechanical screws, moves the powder through a pipeline or conveyor belt to the destination. The control panel, equipped with sensors and feedback mechanisms, continuously monitors the flow rate, pressure, and other parameters, ensuring that the powder is conveyed at the correct speed and volume. This closed-loop control system enhances the system's reliability and accuracy, minimizing errors and waste.
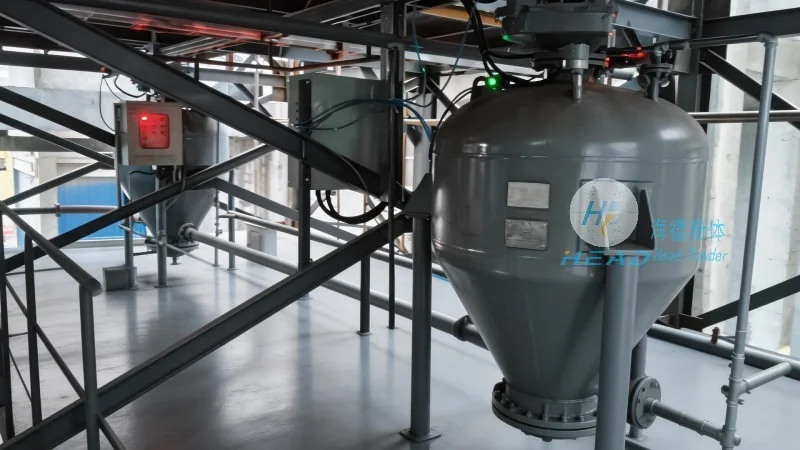
Key Features and Benefits of the Small Bag Unpacking Powder Conveying System
HeadPowder's small bag unpacking powder conveying systems are equipped with several features that enhance their performance and usability. These include automatic bag opening, which eliminates the need for manual intervention and reduces labor costs; precise weighing or dosing capabilities, which ensure consistent product quality; and a hygienic design, which minimizes the risk of contamination in food and pharmaceutical applications. The systems are also designed for easy maintenance and cleaning, with removable components that can be disassembled and sanitized. Additionally, the advanced control system allows for remote monitoring and adjustment, providing operators with real-time data on the system's performance. The overall benefits of these systems include increased efficiency, reduced downtime, improved product quality, and enhanced safety in the workplace.