

Operation Process and Working Principle of Powder Pneumatic Conveying System for Food Additives
For food manufacturers, the efficient and safe handling of food additives is crucial to maintaining product quality and operational efficiency. A powder pneumatic conveying system designed specifically for food additives offers a reliable solution that ensures precise material transport while adhering to strict industry standards. This article explores the operation process and working principle of such a system, highlighting its key components, operational mechanics, and the benefits it provides to the food processing industry.
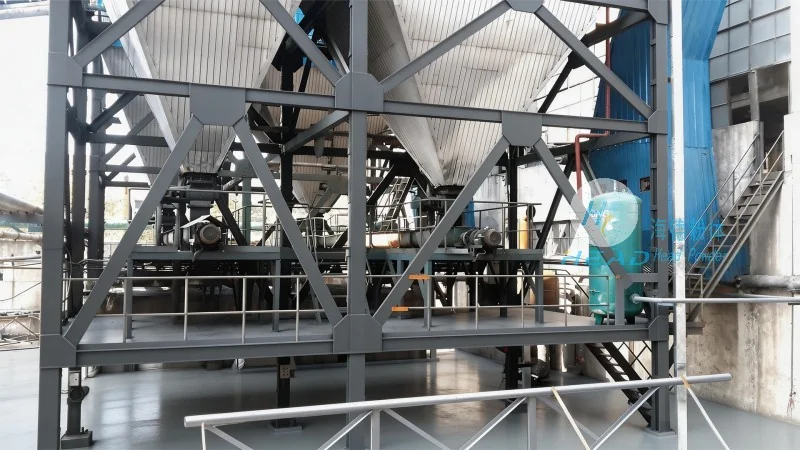
Understanding the Core Components of a Food Additive Pneumatic Conveying System
The foundation of any effective powder pneumatic conveying system lies in its carefully engineered components, each playing a vital role in the overall performance and safety of the operation. The system typically includes a number of key elements, such as a hopper for material storage, a feeder to control the flow of powder, a conveying line (often equipped with filters or cyclones to prevent dust accumulation), and a receiver for the delivered material. These components are meticulously designed to handle the unique properties of food additives, which may include varying particle sizes, moisture content, and sensitivity to contamination.
Working Principle: How the System Transports Powder
The working principle of a pneumatic conveying system for food additives revolves around the use of air to move powder through a closed pipeline. The process begins with the material being discharged from the hopper into the feeder, which regulates the flow rate to maintain consistent pressure and prevent blockages. The feeder then feeds the powder into the conveying line, where it is entrained by high-velocity air flowing through the pipeline. As the powder particles are carried along by the air stream, they are transported to the receiver, where the air is separated from the material and either filtered or vented back into the system. This method of operation ensures that the food additive is moved without direct contact with external surfaces, minimizing the risk of contamination and preserving the product's integrity.
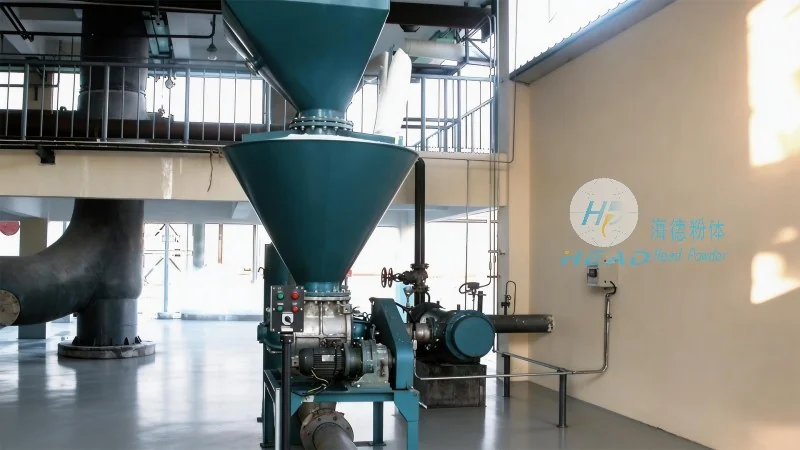
Operation Process: Step-by-Step Execution
The operation of a food additive pneumatic conveying system follows a systematic process that ensures smooth and continuous material transport. The process typically begins with the preparation of the system, which involves checking the hopper for sufficient material, verifying the feeder settings, and ensuring that all components are properly lubricated and free of obstructions. Once the system is ready, the feeder is activated to start the flow of powder. The air compressor then generates the necessary pressure to move the material through the conveying line. As the powder is transported, the system continuously monitors pressure and flow rates to maintain optimal performance. The receiver collects the delivered material, and the process repeats as needed. This step-by-step approach ensures that the system operates efficiently and reliably, minimizing downtime and maximizing productivity.
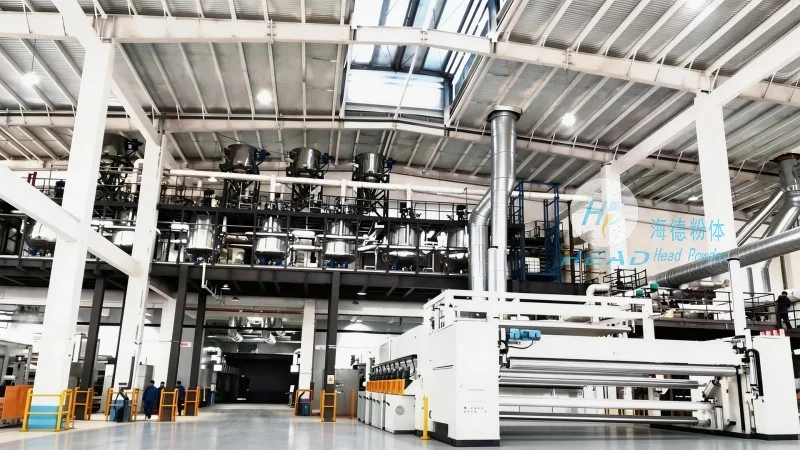
Benefits and Advantages of Using a Food Additive Pneumatic Conveying System
Implementing a powder pneumatic conveying system for food additives offers numerous benefits that enhance both operational efficiency and product quality. One of the primary advantages is the ability to transport materials in a closed system, which significantly reduces the risk of contamination from external sources. This is particularly important for food additives, as even minor contaminants can impact the safety and taste of the final product. Additionally, the system allows for precise control over the flow rate and pressure, ensuring that the material is delivered at the exact rate required by the production process. This precision helps to maintain consistent product quality and reduces waste. The closed system also minimizes dust emissions, improving workplace safety and compliance with environmental regulations. Furthermore, the system's ability to handle a wide range of particle sizes and moisture content makes it versatile and suitable for various food additive applications.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of advanced powder handling solutions, including pneumatic conveying systems for food additives. With a strong commitment to quality and innovation, the company specializes in designing and manufacturing systems that meet the unique needs of the food processing industry. HeadPowder's systems are engineered to adhere to strict industry standards, ensuring that they are safe, reliable, and efficient. The company's headquarters is located in Shandong, China, where it has established a reputation for delivering high-quality products and exceptional customer service. By leveraging its expertise in powder technology, HeadPowder provides tailored solutions that help food manufacturers optimize their operations and maintain the highest standards of product quality.