

What is a Negative Pressure Vacuum Powder Conveying System Device? And What Are Its Design Principle
The negative pressure vacuum powder conveying system is a specialized equipment designed for the efficient and safe transportation of bulk powders over long distances. This technology is widely used in various industries such as chemical, food, pharmaceutical, and cement, where the handling of fine or abrasive powders requires precise control and minimal product loss. The system operates by creating a negative pressure environment in the conveying line, which draws the powder from the source to the destination through a sealed pipeline.
Core Design Principles of the System
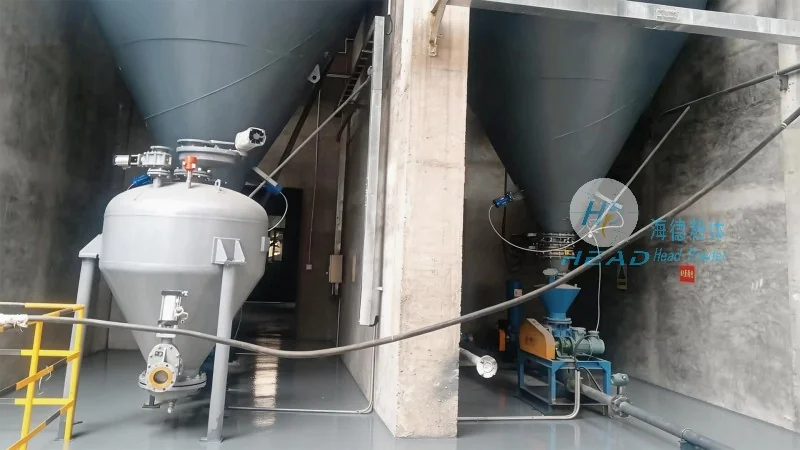
The fundamental design principle of a negative pressure vacuum powder conveying system is based on fluid dynamics and vacuum technology. The system comprises several key components that work in concert to achieve efficient powder transport. These components include a vacuum pump, a filter, a conveying pipe, and a control system. The vacuum pump is responsible for generating the necessary negative pressure, which creates a pressure differential between the source and the destination. The filter, typically located at the inlet of the system, serves to separate the powder from the air and remove any contaminants, protecting both the pump and the downstream equipment from damage. The conveying pipe is constructed from materials that are resistant to corrosion and wear, such as stainless steel or high-density polyethylene, to accommodate the specific properties of the powders being transported. The control system monitors critical parameters like pressure, flow rate, and temperature, ensuring the system operates within safe and optimal conditions.
Working Mechanism and Operational Process
When the system is activated, the vacuum pump begins to operate, establishing a negative pressure within the conveying line. This pressure differential causes the powder to be drawn from the source (e.g., a hopper or silo) into the sealed pipeline. The powder travels through the pipe due to the continuous suction created by the vacuum pump. The filter at the inlet prevents the powder from entering the pump directly, maintaining the integrity of the equipment and ensuring that only clean air passes through the system. The control system continuously adjusts the pump speed or pressure as needed to maintain a consistent flow rate, preventing clogging or excessive pressure drops that could lead to system failure. This closed-loop operation ensures that the powder is transported safely and efficiently, with minimal loss or contamination.
About Shandong HeadPowder Engineering Co., Ltd.
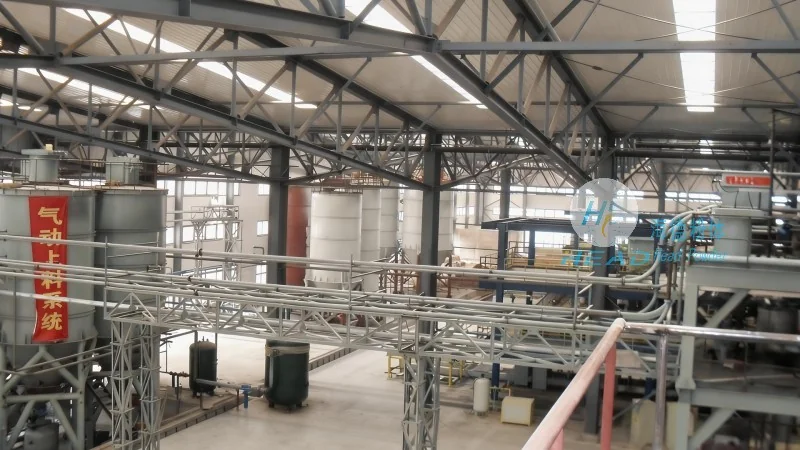
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of negative pressure vacuum powder conveying systems. HeadPowder has been in the industry for many years, specializing in the design, development, and installation of advanced powder handling solutions. The company is headquartered in Shandong, China, and has a team of experienced engineers, technicians, and sales professionals dedicated to providing high-quality products and reliable services to clients worldwide. HeadPowder focuses on customizing systems to meet the unique requirements of different industries, ensuring that their solutions are both efficient and cost-effective.
Advantages of Negative Pressure Vacuum Conveying Systems
Compared to traditional conveying methods such as pneumatic or mechanical systems, negative pressure vacuum conveying offers several distinct advantages. One of the primary benefits is the clean and hygienic operation, which is essential for industries dealing with food, pharmaceutical, and cosmetic products. The sealed pipeline prevents dust and contamination from escaping into the environment, maintaining product purity throughout the conveying process. Additionally, the system is energy-efficient, as it uses less power to operate compared to positive pressure systems, which can result in significant cost savings over time. The negative pressure method also allows for the handling of a wide range of powder types, including fine powders, bulk materials, and even sensitive powders that are prone to moisture or temperature changes. The system's ability to handle abrasive or corrosive powders without causing wear or damage to the equipment further enhances its versatility.
Design Considerations and Customization
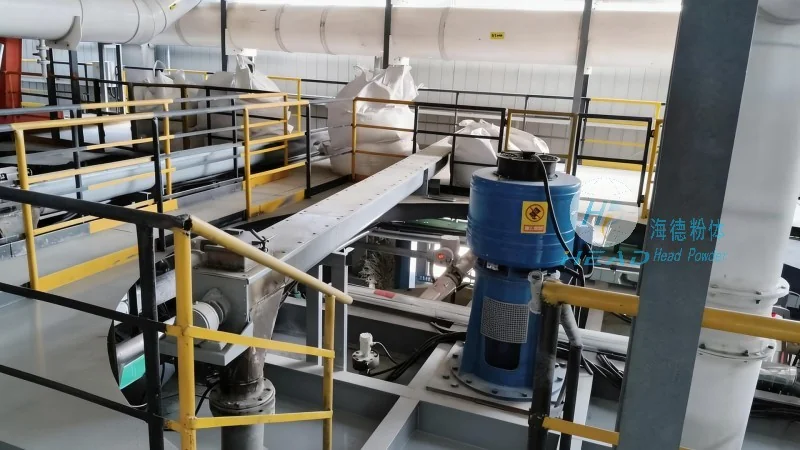
The design of a negative pressure vacuum powder conveying system is tailored to the specific characteristics of the powder being transported and the operational requirements of the client. Key factors that influence the design include the powder's particle size, density, flowability, and moisture content. The conveying distance and the required flow rate also play a critical role in determining the system's specifications. HeadPowder's engineering team works closely with clients to conduct thorough assessments of their powder properties and application needs. Based on this information, they design a customized system that optimizes performance, minimizes energy consumption, and ensures long-term reliability. The company offers a range of standard and custom configurations, including different pump sizes, filter types, and pipe materials, to accommodate diverse industrial applications.
Applications and Industries
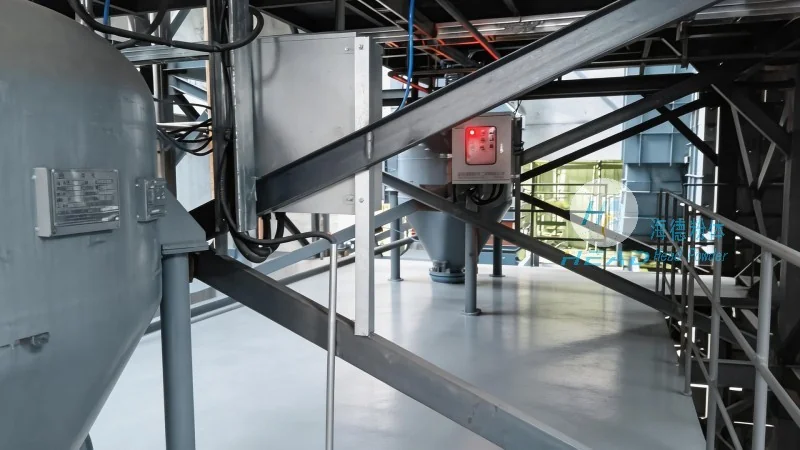
Negative pressure vacuum powder conveying systems are used in a variety of industries where bulk powder handling is essential. In the chemical industry, they are used to transport raw materials and finished products, such as pigments, polymers, and fertilizers. The food and pharmaceutical industries rely on these systems to handle ingredients and products that require strict hygiene and contamination control. The cement and construction sectors use them for transporting raw materials like limestone and clinker. Additionally, the system is applicable in the agricultural industry for handling grain and other agricultural products. The versatility of the negative pressure vacuum conveying system makes it a preferred choice in many sectors due to its ability to handle different powder types and its efficiency in long-distance transport.
Conclusion
In summary, the negative pressure vacuum powder conveying system is a sophisticated piece of equipment that leverages vacuum technology to efficiently and safely transport bulk powders. Its design principles, based on fluid dynamics and careful component selection, ensure optimal performance and reliability. Companies like Shandong HeadPowder Engineering Co., Ltd. specialize in providing these systems, customizing them to meet the specific needs of various industries. The advantages of this technology, including clean operation, energy efficiency, and versatility, make it an essential solution for industries dealing with powders. As the demand for efficient powder handling continues to grow, the negative pressure vacuum conveying system remains a reliable and effective choice for businesses seeking to improve their operational efficiency and product quality.