

What is a Nitrogen-Protected Powder Handling System? Explained: Design Principles and Applications
For industries dealing with powders, maintaining product integrity and safety is paramount. A nitrogen-protected powder handling system is a specialized solution designed to address these challenges by creating an inert atmosphere around the material being transported. This system is particularly crucial in sectors where oxidation, moisture, or contamination could compromise the quality of the powder, such as pharmaceuticals, food processing, and chemical manufacturing.
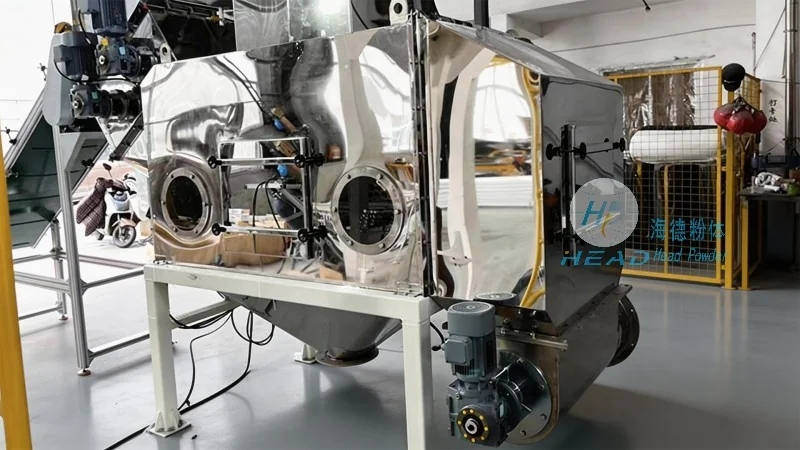
Understanding the Core Function of Nitrogen Protection in Powder Handling
The primary function of a nitrogen-protected system is to displace oxygen and moisture from the powder and the surrounding environment. By introducing nitrogen gas, which is chemically inert, the system prevents oxidation reactions that can alter the powder's properties. This is achieved through a closed-loop or semi-closed-loop design that ensures the nitrogen gas remains in contact with the powder throughout the handling process, from storage to discharge.
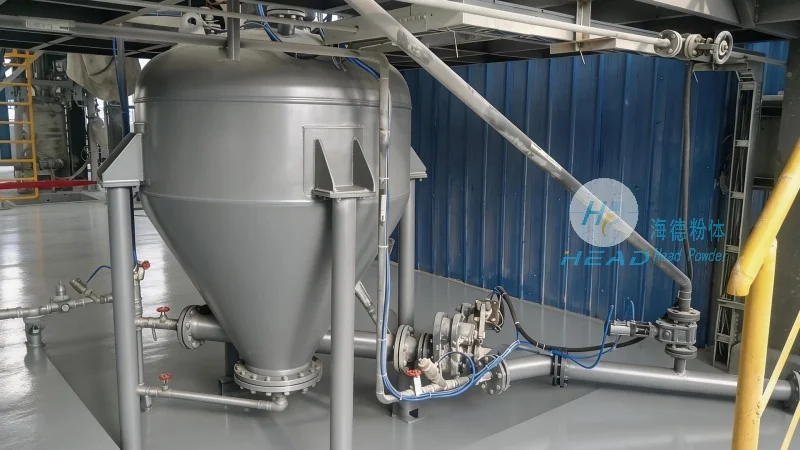
Design Principles Behind Nitrogen-Protected Systems
The design of a nitrogen-protected powder handling system is based on several key principles to ensure efficiency and reliability. First, the system must maintain a positive pressure environment, which prevents external air from entering and contaminating the powder. This is typically achieved by using nitrogen gas to pressurize the system's storage and transport vessels. Second, the system incorporates proper gas distribution mechanisms, such as diffusers or spargers, to ensure uniform nitrogen coverage. Third, the design includes effective sealing and leak detection features to maintain the integrity of the inert atmosphere. Additionally, the system is engineered to minimize particle attrition and degradation, which can occur during handling and transfer.
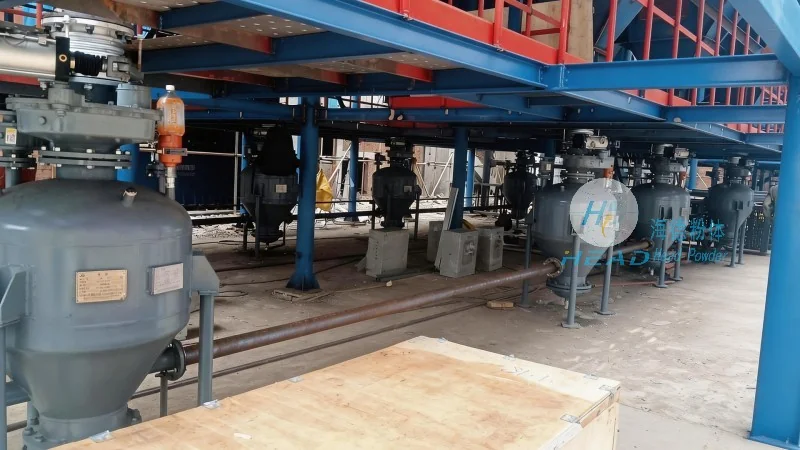
Key Components and Their Roles in the System
Several critical components make up a nitrogen-protected powder handling system. The main components include a nitrogen gas source, such as a high-purity nitrogen generator or cylinder, and a pressure regulator to control the gas flow. The system also features a storage silo or hopper that is equipped with a nitrogen inlet and outlet to maintain the inert atmosphere. For transport, the system may use pneumatic conveying lines or bulk material handling equipment, such as screw conveyors or bucket elevators, that are integrated with nitrogen gas distribution. The system also includes sensors and controls to monitor pressure, temperature, and gas flow, ensuring the system operates within safe and optimal parameters. Additionally, the design may incorporate dust collection and filtration systems to maintain air quality and prevent particle release.
Application Scenarios and Industry Benefits
Nitrogen-protected powder handling systems are widely used in various industries where powder quality and safety are critical. In the pharmaceutical industry, these systems are essential for handling active pharmaceutical ingredients (APIs) and excipients, as even trace amounts of moisture or oxygen can affect the efficacy and stability of the drug. In food processing, the systems are used to handle ingredients like flour, sugar, and spices, ensuring they remain fresh and free from spoilage. In chemical manufacturing, the systems are crucial for handling reactive powders that could cause explosions or fires if exposed to air. The benefits of using such systems include improved product quality, extended shelf life, reduced waste due to contamination, and enhanced safety for operators. Furthermore, the systems help meet regulatory requirements for handling sensitive materials, ensuring compliance with industry standards and guidelines.
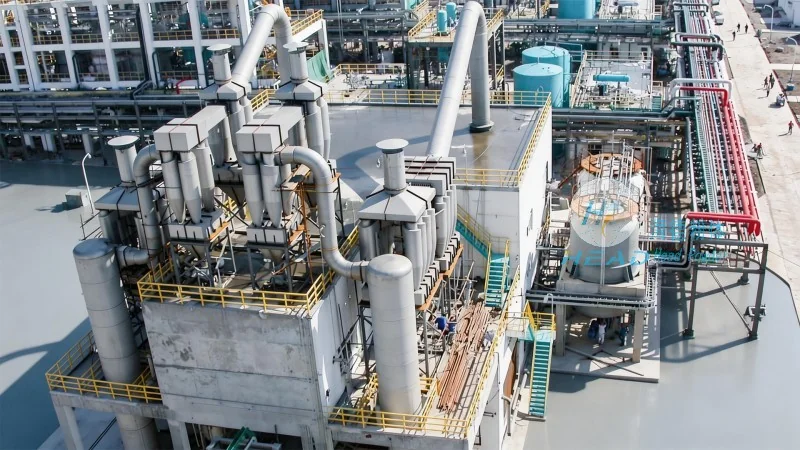
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of advanced powder handling systems, including nitrogen-protected solutions. The company is headquartered in Shandong, China, and has a strong reputation for delivering high-quality, reliable equipment tailored to the specific needs of its clients. With years of experience in the industry, HeadPowder has developed a comprehensive range of products that cater to various applications, from small-scale laboratory use to large-scale industrial operations. The company's commitment to innovation and customer satisfaction has made it a trusted partner for businesses seeking efficient and safe powder handling solutions. HeadPowder's products are designed with precision engineering and rigorous testing to ensure they meet the highest standards of performance and durability. The company also provides technical support and after-sales services to help clients optimize their powder handling processes and maximize operational efficiency.