

What is a Purified Ash Material Handling System? What are its Design Principles?
For industries reliant on combustion processes, the management of ash byproducts is a critical operational and environmental challenge. A purified ash material handling system addresses these challenges by providing an efficient, controlled method to transport and handle ash materials. Understanding the design principles behind such systems is essential for optimizing performance, ensuring compliance with regulations, and enhancing overall operational efficiency. This article explores the key aspects of purified ash material handling systems, including their components, design considerations, and applications, with a focus on the expertise of Shandong HeadPowder Engineering Co., Ltd.
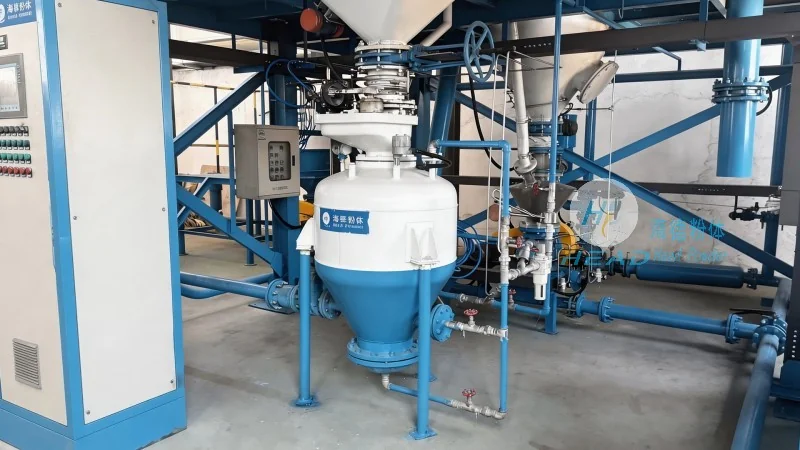
Overview of Purified Ash Material Handling Systems
A purified ash material handling system is a comprehensive setup designed to handle ash, a byproduct of combustion, from its generation point to its final destination. These systems are commonly used in power plants, cement factories, and other industrial facilities where ash management is integral to both environmental sustainability and resource utilization. The primary goal of the system is to transport ash safely and efficiently while minimizing dust emissions and ensuring operational reliability. The system typically integrates multiple components, including conveyors, dust collection equipment, storage facilities, and control systems, all working in harmony to achieve these objectives.
Core Components and Their Functions
The effectiveness of a purified ash material handling system hinges on its core components, each playing a vital role in the overall operation. First, ash conveyors are the backbone of the system, responsible for moving ash from the source to the next stage. These can be pneumatic conveyors, which use air pressure to transport ash through pipelines, or mechanical conveyors, such as belt or screw conveyors, which rely on mechanical force. The choice of conveyor type depends on factors like ash characteristics (e.g., moisture content, particle size), distance to be covered, and the required flow rate. Second, dust collection systems are critical for maintaining air quality and complying with environmental regulations. These systems, including baghouses and electrostatic precipitators, capture and remove airborne particles, preventing dust from escaping into the environment. Third, storage silos or hoppers are used to temporarily store ash before further processing or disposal. These structures are designed to handle the bulk density and flow characteristics of ash, ensuring stable storage and easy access for downstream operations.
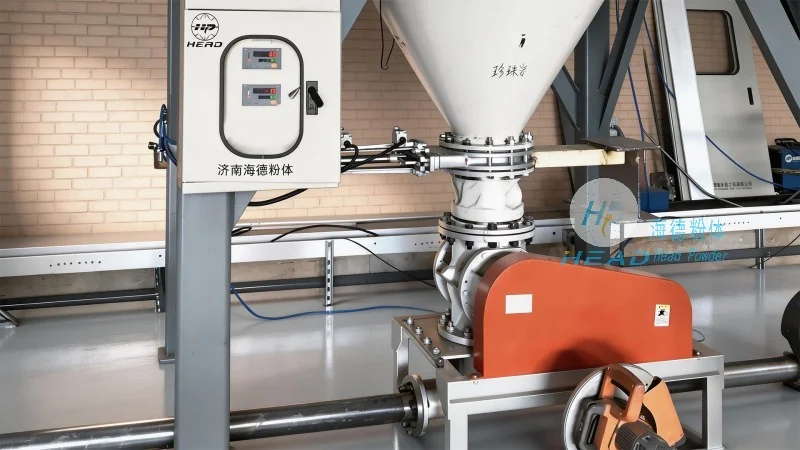
Design Principles for Optimal Performance
The design of a purified ash material handling system follows several key principles to ensure efficiency, reliability, and safety. First, material flow optimization is paramount to prevent blockages and ensure consistent transport. Engineers carefully calculate the ash's bulk density, flowability, and other properties to select the appropriate conveyor size and speed. This helps maintain a smooth flow and reduces the risk of system downtime. Second, dust control is a major design consideration, as ash particles can be abrasive and pose health risks. Advanced filtration technologies, such as high-efficiency particulate air (HEPA) filters or electrostatic precipitators, are integrated to capture fine particles and minimize emissions. Third, equipment durability is essential due to the harsh conditions of ash handling. Components are constructed from materials resistant to abrasion, corrosion, and high temperatures, ensuring long-term performance and reducing maintenance costs. Additionally, the system is designed for easy maintenance and accessibility, allowing for quick repairs and replacements without disrupting operations.
Applications and Benefits in Industrial Settings
Purified ash material handling systems find widespread application in various industries, with power generation and cement manufacturing being the most prominent. In power plants, these systems manage fly ash and bottom ash, which can be utilized as a raw material in cement production or as a soil amendment, reducing the need for virgin materials and lowering environmental impact. The benefits of implementing such a system extend beyond environmental compliance. Efficient ash handling reduces operational costs by minimizing downtime and maintenance expenses. It also enhances workplace safety by controlling dust exposure and preventing accidents. Furthermore, the system's flexibility allows for adaptation to changing operational needs, such as varying ash production rates or different disposal methods.
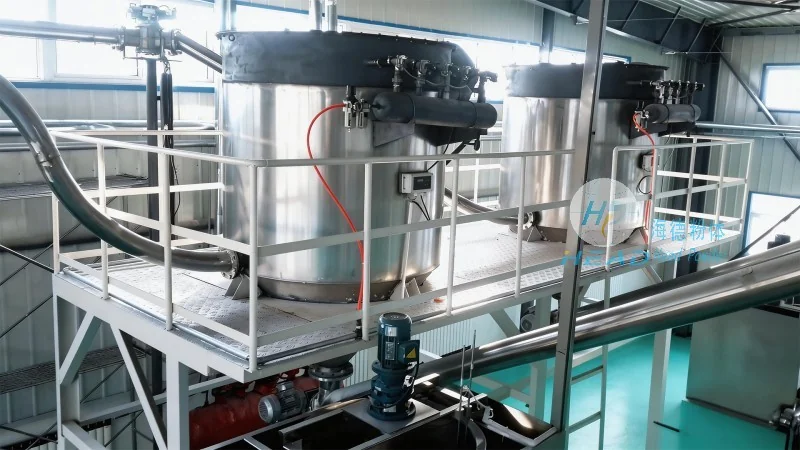
Shandong HeadPowder Engineering Co., Ltd.: A Leader in Ash Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a distinguished company specializing in the design and manufacturing of advanced material handling systems. Headquartered in Shandong, China, the company has built a strong reputation for delivering high-quality, customized solutions tailored to the unique requirements of ash and bulk material handling. With a team of experienced engineers and technicians, HeadPowder leverages cutting-edge technology and robust engineering principles to develop systems that meet or exceed industry standards. The company's commitment to innovation and customer satisfaction has made it a trusted partner for businesses seeking to optimize their ash handling processes and achieve sustainable operations.
Conclusion
In conclusion, a purified ash material handling system is a sophisticated and essential component of modern industrial operations, particularly in sectors dealing with combustion byproducts. The design principles behind these systems focus on efficiency, environmental compliance, and operational reliability. By integrating advanced components and adhering to best practices, such systems ensure safe and effective ash management. For businesses looking to enhance their ash handling capabilities, companies like Shandong HeadPowder Engineering Co., Ltd. offer expert solutions that combine technology, engineering, and customer-centric service to meet the evolving needs of the industry.