Organic fertilizer powder conveying systems are essential in modern agricultural and industrial applications, designed to efficiently transport bulk organic materials. These systems play a crucial role in optimizing the handling and distribution of organic fertilizers, ensuring consistent performance and reliability in various operational settings.
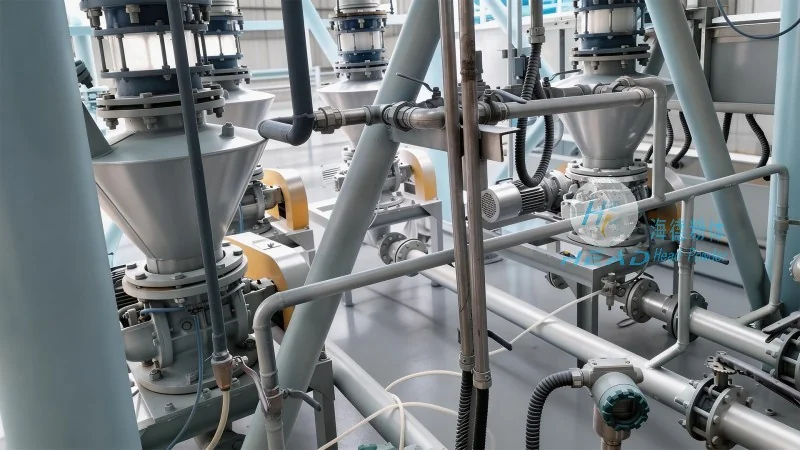
The core working principle of an organic fertilizer powder conveying system revolves around the use of specialized equipment to move bulk materials from a source to a destination. Typically, such systems integrate components like feed hoppers, conveyor mechanisms (e.g., screw conveyors, pneumatic conveyors, or bucket elevators), and control systems to manage the flow of organic fertilizer powders. The process begins with the organic fertilizer being loaded into a hopper, where it is then transferred to the conveyor system. Depending on the system design, the conveyor may use mechanical force (such as rotating screws or belts) or pneumatic pressure (air or gas) to transport the powder. The control system ensures precise regulation of the conveying speed and quantity, maintaining optimal performance and preventing material blockages or spills.
For instance, in a screw conveyor system, the organic fertilizer powder is fed into a rotating screw that moves the material forward through a tube or trough. This method is particularly effective for dry, free-flowing organic fertilizers, as it minimizes material degradation and maintains product integrity. Pneumatic conveying systems, on the other hand, utilize compressed air to create a flow of air and powder, which is then directed to the desired location. This approach is advantageous for longer distances or when dealing with more delicate organic materials that require gentle handling.
Organic fertilizer powder conveying systems from Shandong HeadPowder Engineering Co., Ltd. are engineered with several key features that enhance their efficiency and reliability. One of the primary features is the robust construction, designed to withstand the rigors of continuous operation with bulk organic materials. The systems are typically made from corrosion-resistant materials, such as stainless steel or high-quality alloys, to ensure durability and longevity. This is particularly important when handling organic fertilizers, which may contain acidic or moisture-rich components that could otherwise degrade standard equipment.
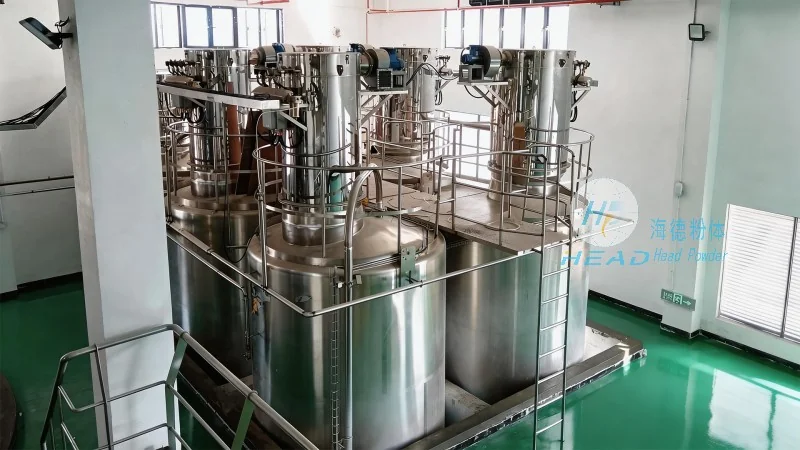
Another critical feature is the advanced control technology integrated into the system. Modern organic fertilizer powder conveying systems utilize programmable logic controllers (PLCs) and sensors to monitor and adjust the conveying process in real-time. This allows for precise control over the flow rate, pressure, and temperature, ensuring optimal performance and preventing issues like overloading or under-conveying. The control systems also include safety features, such as emergency stop buttons and overload protection, to safeguard both the equipment and personnel.
Efficiency and energy conservation are also prominent features of these systems. By optimizing the conveying process, the systems minimize energy consumption while maximizing throughput. For example, variable speed drives (VSDs) can adjust the conveyor speed based on the material load, reducing energy waste during low-demand periods. Additionally, the use of efficient pneumatic or mechanical designs reduces the overall operational costs, making the systems cost-effective for long-term use.
The organic fertilizer powder conveying systems from Shandong HeadPowder Engineering Co., Ltd. are widely used in both agricultural and industrial sectors. In agriculture, these systems facilitate the efficient distribution of organic fertilizers to farms, ensuring that crops receive the necessary nutrients for optimal growth. The systems can handle large volumes of organic materials, such as compost, manure, or organic waste, and deliver them to storage facilities or application points with minimal effort. This improves the overall productivity of farming operations and supports sustainable agricultural practices.
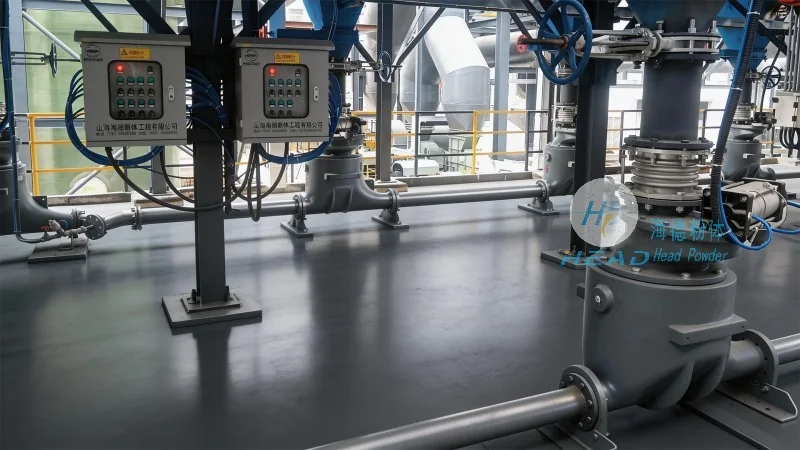
In industrial applications, the systems are used in processing facilities that produce organic fertilizers, such as biogas plants or composting operations. The efficient conveying of bulk organic materials reduces downtime and increases the overall throughput of the production process. The systems also help maintain a clean and organized workspace by preventing material spillage and dust accumulation, which is crucial for maintaining safety and compliance with environmental regulations.
Furthermore, the systems contribute to environmental sustainability by promoting the use of organic fertilizers, which are more eco-friendly alternatives to synthetic fertilizers. By enabling the efficient handling and distribution of organic materials, these systems support the transition to more sustainable agricultural and industrial practices, reducing the environmental impact of fertilizer production and use.
Organic fertilizer powder conveying systems are vital components in modern agricultural and industrial operations, offering efficient and reliable solutions for bulk material handling. The working principles and key features of these systems, as exemplified by the products from Shandong HeadPowder Engineering Co., Ltd., highlight their effectiveness in optimizing performance, enhancing safety, and promoting sustainability. With their robust construction, advanced control technology, and energy-efficient designs, these systems provide long-term value and support the growing demand for organic fertilizers in both domestic and international markets. Based in Shandong, China, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and provide high-quality conveying solutions tailored to the needs of the organic fertilizer industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan City, Shandong Province, China

telephone
WeChatconsult
top