Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a professional manufacturer specializing in the design, production, and supply of bulk material handling equipment. The company is headquartered in Shandong, China, and has been committed to providing high-quality, reliable solutions for powder and bulk material transportation in various industrial sectors. This article focuses on the working principle and key features of white gray powder conveyors, which are widely used in industries such as cement, chemical, and food processing.
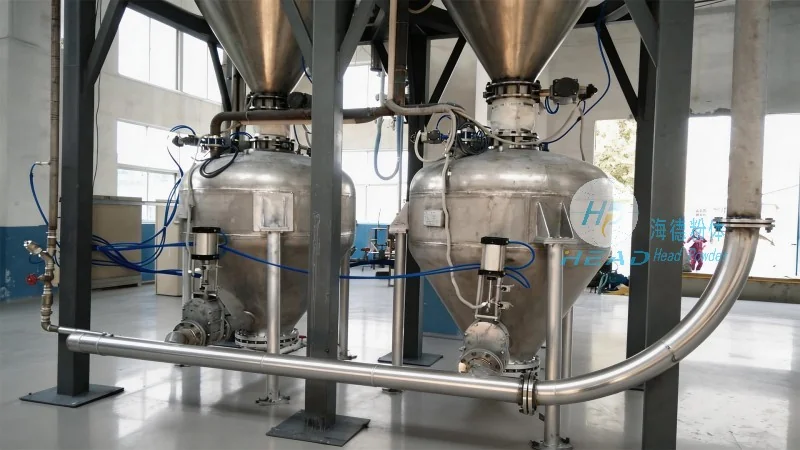
The white gray powder conveyor, also known as a bulk material conveyor, operates based on the principle of mechanical transport. The core components include a hopper for material storage, a conveyor belt or screw mechanism for material movement, and a drive system to power the operation. When the material is fed into the hopper, it is then transferred through the conveyor system to the discharge point. The conveyor's design ensures efficient and continuous movement of the powder, minimizing material loss and ensuring consistent flow rates. The drive system typically uses electric motors and gearboxes to provide the necessary torque and speed for smooth operation. The hopper is equipped with a feeding device, such as a rotary valve or a screw feeder, which controls the flow of material into the conveyor. This control mechanism allows for precise regulation of the material discharge rate, adapting to different production requirements. The conveyor's structure is designed to handle the specific properties of white gray powder, including its density, moisture content, and flowability. By optimizing the material's path and the conveyor's speed, the system ensures that the powder is transported safely and efficiently, without causing blockages or degradation of the material.
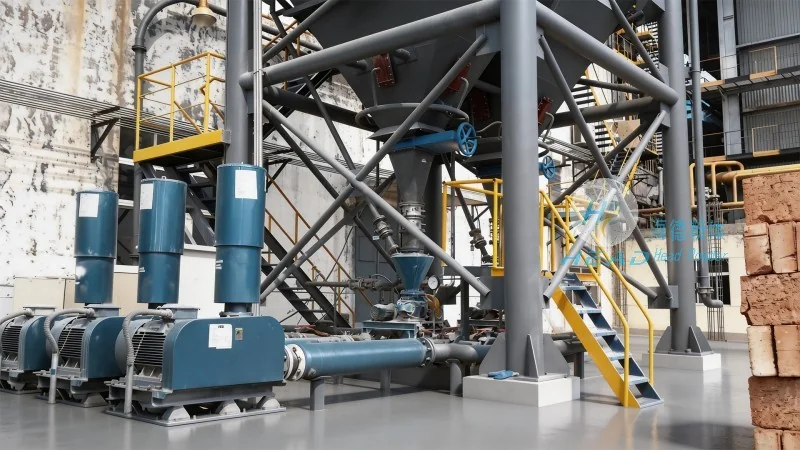
White gray powder conveyors from HeadPowder are characterized by several advanced features that enhance their performance and reliability. First, the equipment is designed with a robust construction to withstand the harsh conditions of industrial environments. The materials used for the hopper and conveyor components are corrosion-resistant and durable, ensuring long-term service life even in high-moisture or abrasive conditions. The conveyor system incorporates a closed-loop design, which helps to prevent dust leakage and maintain a clean working environment. This is particularly important for white gray powders, as they can be fine and prone to dust generation. The closed-loop design also reduces the risk of material contamination from external sources, maintaining product purity. Another key feature is the adjustable speed control, which allows operators to modify the conveyor's speed based on the material's flow characteristics and production needs. This flexibility ensures optimal performance under varying conditions, such as changes in material density or the need for increased throughput. The conveyor is equipped with a safety system that includes overload protection and emergency stop mechanisms. These features help to prevent equipment damage and ensure the safety of personnel operating the system. Additionally, the conveyor's maintenance-friendly design simplifies routine checks and repairs, reducing downtime and maintenance costs. The modular construction of the equipment enables easy replacement of worn parts, such as the conveyor belt or bearings, without the need for extensive disassembly. This design approach enhances the overall efficiency and cost-effectiveness of the system. The white gray powder conveyor also features a user-friendly control panel, which provides real-time monitoring of the system's performance. Operators can access data on material flow rate, conveyor speed, and system status, allowing for quick adjustments and troubleshooting. The control panel is designed to be intuitive, reducing the learning curve for new operators and improving overall operational efficiency. Furthermore, the conveyor's energy-efficient design minimizes power consumption, contributing to lower operational costs and reduced environmental impact. By optimizing the motor and drive system, the equipment operates at high efficiency, making it an economical choice for industrial applications.
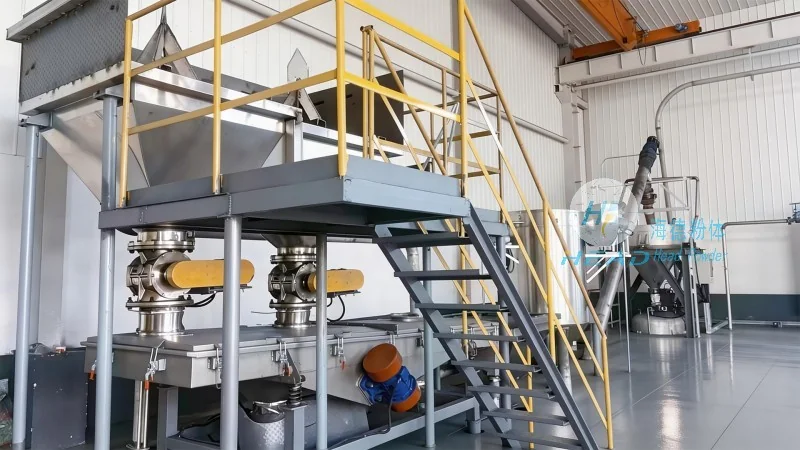
White gray powder conveyors are widely used in various industrial applications where the transportation of bulk materials is critical. In the cement industry, these conveyors are used to transport raw materials such as limestone and clay from storage silos to the production line. The consistent and reliable operation of the conveyor ensures that the raw materials are delivered in the correct proportions, which is essential for maintaining the quality of the final cement product. In the chemical industry, the conveyors are used to transport chemicals and powders, such as fertilizers and pigments, between processing units. The ability to handle different types of powders with varying properties makes the conveyor versatile and suitable for diverse chemical applications. The food processing industry also benefits from the use of white gray powder conveyors, particularly for transporting ingredients like flour, sugar, and spices. The equipment's design ensures that the materials are handled hygienically, meeting the strict standards required for food production. The benefits of using these conveyors in industrial settings include improved production efficiency, reduced labor costs, and enhanced safety. By automating the material transport process, the conveyor minimizes the need for manual handling, which reduces the risk of accidents and exposure to hazardous materials. The consistent flow of materials also helps to maintain a steady production rate, preventing bottlenecks and ensuring that production schedules are met. Additionally, the conveyor's ability to handle large volumes of material reduces the time required for material transfer, increasing overall productivity. The reliability of the equipment also contributes to lower maintenance costs, as the robust design minimizes the frequency of breakdowns and repairs. Overall, white gray powder conveyors from HeadPowder provide a cost-effective and efficient solution for bulk material transportation in various industrial sectors.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan City, Shandong Province, China

telephone
WeChatconsult
top