

Working Principle and Features of Coal Ash Material Handling Systems
Coal ash, a byproduct of coal combustion in power plants, requires efficient and reliable handling systems to ensure safe and sustainable management. The coal ash material handling system developed by Shandong HeadPowder Engineering Co., Ltd. (commonly known as HeadPowder) is designed to address these challenges, offering a comprehensive solution for transporting and managing coal ash from generation to disposal or utilization.
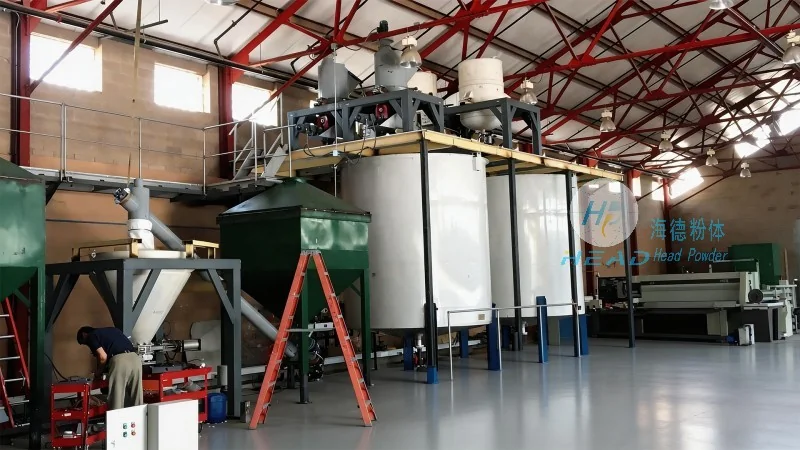
Overview of the Coal Ash Material Handling System
The coal ash material handling system is a specialized equipment setup engineered to handle the unique properties of coal ash, including its high moisture content, abrasive nature, and potential for dust generation. This system integrates multiple components that work in tandem to ensure seamless material flow, minimal downtime, and optimal operational efficiency. HeadPowder, a leading provider in the field, has leveraged years of industry experience to design a system that meets the stringent requirements of modern power plants and industrial facilities.
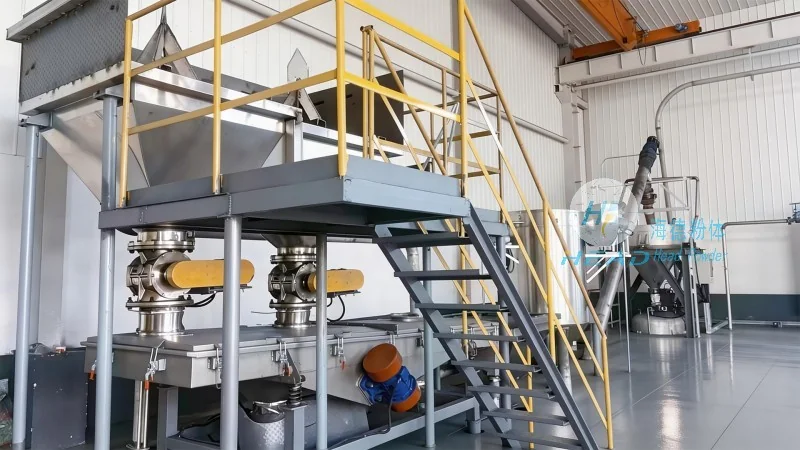
Working Principle of the Coal Ash Material Handling System
The core working principle of the coal ash material handling system involves a series of steps that transform raw coal ash into a manageable material stream. The process typically begins with the collection of ash from boilers or storage silos. A series of feeders, such as rotary or belt feeders, then convey the ash into the primary transport equipment. The system utilizes advanced conveyor technologies, including high-capacity belt conveyors or pneumatic conveying systems, to transport the ash over long distances with minimal energy consumption. The control system, equipped with sensors and automation software, monitors the flow rate, pressure, and temperature of the material, ensuring consistent performance and preventing blockages or overloads. This integrated approach allows for real-time adjustments to maintain optimal operational conditions.
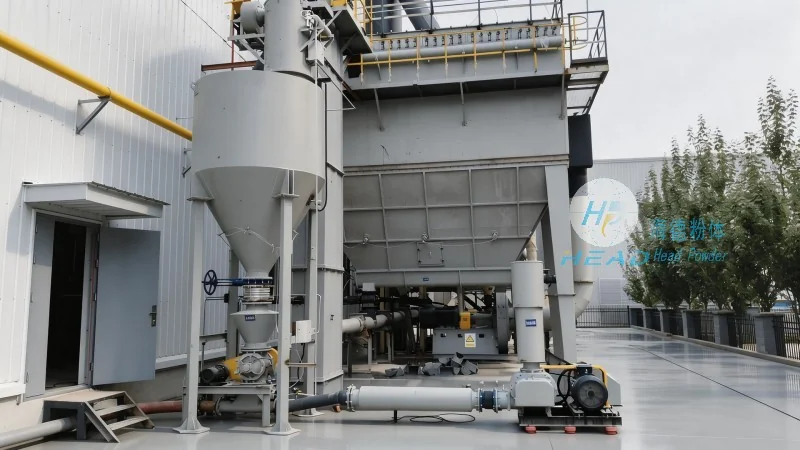
Key Features and Advantages of the System
The coal ash material handling system by HeadPowder is distinguished by several key features that enhance its performance and reliability. Firstly, the system is designed with durability in mind, using high-quality materials and robust construction to withstand the abrasive and corrosive effects of coal ash. This ensures a long service life and reduces maintenance costs over time. Secondly, the system incorporates advanced control technologies, including PLC (Programmable Logic Controller) systems and remote monitoring capabilities, which enable precise control and efficient management of the material handling process. This not only improves operational efficiency but also enhances safety by minimizing human intervention in hazardous environments. Thirdly, the system is highly adaptable, capable of handling varying ash compositions and flow rates, making it suitable for a wide range of applications from small-scale power plants to large industrial facilities. Additionally, the system is designed with environmental considerations in mind, incorporating dust suppression measures and energy-efficient components to reduce the environmental impact of ash handling operations.
Application and Benefits in Industrial Settings
The coal ash material handling system is widely used in power generation plants, cement factories, and other industrial facilities where coal ash needs to be transported and utilized as a raw material or disposed of safely. By implementing this system, facilities can achieve significant improvements in operational efficiency, reduced downtime, and lower maintenance costs. The system's ability to handle large volumes of ash with minimal energy consumption also contributes to cost savings and environmental sustainability. Furthermore, the system's reliability and durability ensure consistent performance, even under harsh operating conditions, which is crucial for maintaining the smooth operation of industrial processes. HeadPowder's expertise in engineering and manufacturing has enabled the development of a system that meets the evolving needs of the industry, providing a reliable solution for coal ash management.
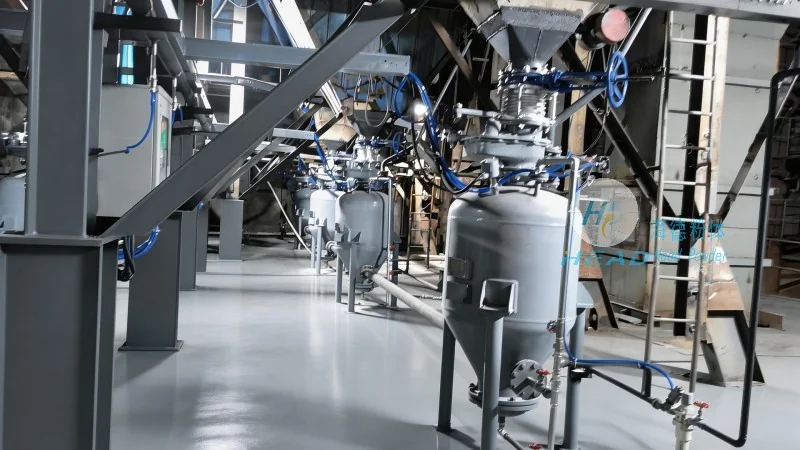
Conclusion
Shandong HeadPowder Engineering Co., Ltd. has successfully developed a coal ash material handling system that combines advanced technology with robust engineering to address the challenges of coal ash management. The system's working principle, centered on efficient material transport and intelligent control, along with its key features such as durability, adaptability, and environmental friendliness, makes it an ideal solution for modern industrial applications. By leveraging this system, power plants and industrial facilities can enhance their operational efficiency, reduce costs, and contribute to sustainable development. HeadPowder's commitment to quality and innovation ensures that the coal ash material handling system remains at the forefront of the industry, providing reliable and effective solutions for coal ash management worldwide.