

Operation Process and Working Principle of Soda Ash Powder Conveying
HeadPowder, a leading enterprise in the field of powder handling technology, specializes in providing efficient solutions for soda ash powder conveying systems. This article delves into the operational process and working principles of such systems, highlighting the technical aspects and practical applications that ensure reliable material transport in industrial settings.
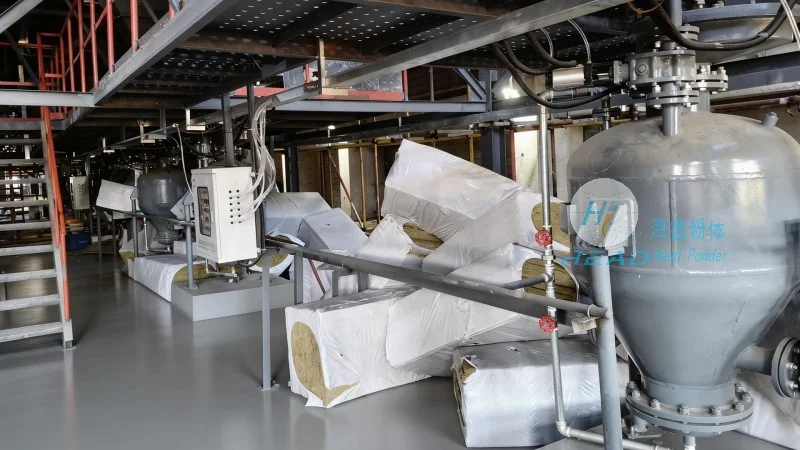
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, operating from Shandong, China, is dedicated to advancing powder handling solutions. With a strong focus on innovation and quality, the company has established itself as a trusted provider of equipment and services tailored to the needs of various industries that rely on soda ash powder transport. The company's expertise spans the design, manufacturing, and implementation of conveying systems that meet stringent operational requirements.
Understanding Soda Ash Powder Conveying Systems
Soda ash, or sodium carbonate, is a widely used chemical in industries such as glass manufacturing, chemical production, and water treatment. The efficient transport of this fine powder is critical for maintaining production efficiency and product quality. Conveying systems designed for soda ash powder must address challenges like dust generation, material flow control, and system durability to ensure smooth operation.
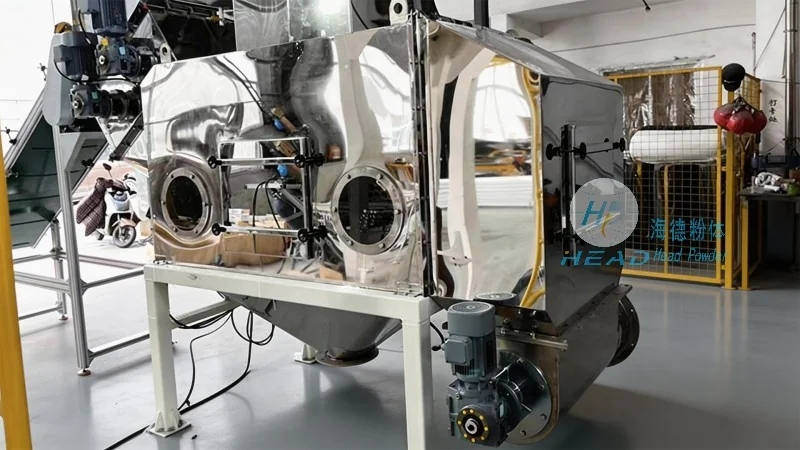
Key Components of Soda Ash Powder Conveying Systems
The operation of a soda ash powder conveying system involves several key components that work in tandem to achieve reliable material transport. These components typically include feed hoppers, conveyors (such as screw conveyors or pneumatic systems), control valves, and dust collection units. Each component plays a crucial role in the overall process, from initial material intake to final discharge.
The Operational Process of Soda Ash Powder Conveying
The operational process of a soda ash powder conveying system begins with the loading of the powder into the feed hopper. The hopper is designed to store the material and provide a controlled feed to the conveyor system. Once the material is in the hopper, it is discharged into the conveyor, which then transports the powder to the desired destination. In many systems, the conveyor is equipped with adjustable speed controls to regulate the flow rate of the powder, ensuring consistent and efficient transport.
Working Principle of Soda Ash Powder Conveying
The working principle of soda ash powder conveying systems is based on the principles of fluidization and mechanical transport. For pneumatic conveying systems, the powder is suspended in a stream of air and transported through pipelines. This method is particularly effective for long-distance transport and can handle fine powders without causing excessive wear on equipment. In mechanical conveying systems, such as screw conveyors, the powder is moved by rotating screws that push the material forward. This method is ideal for short to medium-distance transport and requires less air consumption compared to pneumatic systems.
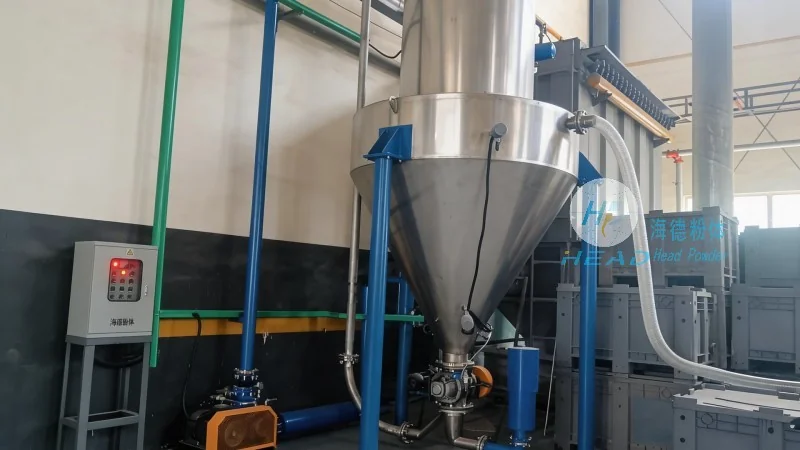
Ensuring System Efficiency and Reliability
Efficiency and reliability are paramount in soda ash powder conveying systems. Proper maintenance and regular inspections are essential to prevent issues such as blockages, material buildup, and equipment wear. The use of high-quality materials and components, along with advanced control systems, helps to minimize downtime and maximize operational performance. Additionally, the integration of dust collection systems is crucial for maintaining a safe and clean working environment, as soda ash powder can be a respiratory irritant if not handled properly.
Applications and Benefits of Soda Ash Powder Conveying
Soda ash powder conveying systems are widely used in various industrial applications, including the production of glass, chemicals, and detergents. The benefits of these systems include improved production efficiency, reduced labor costs, and enhanced product quality. By ensuring consistent and reliable transport of soda ash powder, these systems contribute to the overall success of industrial operations, helping companies to meet their production targets and maintain competitive advantages in the market.