

Operation Process and Working Principle of Stone Coal Material Conveying
Stone coal material conveying systems are critical components in industrial operations, particularly in environments where the transportation of solid waste materials like stone coal is required. These systems are designed to efficiently move stone coal from one location to another, ensuring smooth and continuous material handling processes. The operation process and working principle of such systems are essential for understanding their functionality and optimizing their performance in various industrial settings.
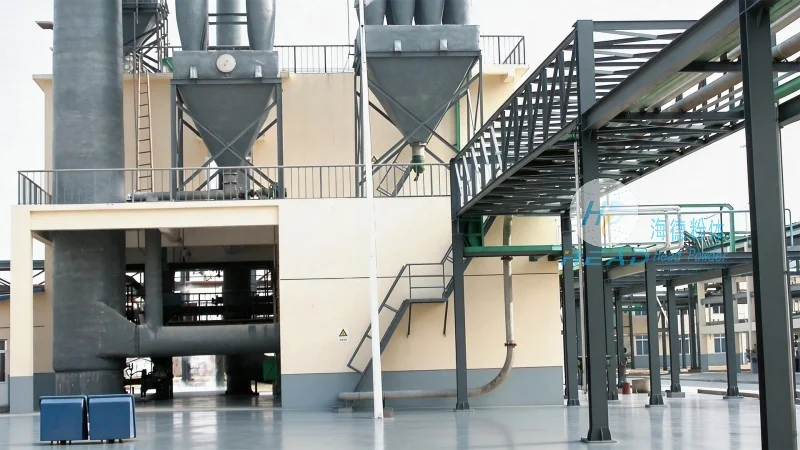
Introduction to Stone Coal Material Conveying Systems
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, production, and supply of advanced stone coal material conveying equipment. The company's products are engineered to meet the specific needs of industrial clients, providing reliable and efficient solutions for material handling challenges. This article will delve into the operation process and working principle of stone coal material conveying systems, highlighting the key components and mechanisms that enable their effective operation.
Key Components of the Stone Coal Material Conveying System
The stone coal material conveying system typically consists of several key components that work in tandem to facilitate material transport. These components include the feeding mechanism, the conveyor belt or conveyor system, the drive system, and the control unit. Each component plays a crucial role in ensuring the smooth and efficient movement of stone coal from the source to the destination. The feeding mechanism is responsible for introducing the stone coal into the system, while the conveyor belt or conveyor system provides the primary means of transporting the material. The drive system powers the conveyor, and the control unit manages the operation and monitoring of the entire system.
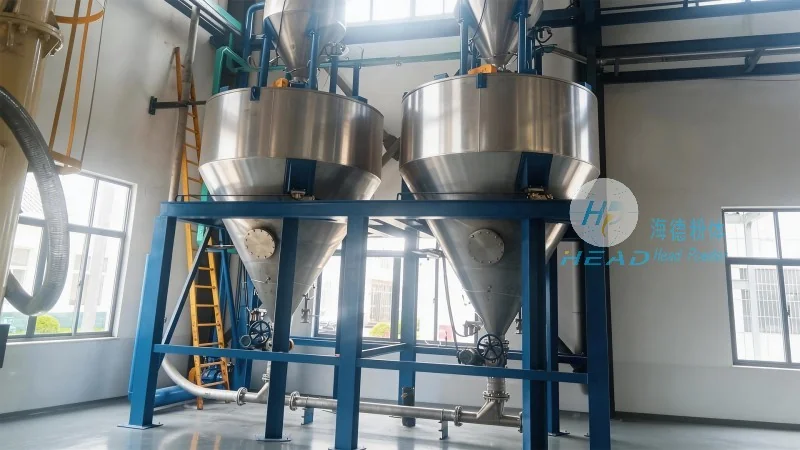
Operation Process of the Stone Coal Material Conveying System
The operation process of the stone coal material conveying system begins with the loading of stone coal into the feeding hopper or container. The feeding mechanism then transfers the stone coal onto the conveyor belt or conveyor system. As the conveyor moves, the stone coal is transported along the path defined by the system's design. The speed and direction of the conveyor can be adjusted to control the flow rate and ensure proper material handling. The system is equipped with sensors and monitoring devices that track the material level, conveyor speed, and other operational parameters, providing real-time feedback to the control unit. This allows for continuous monitoring and adjustment to maintain optimal performance. Once the stone coal reaches the end of the conveyor, it is discharged into the designated collection area or processing unit. The entire process is automated, reducing the need for manual intervention and enhancing operational efficiency.
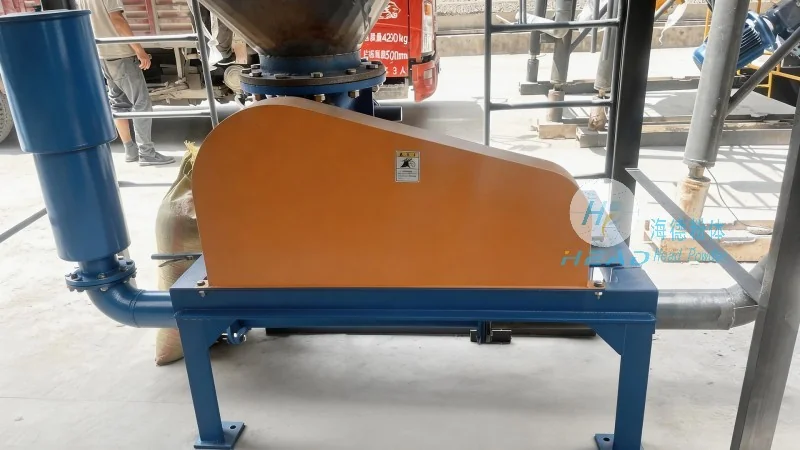
Working Principle of the Stone Coal Material Conveying System
The working principle of the stone coal material conveying system is based on mechanical and hydraulic principles that enable the movement of solid materials. The conveyor belt or conveyor system uses a continuous loop of material, such as a rubber belt or metal chain, to transport the stone coal. The drive system, which may consist of electric motors or hydraulic pumps, provides the necessary force to move the conveyor. The feeding mechanism ensures that the stone coal is evenly distributed across the conveyor surface, preventing blockages and ensuring smooth transport. The control unit manages the operation by receiving input from sensors and adjusting the conveyor speed and feeding rate accordingly. This closed-loop control system ensures that the system operates efficiently and safely, minimizing downtime and maximizing productivity. The system's design also incorporates safety features, such as emergency stop buttons and overload protection, to prevent accidents and ensure the safety of operators and equipment.
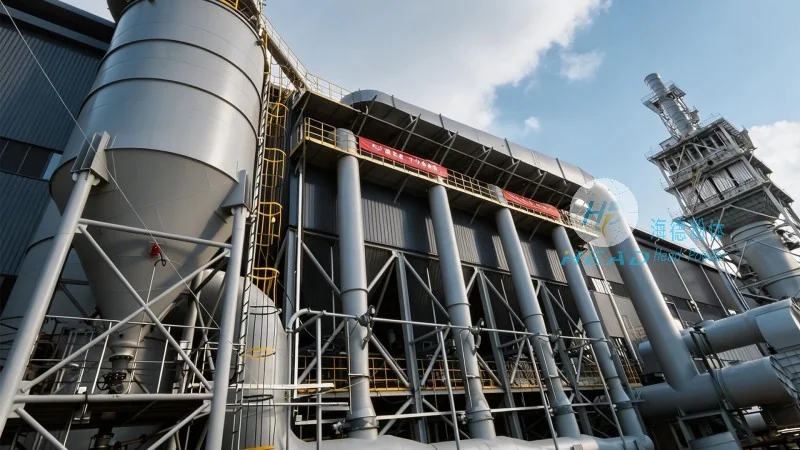
Benefits and Applications of Stone Coal Material Conveying Systems
Stone coal material conveying systems offer numerous benefits in industrial applications. They provide a reliable and efficient means of transporting solid waste materials, reducing the need for manual handling and associated labor costs. The systems are designed to handle a wide range of material sizes and types, making them suitable for various industrial settings. HeadPowder's stone coal material conveying systems are widely used in power plants, mining operations, and waste management facilities, where the transportation of stone coal is a critical part of the production process. The systems are also known for their durability and low maintenance requirements, ensuring long-term operational reliability. Additionally, the systems can be customized to meet specific client requirements, providing tailored solutions for different industrial needs.
Conclusion
In conclusion, the operation process and working principle of stone coal material conveying systems are essential for understanding their functionality and optimizing their performance. HeadPowder, with its expertise in the field, provides high-quality stone coal material conveying equipment that meets the needs of industrial clients. The systems are designed to be efficient, reliable, and safe, offering numerous benefits in material handling operations. As industrial demands continue to evolve, the importance of advanced material conveying systems like those offered by HeadPowder will only increase, ensuring continued progress in industrial operations.