

Operation Process and Working Principle of Pharmaceutical Granule Material Handling System Equipment
Pharmaceutical granule material handling systems are essential in contemporary pharmaceutical manufacturing environments. These systems are engineered to efficiently transport, store, and manage granular materials used in the production of drugs and other pharmaceutical products. The equipment from Shandong HeadPowder Engineering Co., Ltd. exemplifies advanced engineering solutions tailored to meet the stringent requirements of the pharmaceutical industry.
Key Components and Their Functions
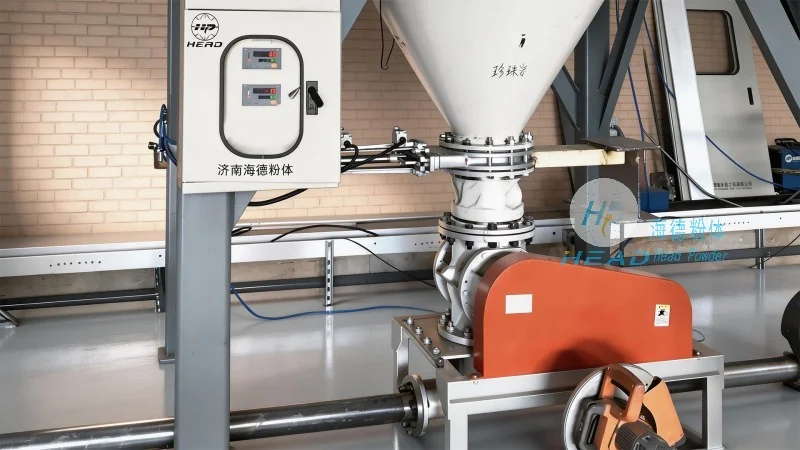
The pharmaceutical granule material handling system typically comprises several key components, each playing a vital role in the overall operation. These components include hoppers, conveyor belts, pneumatic conveying systems, and control panels. The hoppers are used to store the granule materials, ensuring a consistent supply to the processing line. Conveyor belts facilitate the movement of materials from one stage to another, while pneumatic conveying systems provide an efficient means of transporting granules over longer distances or through complex pathways. The control panels enable operators to monitor and adjust the system parameters, ensuring optimal performance and compliance with regulatory standards.
Operation Process: From Inlet to Outlet
The operation of the pharmaceutical granule material handling system begins with the loading of raw granule materials into the inlet hopper. The system then uses a combination of gravity and mechanical or pneumatic forces to move the materials through the conveyor system. The granules are transferred from the inlet hopper to the main conveyor, where they are transported to the processing or packaging area. At each stage, the system ensures that the granules are handled gently to prevent degradation or contamination. The control panel continuously monitors the flow rate, pressure, and other critical parameters, making real-time adjustments to maintain consistent performance. The system concludes with the delivery of the granules to the outlet, where they are ready for the next stage of production or packaging.
Working Principle: Mechanical and Pneumatic Integration
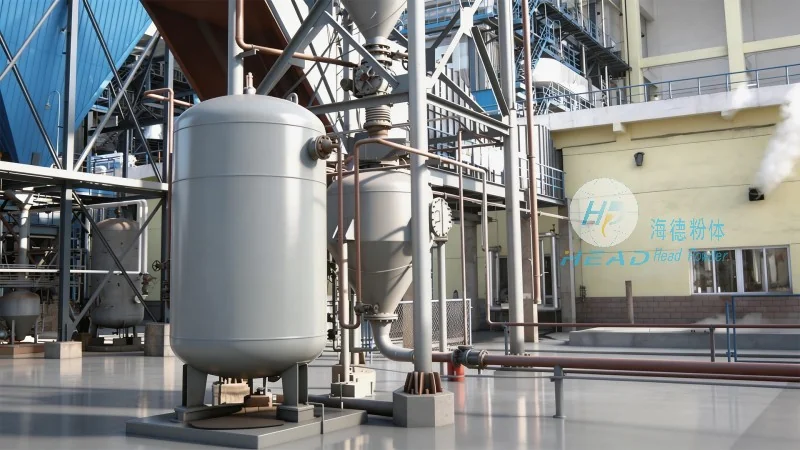
The working principle of the pharmaceutical granule material handling system integrates mechanical and pneumatic technologies to achieve efficient material transport. The mechanical components, such as conveyor belts and screw conveyors, rely on motor-driven mechanisms to move the granules through the system. These components are designed with smooth surfaces and appropriate angles to minimize friction and material degradation. The pneumatic conveying systems use compressed air to create a flow of air and granules, allowing for the transport of materials over longer distances or through vertical paths. The integration of these technologies ensures that the system can handle a wide range of granule sizes and types, from fine powders to larger granules, while maintaining high efficiency and low maintenance costs.
Advantages and Applications in Pharmaceutical Manufacturing
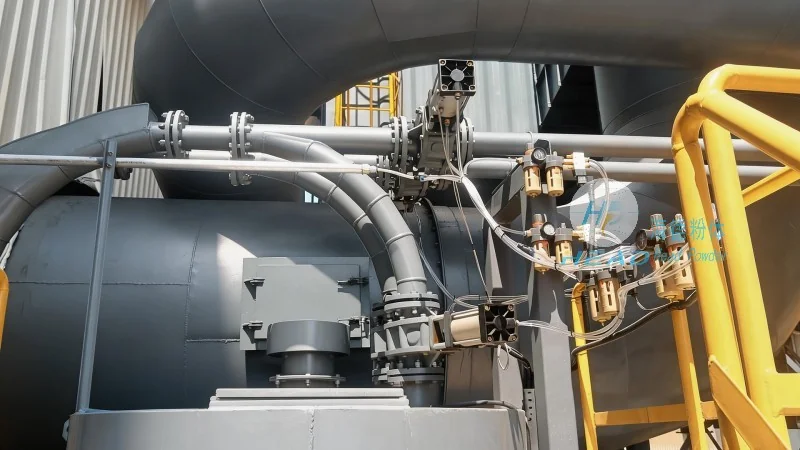
Shandong HeadPowder Engineering Co., Ltd. offers pharmaceutical granule material handling systems that offer several advantages in pharmaceutical manufacturing. These systems enhance productivity by ensuring a continuous and reliable supply of granule materials, reducing downtime and improving overall line efficiency. The gentle handling of materials minimizes product degradation, preserving the quality and efficacy of the pharmaceutical products. Additionally, the systems are designed to meet the stringent regulatory requirements of the pharmaceutical industry, including GMP (Good Manufacturing Practice) compliance. The equipment is widely used in the production of tablets, capsules, and other solid dosage forms, as well as in the handling of excipients and other raw materials used in drug manufacturing.
Conclusion: Reliable Solutions for Pharmaceutical Production
Pharmaceutical granule material handling systems from Shandong HeadPowder Engineering Co., Ltd. represent advanced engineering solutions that address the critical needs of modern pharmaceutical manufacturing. By integrating mechanical and pneumatic technologies, these systems ensure efficient, reliable, and gentle handling of granule materials, contributing to higher product quality and operational efficiency. With a focus on compliance with industry standards and customer-specific requirements, the company provides tailored solutions that meet the diverse needs of pharmaceutical manufacturers worldwide. The operation process and working principle of these systems are designed to optimize performance while maintaining the highest standards of safety and quality in pharmaceutical production.