

Analysis of Fertilizer Pneumatic Conveying Systems
Understanding the technology and applications of fertilizer pneumatic conveying systems is crucial for optimizing material handling in agricultural and industrial settings. This system efficiently transports bulk fertilizers through a network of pipes using air pressure or vacuum, offering advantages such as reduced labor costs, improved safety, and enhanced process control.
Key Components of Fertilizer Pneumatic Conveying Systems
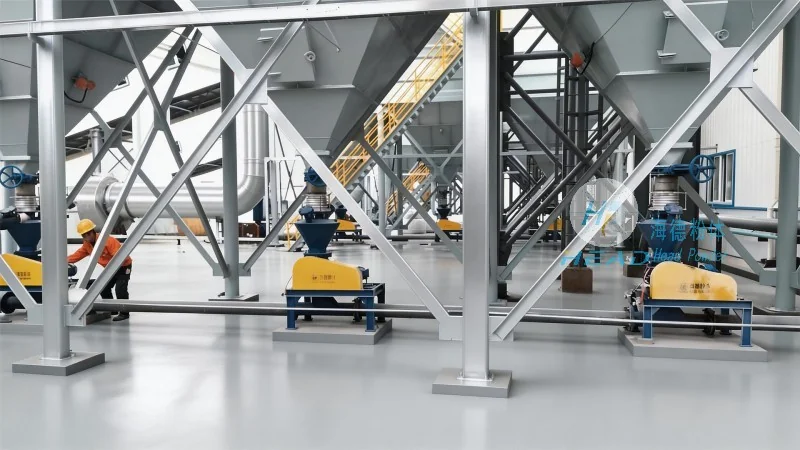
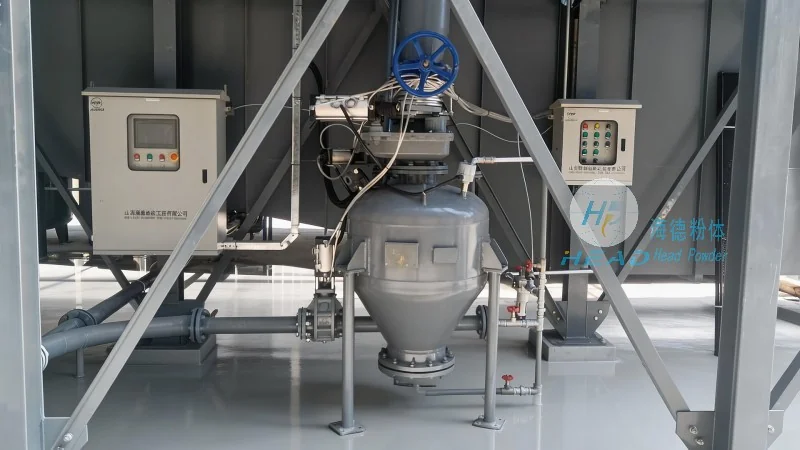
The core components of a fertilizer pneumatic conveying system include the material hopper, conveyor line, air compressor, and control valves. The material hopper stores the bulk fertilizer, ensuring a consistent feed rate. The conveyor line, typically made of stainless steel or other corrosion-resistant materials, transports the fertilizer through the system. The air compressor generates the necessary air pressure or vacuum to move the material. Control valves regulate the flow of air and material, allowing for precise control over the conveying process.
Advantages of Using Pneumatic Conveying for Fertilizers
Implementing a pneumatic conveying system for fertilizer handling offers several benefits. Firstly, it minimizes the risk of dust exposure and associated health hazards, as the material is contained within the system. Secondly, it reduces labor requirements by automating the material transport process. Thirdly, it enhances process efficiency by enabling continuous operation and precise dosing. Additionally, the system can handle various types of fertilizers, including granular, powdered, and liquid formulations, making it versatile for different agricultural applications.
Applications in Agricultural and Industrial Sectors
Fertilizer pneumatic conveying systems are widely used in both agricultural and industrial contexts. In agriculture, they are employed in fertilizer storage facilities, blending plants, and distribution centers to move bulk fertilizers from storage to application equipment. In industrial settings, they may be used in chemical manufacturing plants or fertilizer production facilities to transport raw materials or intermediate products. The system's ability to handle different fertilizer types and its adaptability to various operational conditions make it a preferred choice for both sectors.
Customization and Scalability Options
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized fertilizer pneumatic conveying systems tailored to specific client needs. The company offers scalable solutions that can accommodate varying production capacities and material types. By working closely with clients, HeadPowder engineers develop systems that optimize material flow, reduce energy consumption, and enhance overall operational efficiency. The company's expertise in material handling technology ensures that each system is built to meet the unique requirements of the agricultural or industrial application.
Installation and Maintenance Considerations
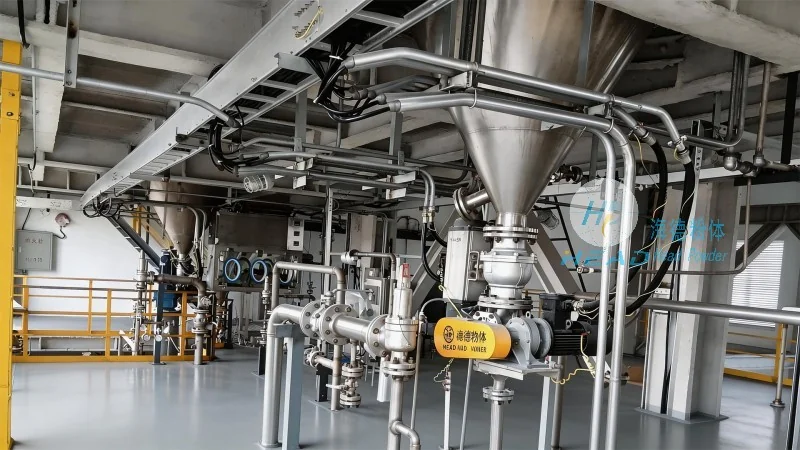
Proper installation and regular maintenance are essential for the reliable operation of fertilizer pneumatic conveying systems. During installation, the system must be carefully aligned and secured to prevent vibrations or leaks. Regular maintenance includes checking for wear and tear on components, cleaning the conveyor line to prevent clogging, and inspecting the air compressor for optimal performance. By adhering to a regular maintenance schedule, users can extend the lifespan of the system and minimize downtime. Shandong HeadPowder Engineering Co., Ltd. provides comprehensive support, including installation guidance and maintenance services, to ensure the system operates at peak efficiency.
Conclusion
Fertilizer pneumatic conveying systems represent a sophisticated and efficient solution for bulk material handling in the agricultural and industrial sectors. By leveraging air pressure or vacuum to transport fertilizers, these systems offer significant advantages over traditional methods, including improved safety, reduced labor costs, and enhanced process control. With the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., clients can implement customized systems that meet their specific operational needs, ensuring optimal performance and reliability in fertilizer handling operations.