

An Analysis of Barley Pneumatic Conveying Systems
HeadPowder, a leading engineering company headquartered in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for agricultural applications, particularly for barley processing. This article provides an in-depth analysis of the barley pneumatic conveying system, highlighting its technical features, operational benefits, and practical applications in modern grain handling operations.
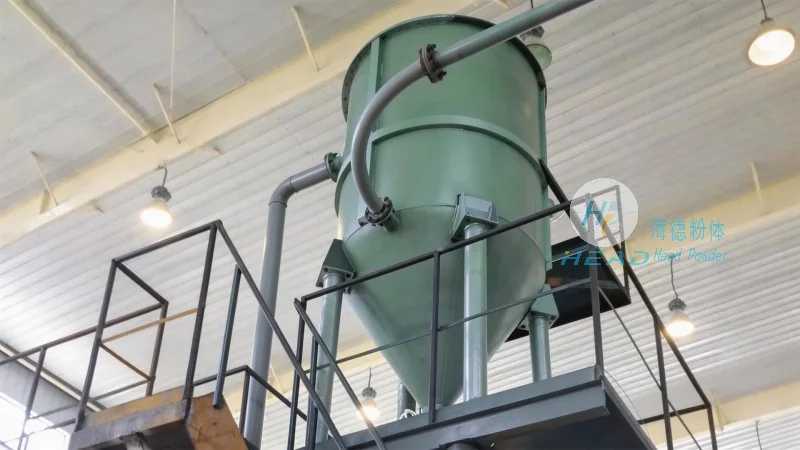
Introduction to Barley Pneumatic Conveying Systems
Barley pneumatic conveying systems represent a sophisticated method for transporting barley grains and related byproducts through a pressurized or vacuum-driven air flow. Unlike traditional mechanical conveyors, these systems utilize air as the primary medium to move materials, offering advantages such as reduced equipment wear, minimal product contamination, and enhanced safety in handling delicate agricultural products. The system is particularly suited for applications in barley processing facilities, where efficient and hygienic material transfer is critical to maintaining product quality and operational efficiency.
Key Components of the Barley Pneumatic Conveying System
The barley pneumatic conveying system consists of several core components that work in concert to ensure reliable and efficient material transport. These components include a hopper or storage silo for raw barley, a rotary airlock or feeder to control material flow, a conveying pipeline network, a pressure or vacuum source (such as a blower or vacuum pump), and a receiver or discharge unit. Each component is engineered to meet the specific demands of barley handling, ensuring that the system operates with minimal downtime and maximum throughput.
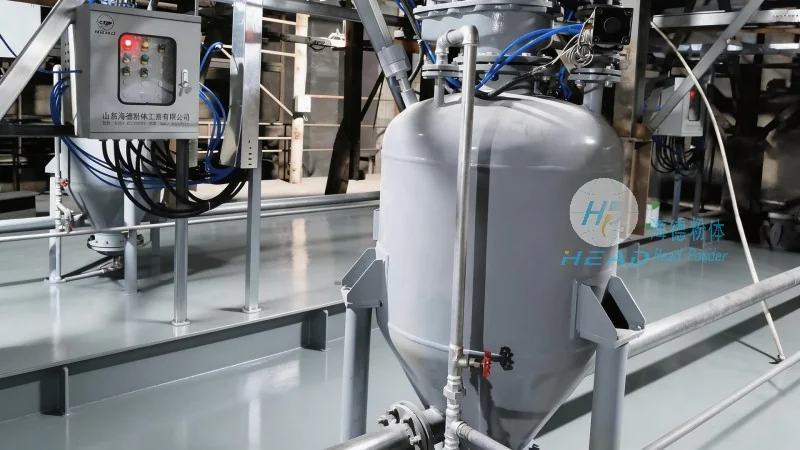
Technical Advantages of the System
One of the primary advantages of the barley pneumatic conveying system is its ability to handle a wide range of barley particle sizes and moisture content without causing damage or degradation to the product. The system’s enclosed pipeline design prevents exposure to dust, moisture, or contaminants, which is essential for maintaining the quality of barley intended for malting, brewing, or animal feed production. Additionally, the system’s energy efficiency and low maintenance requirements contribute to long-term operational cost savings for processing facilities.
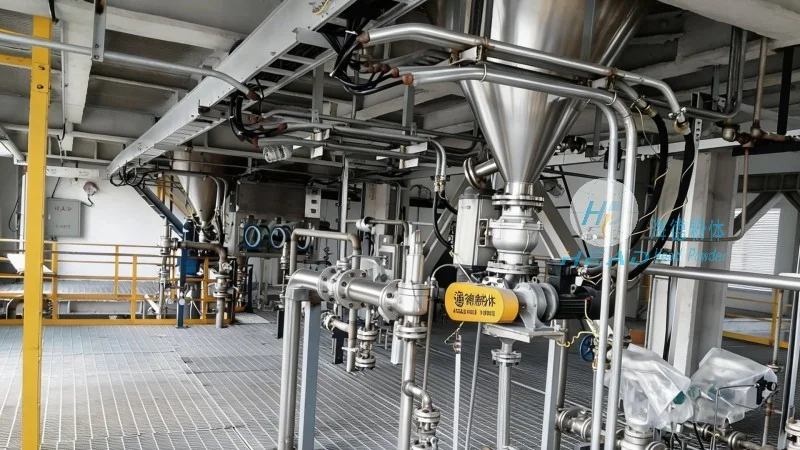
Operational Benefits and Applications
In practical terms, the barley pneumatic conveying system offers significant operational benefits to processing plants. It enables seamless integration between storage, processing, and packaging stages, reducing the need for manual handling and associated labor costs. The system is widely used in barley malting facilities to transport malted barley from storage to the mashing tanks, as well as in breweries for conveying raw barley to the mashing and boiling processes. Furthermore, its adaptability allows for flexible system configurations, accommodating varying production volumes and processing requirements.
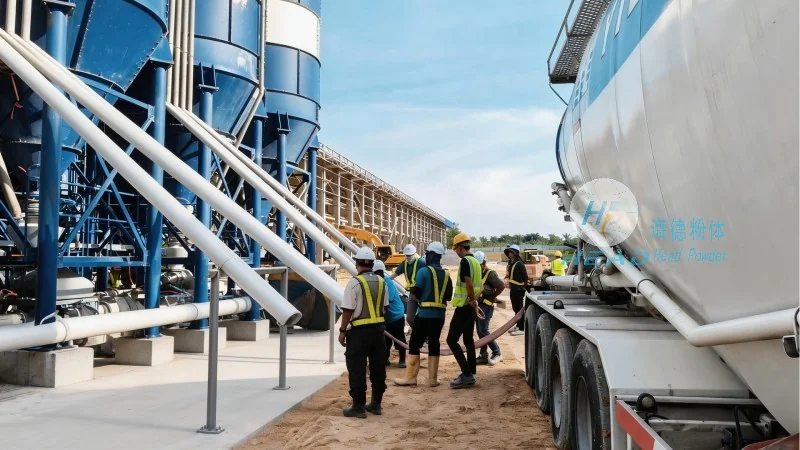
Customization and Engineering Solutions by HeadPowder
HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, provides customized pneumatic conveying solutions tailored to the unique needs of each client. The company’s engineering team works closely with clients to assess their specific barley handling requirements, including storage capacity, processing throughput, and product specifications. By leveraging advanced design software and industry expertise, HeadPowder develops tailored system configurations that optimize material flow, minimize energy consumption, and ensure compliance with industry standards for food safety and hygiene.
Conclusion
Barley pneumatic conveying systems represent a cutting-edge technology for efficient and hygienic barley handling in modern agricultural and food processing industries. With its numerous technical advantages and operational benefits, this system has become an essential component of high-performance barley processing facilities. HeadPowder Engineering Co., Ltd., based in Shandong, China, remains committed to delivering innovative and reliable pneumatic conveying solutions that meet the evolving demands of the barley processing sector, ensuring optimal performance and long-term value for its clients.