

Introduction to Purified Ash Conveying Systems and the Advantages of Purified Ash Pneumatic Conveyin
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design, manufacturing, and implementation of advanced conveying systems for industrial applications. The company's core focus is on providing efficient and reliable solutions for transporting purified ash, a critical byproduct in various industrial processes. This article introduces the purified ash conveying system, highlighting its key features and the advantages of pneumatic conveying technology in this specific application.
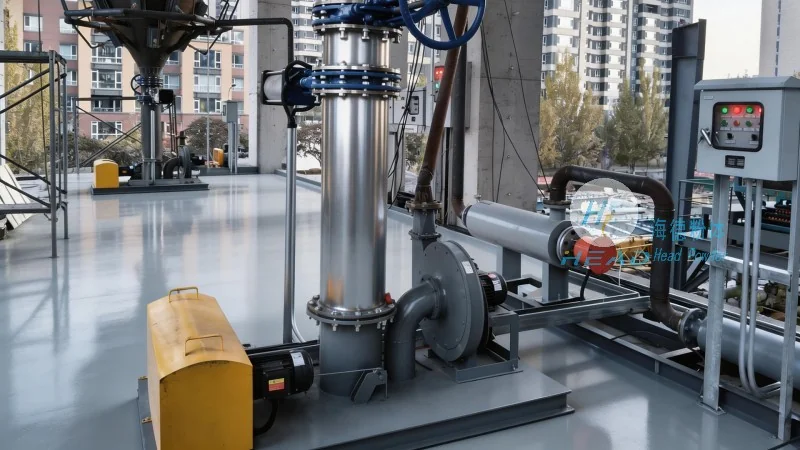
Purified Ash Conveying System Overview
The purified ash conveying system is engineered to handle the transportation of ash generated from industrial processes such as power generation, cement production, and metal smelting. These processes produce large volumes of ash that require safe, efficient, and environmentally compliant handling. The system is designed to meet stringent safety and operational standards, ensuring minimal environmental impact and optimal performance in demanding industrial environments.
Key Components of the Conveying System
The purified ash conveying system comprises several essential components that work in tandem to achieve effective material transport. These include high-capacity feed hoppers, specialized ash feeders, high-pressure air compressors, and flexible or rigid pipelines. Each component is carefully selected and integrated to ensure seamless operation and minimal downtime. The feed hoppers are designed to store and regulate the flow of ash, while the feeders ensure consistent and controlled discharge into the conveying line. The air compressors provide the necessary pressure to move the ash through the pipelines, and the pipelines are constructed from durable materials to withstand the abrasive nature of the ash and the high-pressure air.
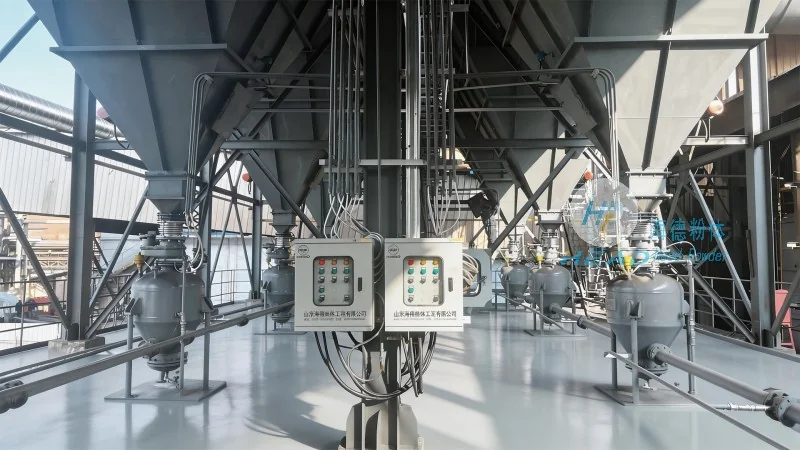
Advantages of Pneumatic Conveying for Purified Ash
Pneumatic conveying offers several distinct advantages over traditional mechanical conveying methods for purified ash. One of the primary benefits is the ability to transport ash over long distances with minimal energy consumption. The system utilizes compressed air to move the material, which reduces the need for mechanical components like conveyor belts or buckets, thereby minimizing maintenance requirements and operational costs. Additionally, pneumatic conveying provides better control over the flow rate and direction of the ash, allowing for precise delivery to storage or processing facilities. This precision is crucial for maintaining consistent product quality and reducing waste.
Enhanced Safety and Environmental Compliance
Another significant advantage of the purified ash conveying system is its enhanced safety features and environmental compliance. The system is designed to minimize dust emissions and prevent the release of harmful particles into the atmosphere. Advanced filtration and dust collection systems are integrated into the design, ensuring that the air discharged from the system meets or exceeds regulatory standards. This not only protects the environment but also safeguards the health and safety of workers in the facility. The enclosed nature of the pneumatic conveying system also reduces the risk of ash contamination and cross-contamination with other materials, maintaining the purity of the ash for downstream applications.
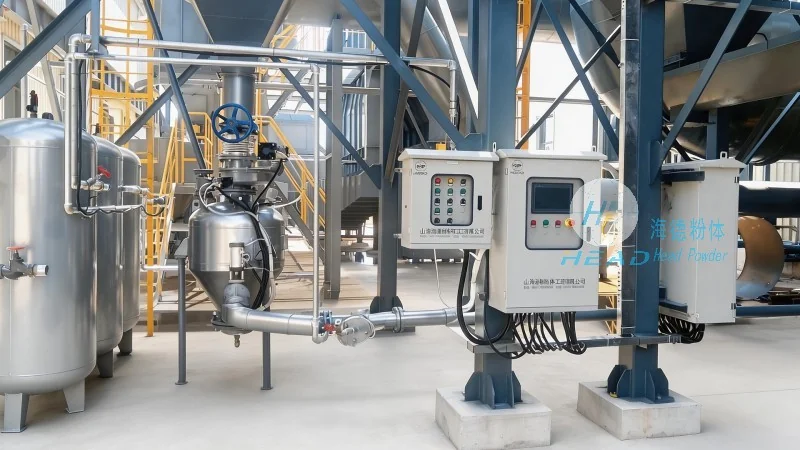
Customization and Scalability
HeadPowder understands that industrial applications vary widely, and the purified ash conveying system is designed to be highly customizable and scalable to meet diverse client needs. The system can be tailored to handle different ash compositions, particle sizes, and flow rates, making it suitable for a range of industrial settings. Whether a client requires a system for short-distance transport or a long-distance pipeline, HeadPowder can design and implement a solution that meets their specific requirements. The company's engineering expertise ensures that the system is optimized for efficiency, reliability, and cost-effectiveness, providing long-term value to its clients.
Reliability and Maintenance
Reliability is a top priority for HeadPowder's purified ash conveying systems. The components are built with high-quality materials and robust construction to withstand the harsh conditions of industrial environments. Regular maintenance is minimized through the use of durable parts and efficient design, reducing the need for frequent repairs and extending the system's operational life. The company provides comprehensive maintenance and support services to ensure that the system operates at peak performance. This includes routine inspections, component replacements, and technical support to address any issues that may arise. By prioritizing reliability, HeadPowder ensures that its clients can rely on the system to meet their production demands consistently.