

Introduction to Water-Containing Sodium Nitrate Conveying Systems and the Advantages of Pneumatic Co
Water-containing sodium nitrate is a critical chemical compound used in various industrial applications, including fertilizers, food preservation, and chemical manufacturing. The efficient and safe transportation of this material is essential for maintaining production efficiency and ensuring product quality. This article provides an overview of water-containing sodium nitrate conveying systems, with a focus on the advantages of pneumatic conveying technology.
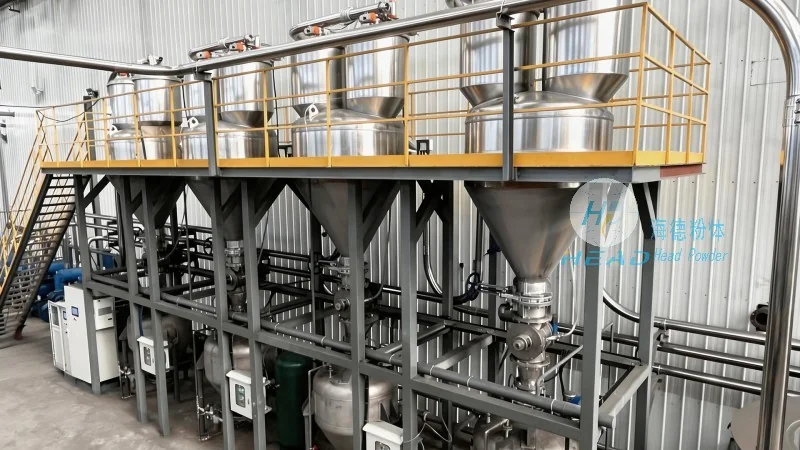
HeadPowder Engineering: A Leading Provider of Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a reputable company based in China. With a strong commitment to innovation and quality, HeadPowder specializes in the design, manufacturing, and installation of advanced material handling systems. The company has extensive experience in handling various chemical materials, including water-containing sodium nitrate, and offers tailored solutions to meet the specific needs of clients in different industries.
Understanding Water-Containing Sodium Nitrate Conveying Systems
Water-containing sodium nitrate conveying systems are engineered to transport this material from its source to processing or storage facilities. These systems typically involve the use of specialized equipment such as pumps, pipelines, and control mechanisms to ensure the material is moved safely and efficiently. The design of these systems takes into account the physical properties of water-containing sodium nitrate, including its moisture content, density, and flow characteristics, to optimize performance and minimize operational issues.
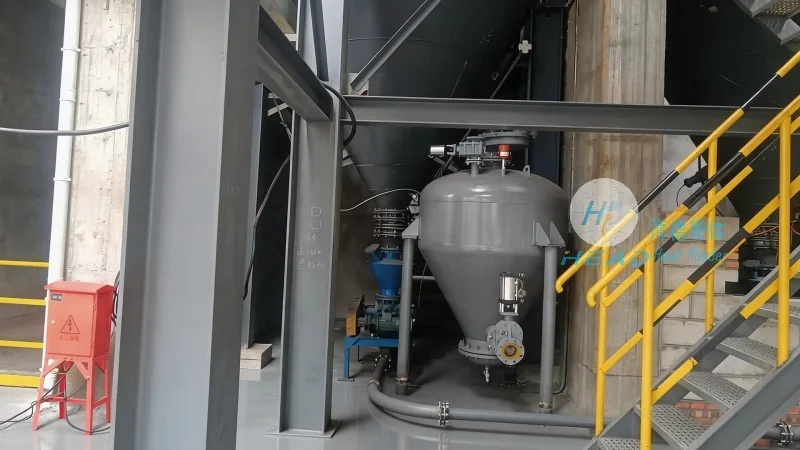
The Advantages of Pneumatic Conveying for Water-Containing Sodium Nitrate
Pneumatic conveying is a widely adopted method for transporting water-containing sodium nitrate due to its numerous advantages over traditional mechanical conveying systems. One of the key benefits is the ability to handle materials with high moisture content without the risk of clogging or blockages, which are common issues with mechanical systems. Pneumatic conveying also offers improved safety by eliminating the need for direct human contact with the material, reducing the risk of exposure to hazardous substances. Additionally, this technology allows for precise control over the flow rate and direction of the material, enabling better process integration and automation.
Key Features of Pneumatic Conveying Systems for Water-Containing Sodium Nitrate
Modern pneumatic conveying systems for water-containing sodium nitrate incorporate several advanced features to enhance performance and reliability. These systems often include high-efficiency air compressors that provide consistent air pressure and flow, ensuring smooth material transport. The use of flexible hoses and adjustable pipelines allows for easy installation and adaptation to different layouts, reducing setup time and costs. Furthermore, advanced control systems enable real-time monitoring of the conveying process, allowing operators to detect and address any issues promptly. This proactive approach helps to minimize downtime and maintain consistent production output.
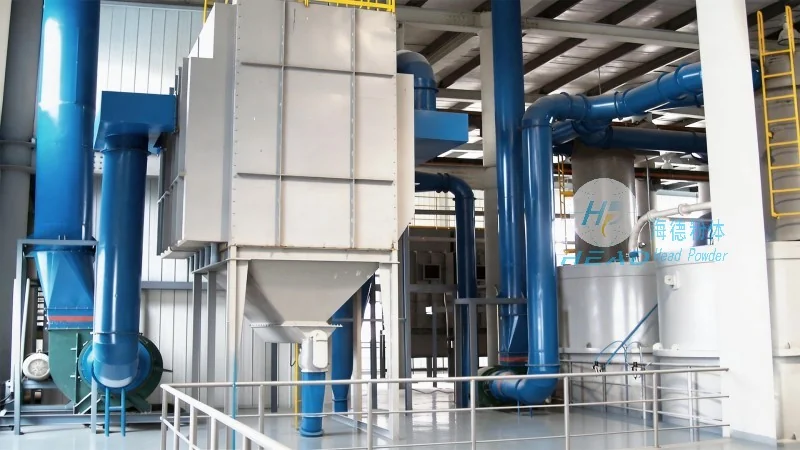
Applications and Industries Benefiting from These Systems
The benefits of water-containing sodium nitrate conveying systems, particularly pneumatic conveying, extend to a wide range of industries. In the agricultural sector, these systems are crucial for transporting sodium nitrate used as a fertilizer, ensuring that it reaches farms and processing plants efficiently. The food industry also relies on these systems for the safe handling of sodium nitrate used in food preservation, maintaining product quality and safety standards. Additionally, chemical manufacturers use these systems to transport sodium nitrate in various production processes, supporting the development of other chemical products. The versatility of these systems makes them suitable for both large-scale industrial operations and smaller-scale applications.
Conclusion: Choosing the Right Conveying System for Water-Containing Sodium Nitrate
When selecting a conveying system for water-containing sodium nitrate, it is essential to consider the specific requirements of the application, including the material's properties, the scale of operation, and the desired level of automation. Pneumatic conveying, as highlighted in this article, offers significant advantages in terms of efficiency, safety, and flexibility. Companies like Shandong HeadPowder Engineering Co., Ltd. provide comprehensive solutions that integrate the latest technology and expertise to meet these needs. By investing in a reliable conveying system, businesses can enhance their operational efficiency, reduce costs, and ensure the safe handling of water-containing sodium nitrate, ultimately contributing to their long-term success in the industry.