

Efficient and Clean Rice Grain Transport: An In-Depth Look at Pneumatic Conveying Technology
For rice processing facilities seeking to enhance the efficiency and cleanliness of their grain handling operations, pneumatic conveying technology emerges as a superior solution. This method offers a reliable, hygienic approach to transporting rice grains, addressing the unique challenges associated with handling delicate and high-value agricultural products like rice.
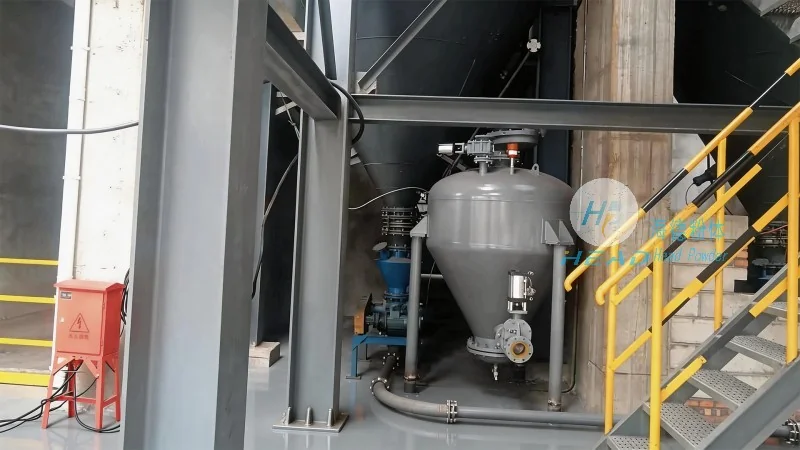
Pneumatic Conveying: A Superior Method for Rice Grain Transport
At the core of efficient rice grain handling is the ability to move bulk materials with minimal human intervention while maintaining product integrity. Pneumatic conveying systems achieve this by utilizing air pressure to transport materials through a sealed pipeline. This technology is particularly advantageous for rice, as it prevents contamination, reduces product breakage, and ensures a consistent flow rate. The system typically consists of a hopper, a conveyor line, and a receiver, all working in tandem to move rice from one location to another within a facility.
Key Advantages of Pneumatic Conveying for Rice Processing
Implementing pneumatic conveying for rice grain transport brings several key benefits that directly impact operational efficiency and product quality. First, the closed system eliminates the risk of dust and airborne contaminants entering the rice, which is crucial for maintaining food safety standards. Second, the gentle handling of the grains minimizes breakage and damage, preserving the quality and market value of the rice. Third, the system allows for precise control over flow rates, enabling operators to adjust the speed of transport based on production needs. Additionally, pneumatic conveying systems are compact and can be integrated into existing facility layouts, saving space and reducing installation costs.
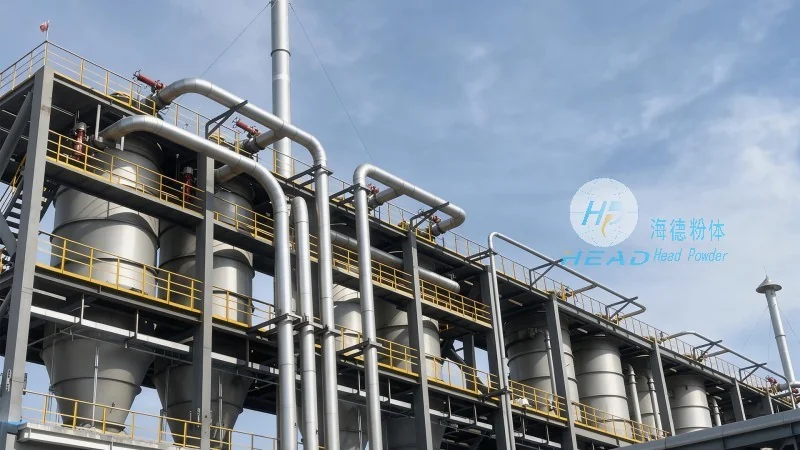
HeadPowder Engineering: Expert in Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial conveying solutions, specializes in designing and manufacturing pneumatic conveying systems tailored to the specific needs of rice processing industries. With years of experience in the field, HeadPowder understands the unique requirements of rice grain transport and offers customized solutions that optimize efficiency and maintain product integrity. The company’s expertise includes the selection of appropriate air velocities, material properties, and system configurations to ensure reliable operation in rice processing facilities.
Customized Pneumatic Conveying Systems for Rice Facilities
HeadPowder Engineering recognizes that each rice processing facility has distinct operational parameters and space constraints. Therefore, the company provides comprehensive consultation services to design pneumatic conveying systems that meet these specific requirements. This includes evaluating the type and quantity of rice being handled, the distance and elevation changes between processing stages, and the existing infrastructure of the facility. By taking these factors into account, HeadPowder engineers develop tailored solutions that maximize the efficiency of rice grain transport while minimizing downtime and maintenance needs.
Ensuring Hygiene and Compliance in Rice Handling
For rice processing facilities, maintaining hygiene and compliance with food safety regulations is paramount. Pneumatic conveying systems, when properly designed and maintained, offer a hygienic solution that meets these stringent standards. The sealed pipeline prevents the entry of external contaminants, and the system can be easily cleaned and sanitized between batches. HeadPowder Engineering ensures that all components of the pneumatic conveying system are constructed from materials that are food-grade and easy to clean, such as stainless steel. This attention to detail helps rice processing facilities adhere to regulatory requirements and maintain the trust of their customers.
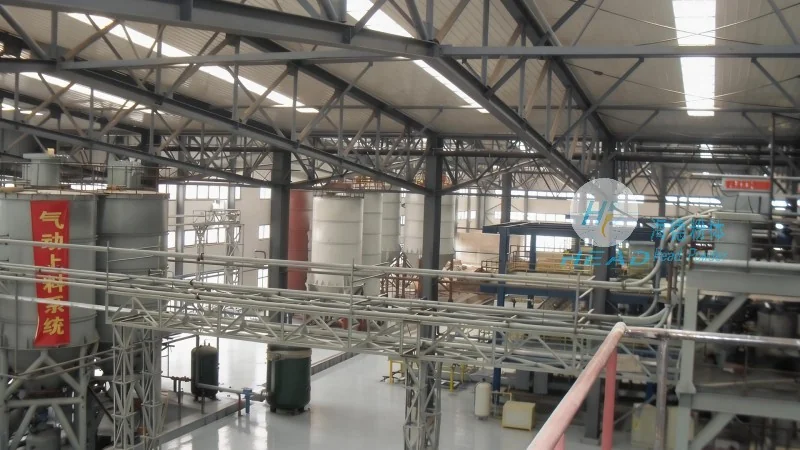
Optimizing Production Flow with Pneumatic Conveying
Efficient rice grain transport is critical to maintaining a smooth production flow in rice processing plants. Pneumatic conveying systems enable the seamless movement of rice from storage to processing, packaging, and distribution stages. By reducing the time and labor required for manual handling, these systems increase overall productivity. Additionally, the ability to control flow rates allows operators to synchronize the transport of rice with other production processes, such as milling or sorting. This synchronization minimizes bottlenecks and ensures that the entire production line operates at optimal capacity.
Long-Term Benefits of Investing in Pneumatic Conveying
While the initial investment in a pneumatic conveying system may seem significant, the long-term benefits far outweigh the costs. The reduced need for manual labor, lower maintenance requirements, and improved product quality lead to substantial cost savings over time. Furthermore, the increased efficiency of the system allows rice processing facilities to handle higher volumes of grain, expanding their production capacity. HeadPowder Engineering’s commitment to quality and reliability ensures that their pneumatic conveying systems provide a long service life, making them a worthwhile investment for any rice processing facility.